

 English
 русский
 Español
 عربى
 中文简体
 中文简体
Content
- 1 Why Ambient-Temperature Pulverizing Matters
- 2 Core Design of the 500 mm Grinding System
- 3 Intelligent Temperature Control
- 4 Particle Size Control and Screening
- 5 Technical Specifications
- 6 Processing PA Engineering Plastics
- 7 Processing PP Films and Injection Scrap
- 8 Applications in Recycling, Masterbatch, and Powder Coating
- 9 Advantages Compared with Conventional Competitors
- 10 Manufacturing Strengths and Quality Control
- 11 Energy, Noise, and Factory Integration
- 12 Maintenance and Operating Practices
- 13 How to Select the Correct Configuration
- 14 Installation and Commissioning
- 15 Quality Evaluation of Finished Powder
- 16 Q&A
- 16.1 What materials can the 500 mm grinder process?
- 16.2 Does the machine require liquid nitrogen?
- 16.3 What is the actual production capacity?
- 16.4 What particle size can be produced?
- 16.5 Can it process glass-fiber-reinforced PA?
- 16.6 How is the machine cooled?
- 16.7 Is the screen included?
- 16.8 What type of feeding system is used?
- 16.9 How often must the grinding disc be replaced?
- 16.10 Is the machine suitable for a laboratory?
- 16.11 Can the machine be used for powder coating?
- 16.12 What information should be provided for a quotation?
- 17 Conclusion
- 18 References
- 19 Product: 500PA/PP Ambient Temperature Grinder Requires No Liquid Nitrogen
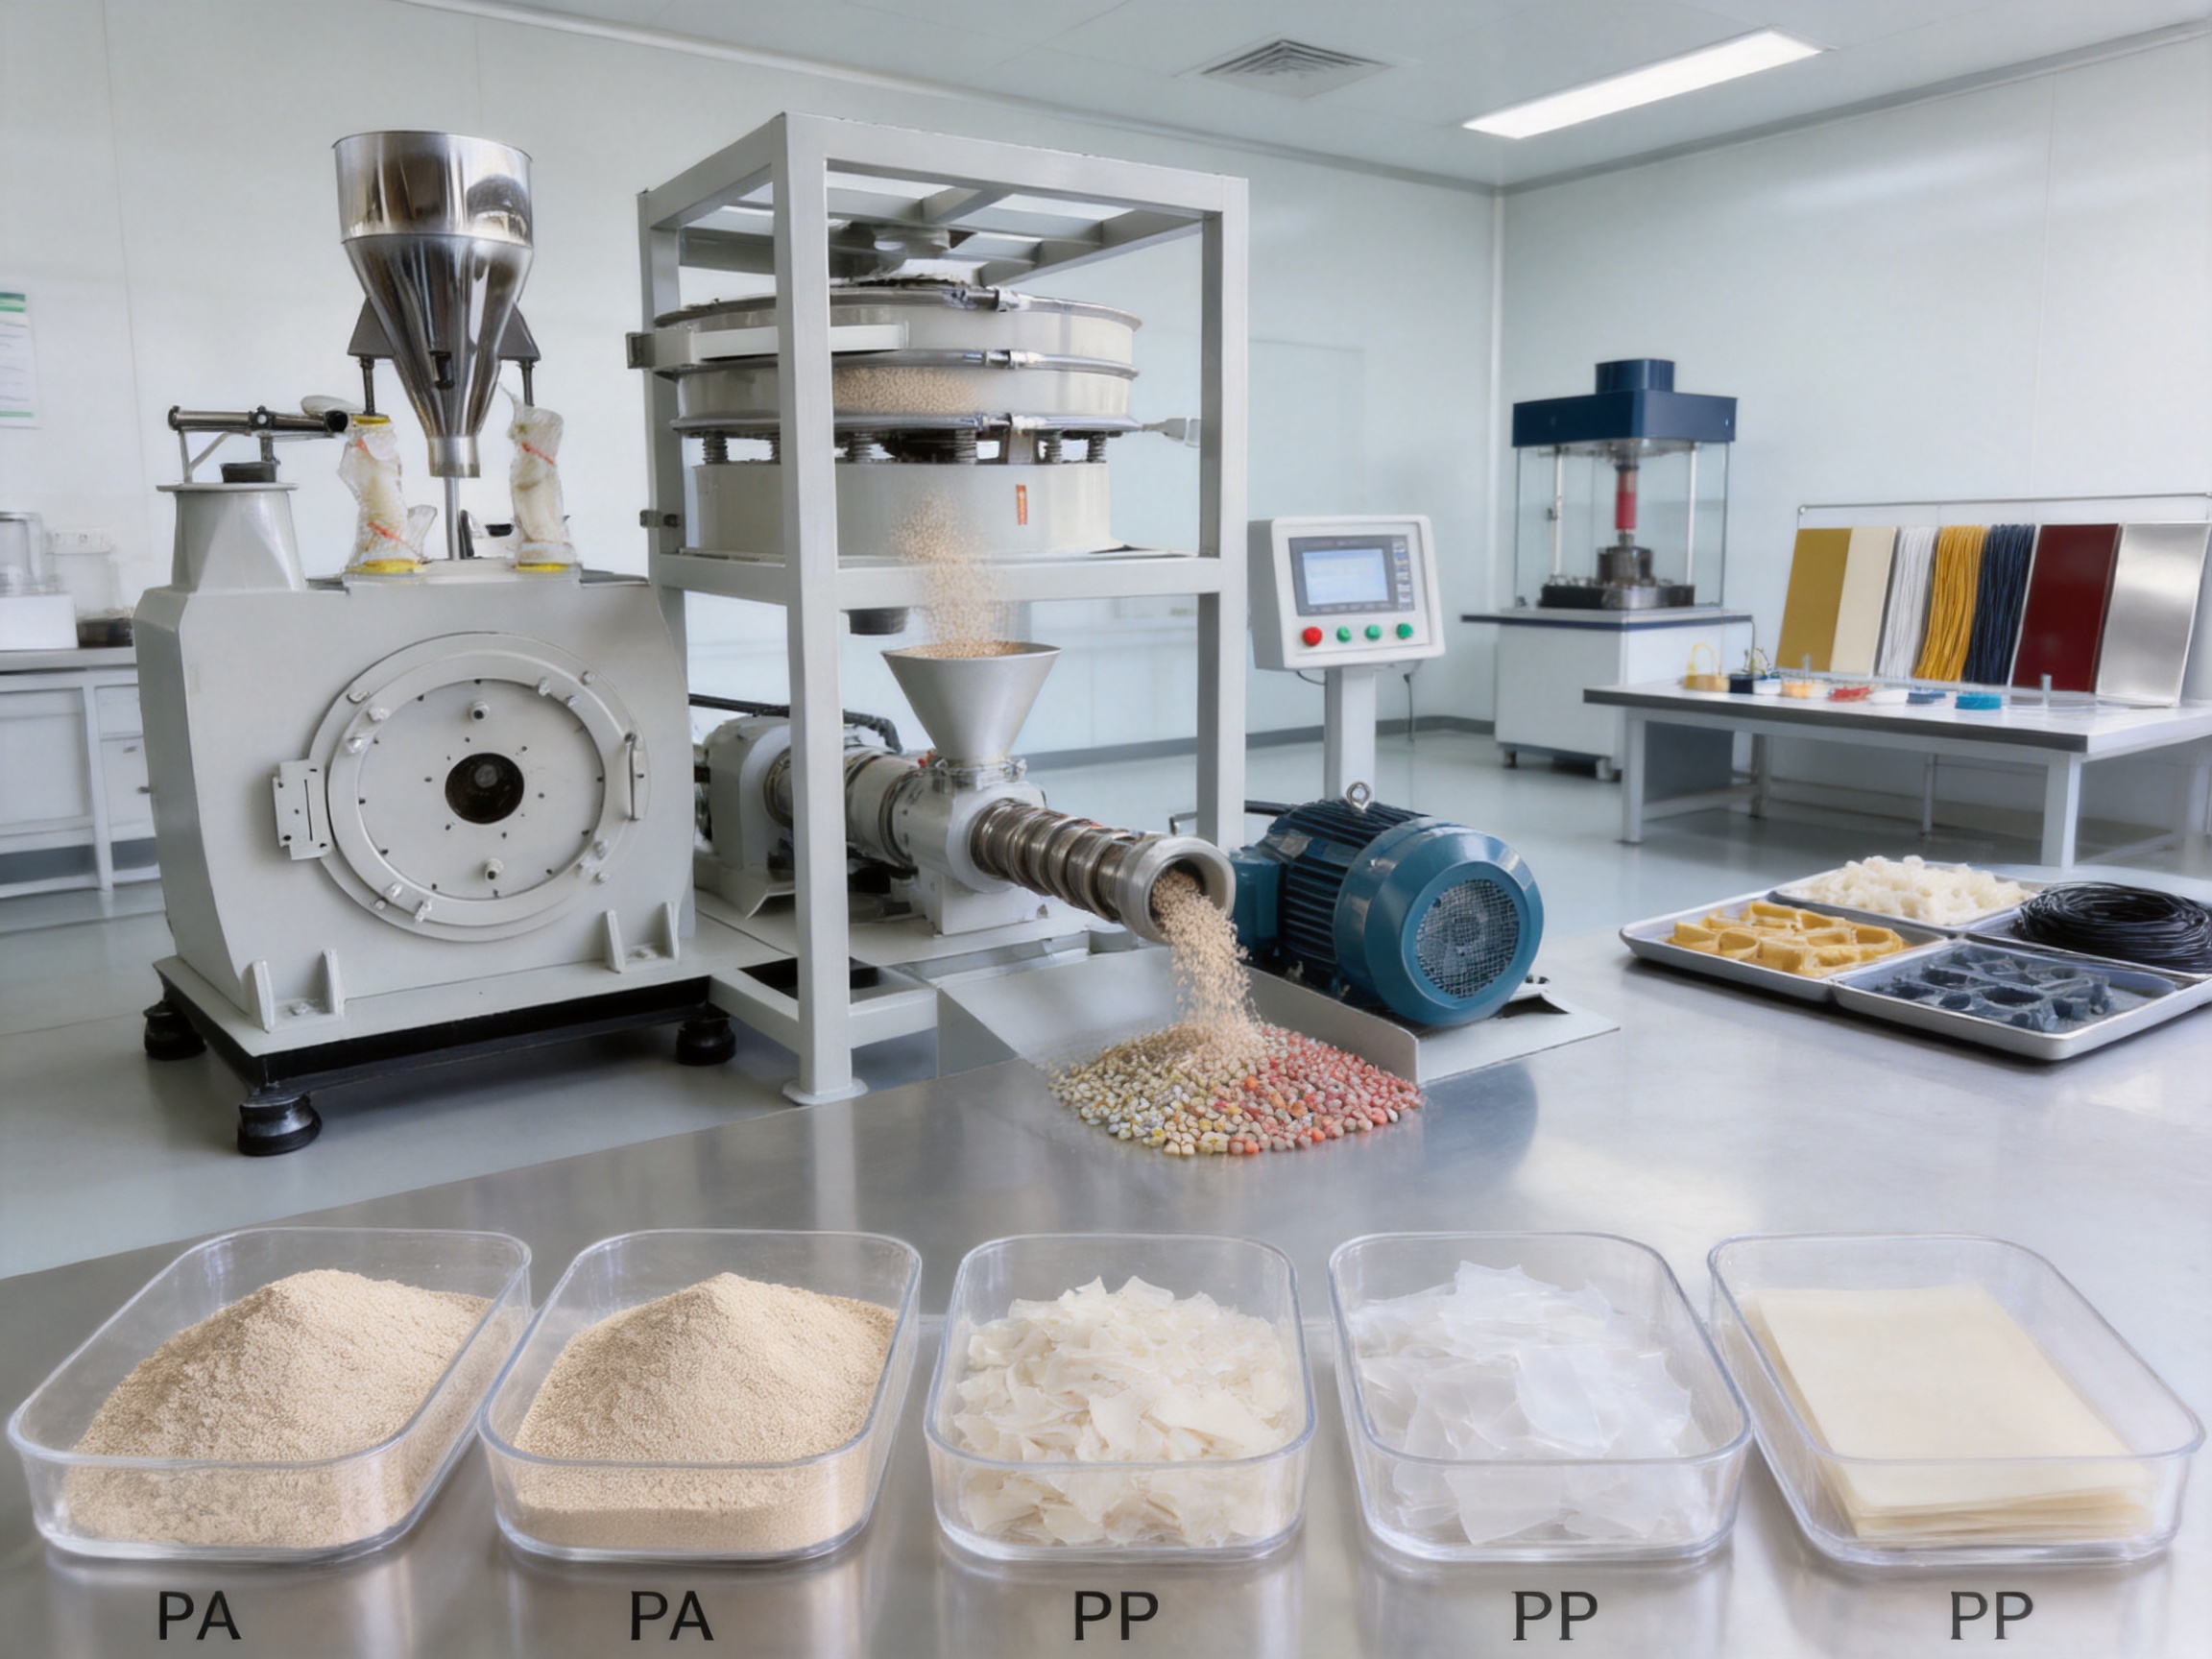
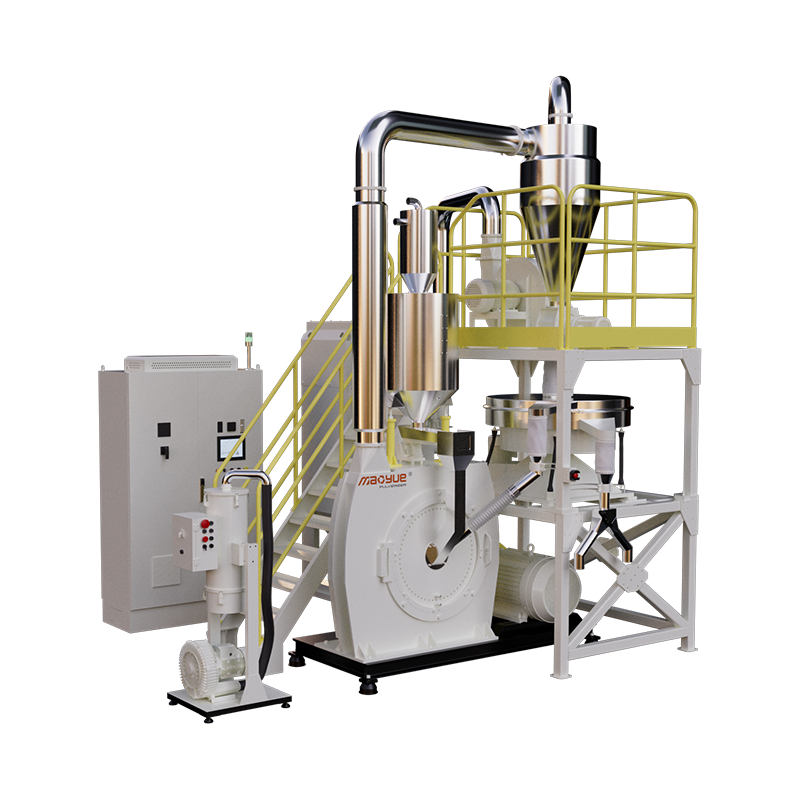
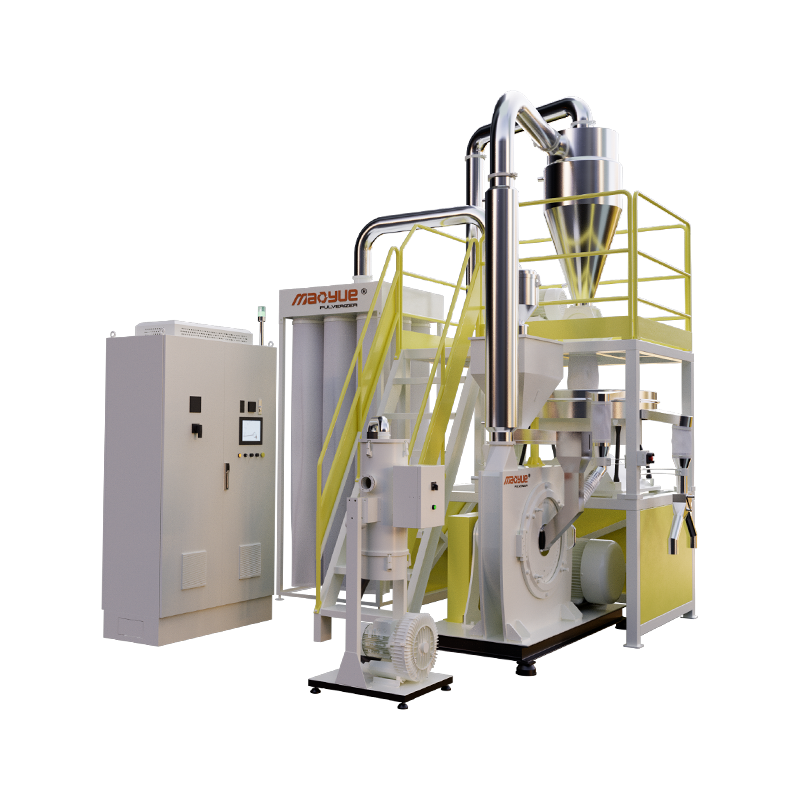
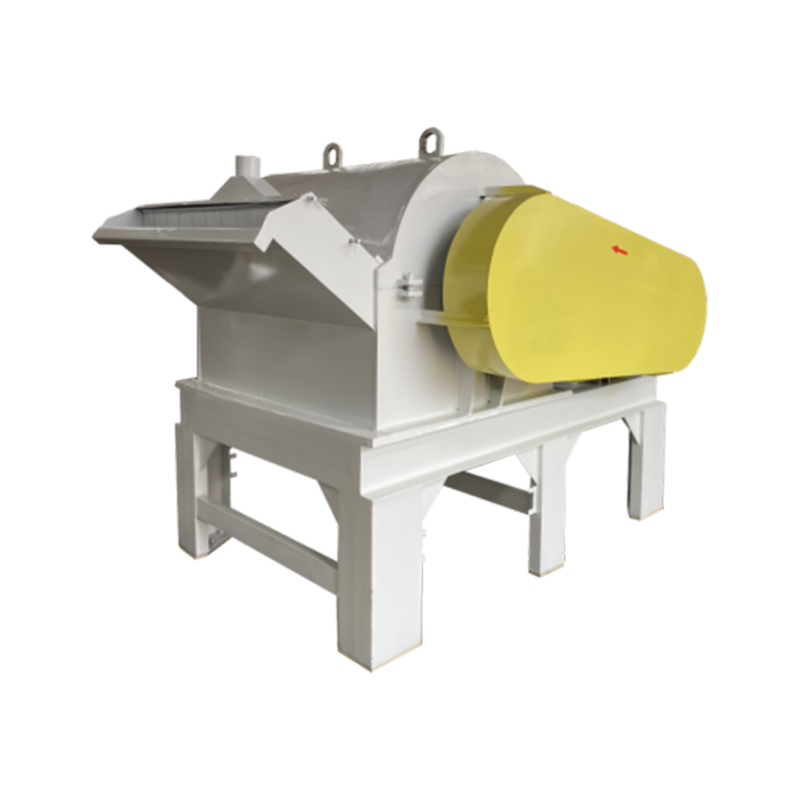
Modern plastic recycling and compounding operations increasingly require equipment that can produce consistent powder without excessive energy consumption, complicated cooling systems, or long changeover times. The 500 mm ambient-temperature grinder is designed to meet these requirements for polyamide (PA), polypropylene (PP), and related plastic materials. It combines a large-diameter grinding disc, controlled temperature management, adjustable particle size, integrated screening, and flexible feeding and discharge arrangements in a compact production system.
The machine is particularly suitable for small and medium-sized recycling plants, masterbatch producers, plastic processors, research laboratories, and businesses that handle several materials in limited or medium production batches. Its central advantage is the ability to process PA and PP under controlled ambient-temperature conditions without depending on liquid nitrogen. This reduces operating complexity and makes the equipment easier to install, operate, and maintain than cryogenic pulverizing systems.
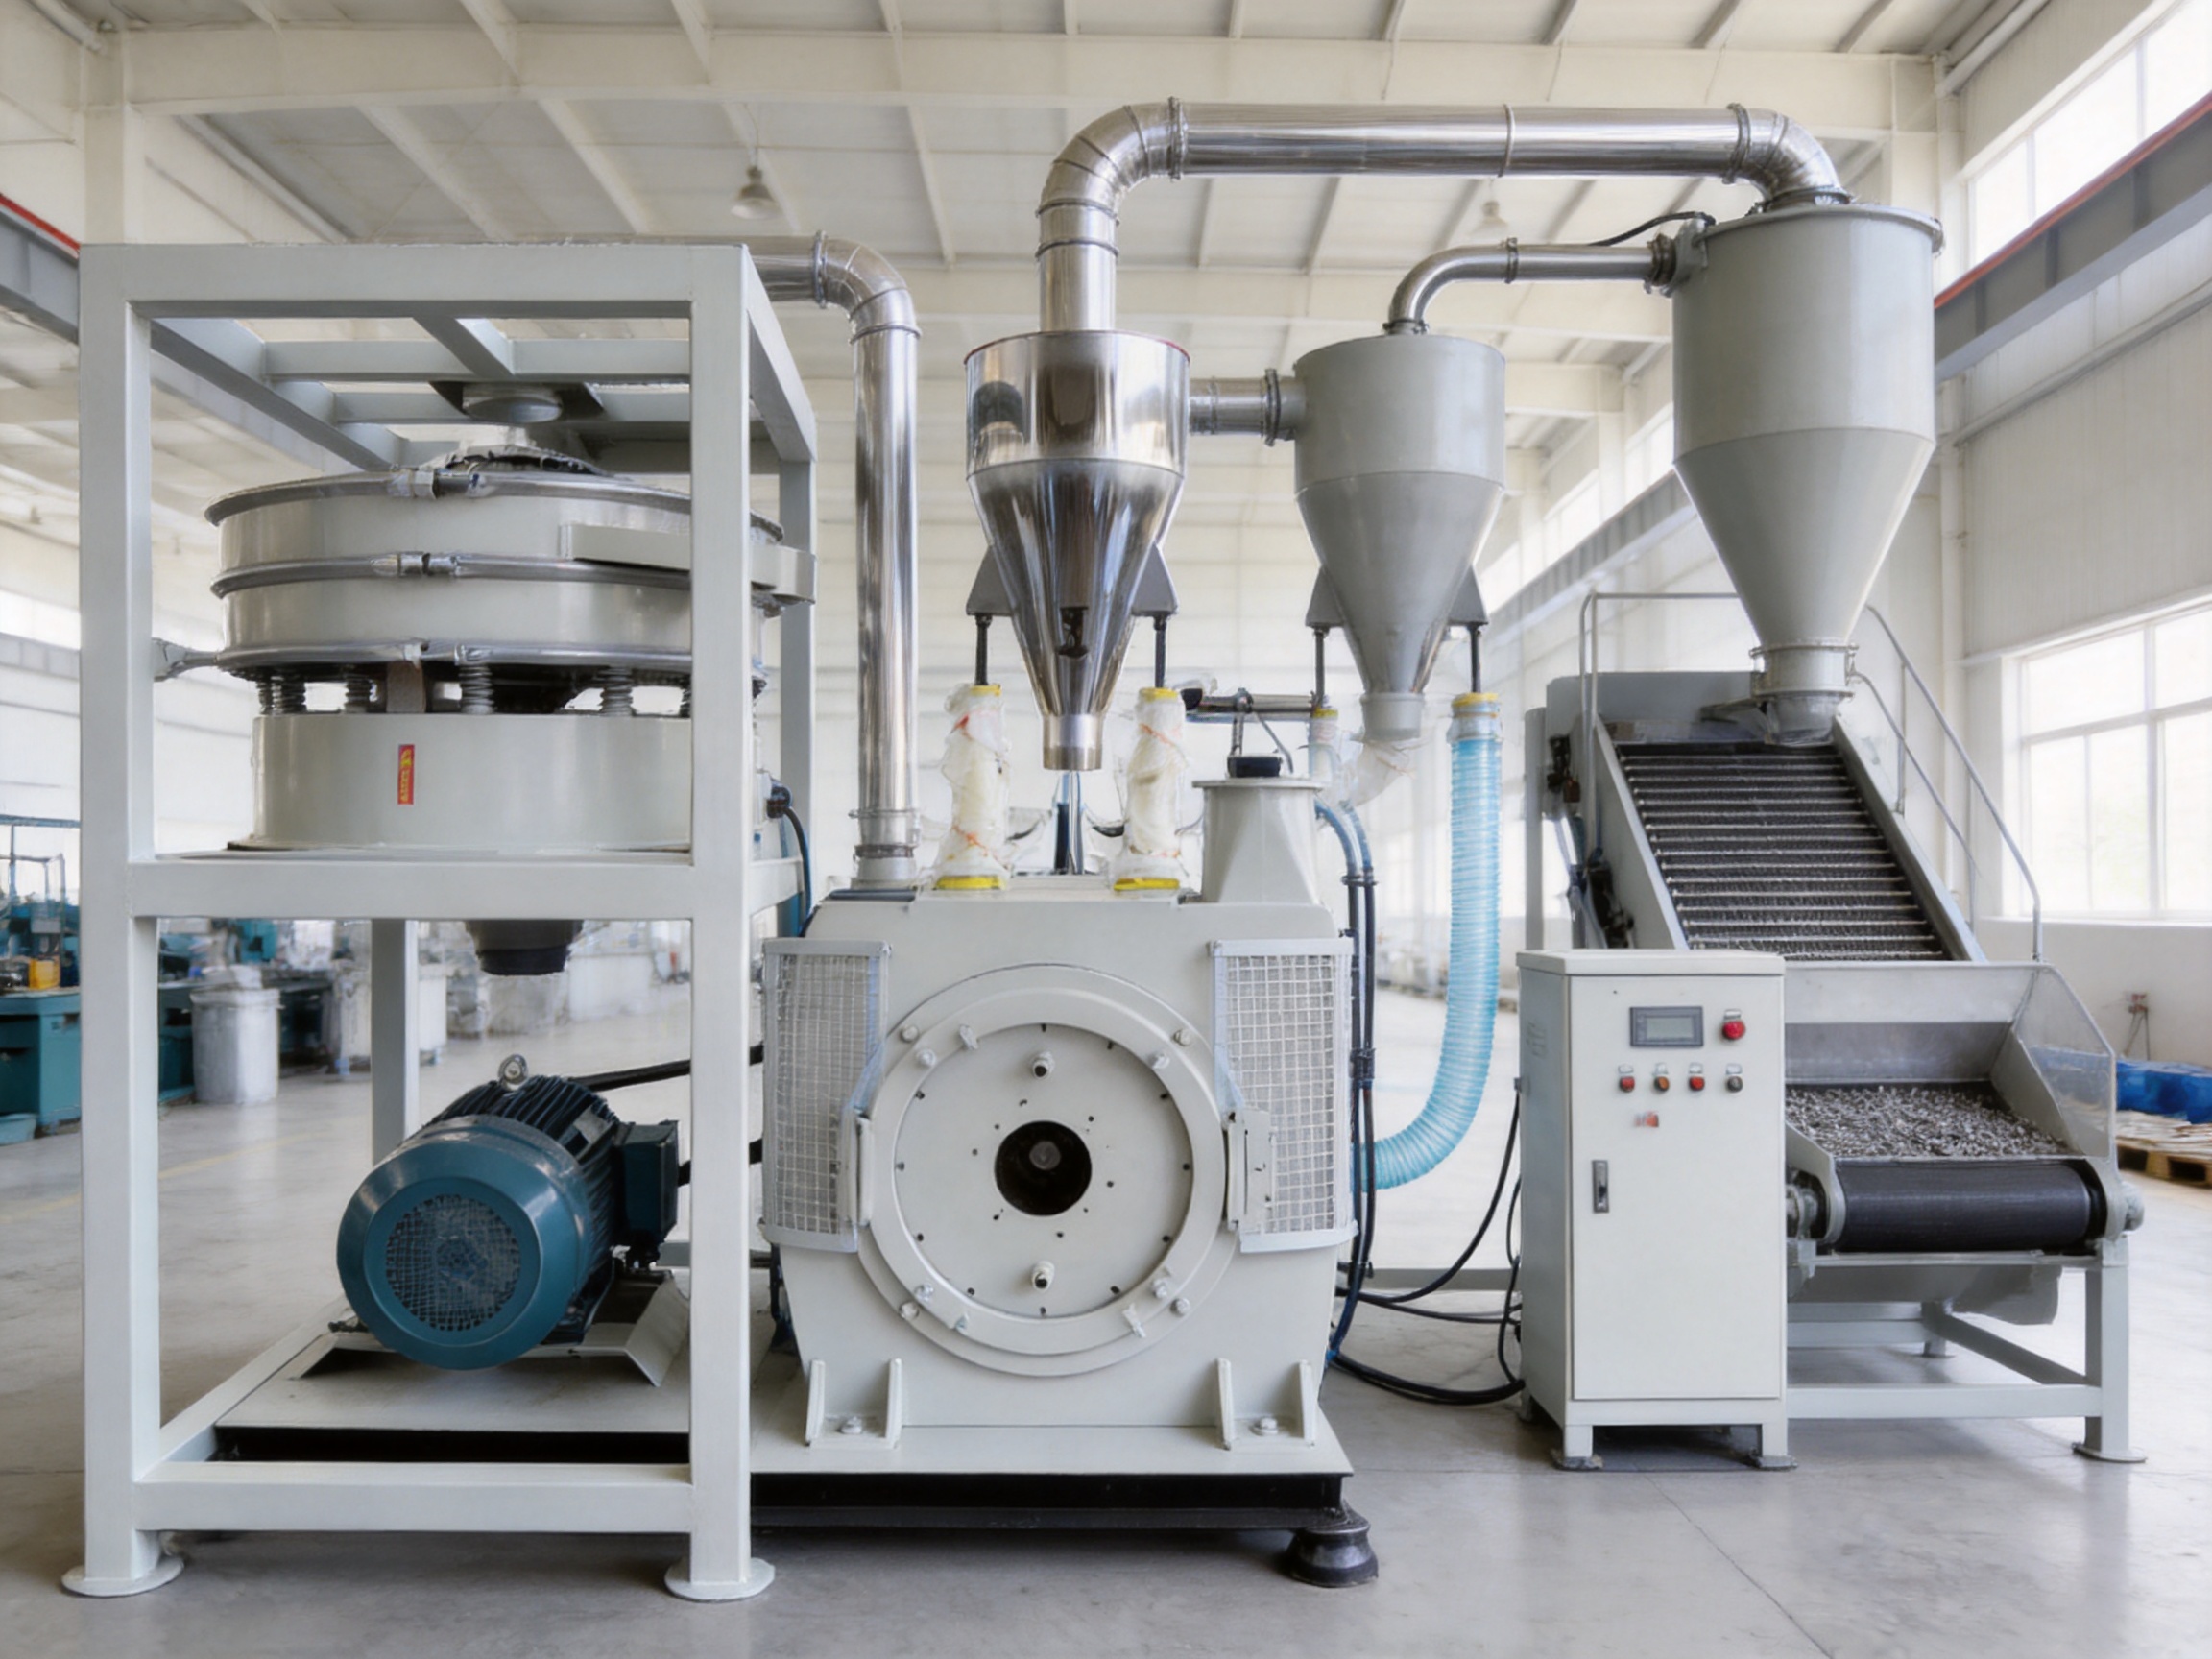
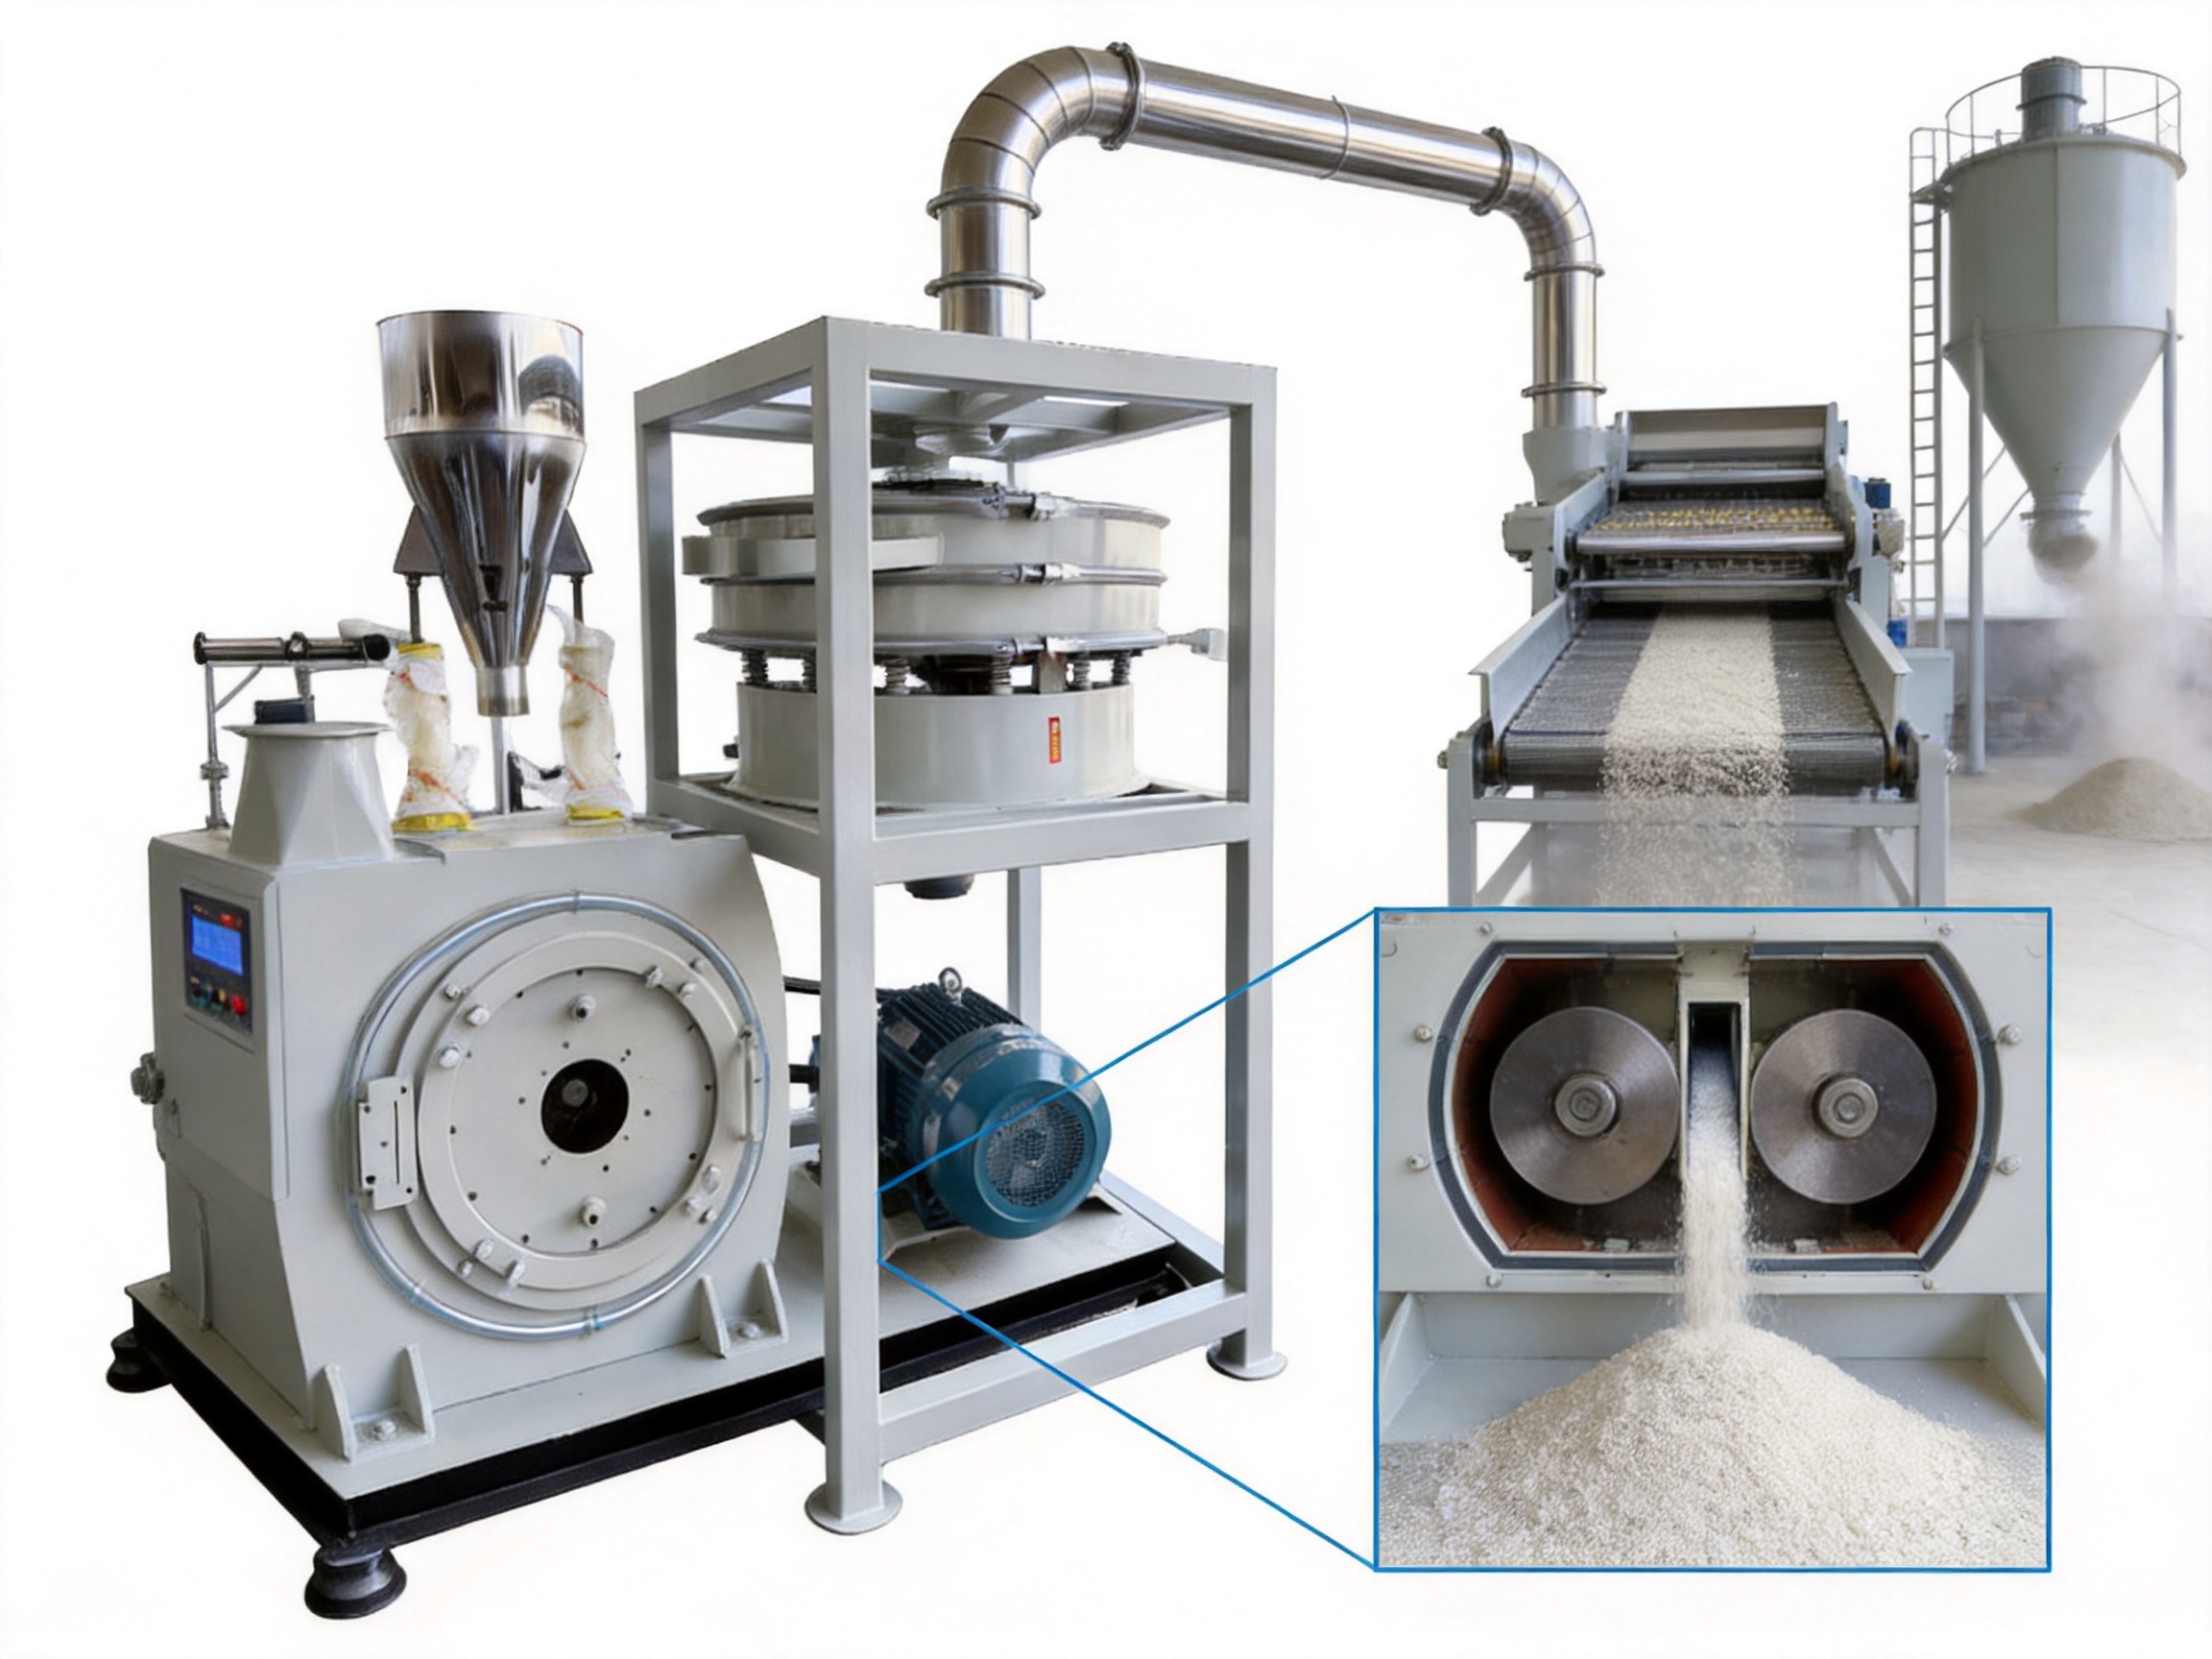
With a 500 mm grinding disc, a 37–45 kW drive motor, water cooling, vacuum feeding, stainless-steel conveying pipes, and vibrating screening, the system provides a practical balance between productivity, powder quality, and investment cost. Depending on the material, feed condition, screen configuration, and operating parameters, the machine can produce powder in different capacity and fineness ranges. The standard technical table specifies approximately 50–160 kg/h and 10–30 mesh, while optimized applications and alternative configurations can support broader working ranges, including approximately 20–100 mesh or finer laboratory-oriented settings.
Why Ambient-Temperature Pulverizing Matters
Plastic pulverizing is not simply a matter of breaking material into smaller pieces. The process must control friction, heat generation, residence time, particle circulation, and discharge efficiency. PA and PP are especially sensitive to processing conditions. Excessive heat can cause melting, agglomeration, discoloration, degradation, or unstable powder characteristics. If the grinding chamber becomes too hot, PP may soften and adhere to the grinding surfaces, while PA may experience thermal degradation or changes in its downstream processing behavior.
Traditional cryogenic systems address these challenges by cooling the material to very low temperatures, often with liquid nitrogen or another cryogenic medium. Cryogenic pulverizing can be effective for certain difficult materials, but it introduces additional equipment, storage requirements, safety procedures, operating costs, and process controls. It may also be excessive for factories that need moderate capacity, frequent material changes, or economical small-batch processing.
The ambient-temperature grinder uses controlled mechanical pulverizing and water-assisted temperature management instead of relying on liquid nitrogen. The cooling arrangement uses water circulation, with one connection serving as the inlet and another as the outlet. This approach is more accessible for ordinary industrial facilities because water-cooling infrastructure is generally easier to install and manage than cryogenic supply systems.
Ambient-temperature operation can provide several practical benefits:
1. It eliminates routine liquid nitrogen consumption for the intended PA and PP applications.
2. It reduces the need for cryogenic storage tanks, insulated lines, and specialized handling procedures.
3. It simplifies the operating environment for production staff.
4. It supports faster material changeovers when several grades or colors are processed.
5. It can lower the total cost of ownership for small and medium-sized plants.
6. It allows users to focus on controlled temperature, gap adjustment, screen selection, and feed preparation rather than cryogenic management.
The system is not intended to replace every type of cryogenic pulverizer in every application. Extremely elastic, heat-sensitive, or difficult-to-grind materials may require specialized process design. However, for many PA and PP recycling, powder production, modification, and development tasks, controlled ambient-temperature pulverizing offers a more economical and flexible route.
Core Design of the 500 mm Grinding System
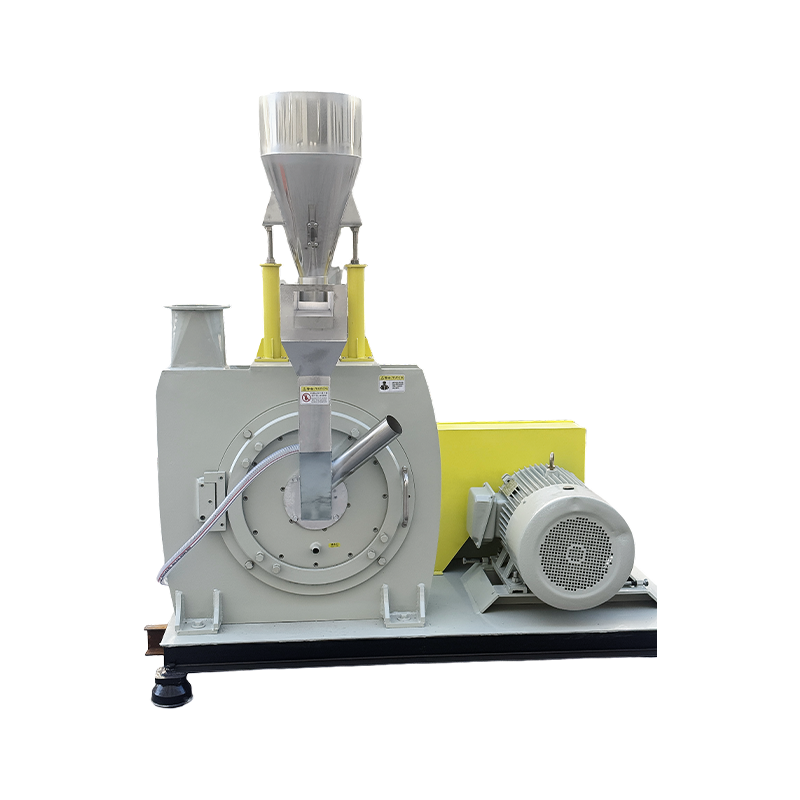
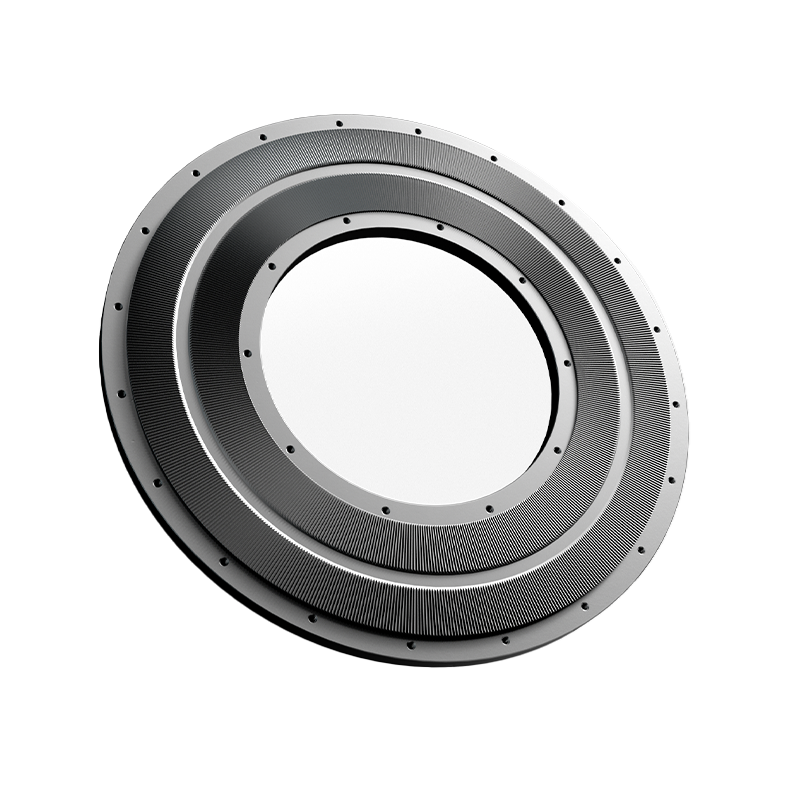
The 500 mm disc is the central working component of the machine. Its size provides a substantial grinding area while keeping the complete system compact enough for small and medium production facilities. The disc is driven by a 37 kW or 45 kW motor, depending on the selected configuration and application requirements. Users may choose different starting and speed-control arrangements, including star-delta starting, soft starting, or inverter control.
Motor selection should be matched to the material, feed size, target fineness, throughput, and production schedule. A lower-power configuration may be sufficient for standard recycling work or moderate throughput. A higher-power configuration can provide additional process capacity for more demanding materials, higher feed rates, or continuous production.
The grinding chamber is designed for adjustable operating conditions. Micron-level gap adjustment enables operators to control the distance between the grinding surfaces. This adjustment is important because different plastic materials require different grinding gaps. A narrow gap may support finer powder production, while a wider gap may reduce heat generation and improve throughput when a coarser product is acceptable.
Accurate gap adjustment also contributes to repeatability. Once a suitable setting is established for a specific PA or PP grade, operators can record and reproduce the operating condition. This helps reduce trial-and-error during subsequent production runs and supports more consistent powder quality between batches.
High-Performance Grinding Disc Material
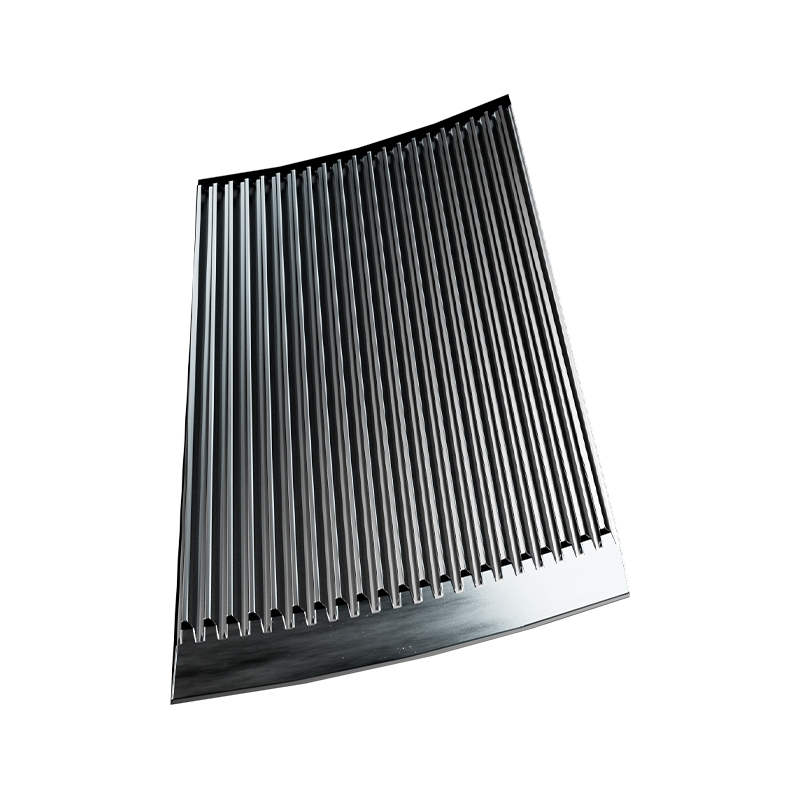
The supplied technical information identifies D2 as the standard grinding disc material. In addition, the product description refers to a proprietary high-chromium-molybdenum-vanadium alloy disc with a hardness of approximately HRC60–65. This hardened wear-resistant construction is intended to provide stronger resistance to edge wear than ordinary grinding discs.
Wear resistance is particularly important when processing glass-fiber-reinforced PA, mineral-filled compounds, and contaminated post-industrial feedstock. Reinforcing fibers and inorganic fillers can accelerate edge wear, gradually changing the grinding profile and increasing the need for maintenance. A harder and more wear-resistant disc can preserve the working geometry for a longer operating period.
According to the supplied product information, wear can be reduced by more than 60 percent when processing glass-fiber-reinforced PA compared with standard disc materials, and disc service life may be approximately twice that of conventional alternatives. Under suitable operating conditions, the stated continuous operating life is approximately 600–800 hours. Actual service life depends on feed cleanliness, filler content, moisture, operating gap, material hardness, and maintenance practices.
A wear-resistant disc does more than reduce replacement frequency. It can also help maintain stable powder characteristics. As a disc wears, the grinding gap and cutting profile may change, causing variations in particle size, throughput, and energy demand. Improved wear resistance helps the machine maintain consistent performance for a longer period and can reduce unplanned production interruptions.
Intelligent Temperature Control
Temperature control is one of the most important features for ambient-temperature PA and PP pulverizing. The machine is equipped with an intelligent temperature control system designed to maintain the grinding chamber within an operating variation of approximately ±3–5°C under suitable production conditions. This level of control helps prevent the chamber from becoming excessively hot during continuous operation.
For PA, stable temperature management helps reduce the risk of thermal degradation. Recycled PA may already have experienced heat history during molding, extrusion, or previous recycling cycles. Additional uncontrolled heat during pulverizing can affect material performance and may contribute to changes in color, flow behavior, or downstream processing stability.
For PP, temperature management helps prevent softening and melt adhesion. When PP becomes too warm inside a conventional grinding chamber, particles may stick to the disc or chamber walls rather than leaving the system as free-flowing powder. This can reduce output, increase cleaning requirements, and create inconsistent particle size. Controlled cooling helps preserve a more stable dry-powder process.
The temperature control system also supports production efficiency. When the grinding chamber operates within a controlled range, operators can establish more reliable relationships between motor load, feed rate, gap setting, and powder fineness. This reduces the need for constant manual intervention and makes the equipment more suitable for repeated production of different materials.
The stated product information indicates that controlled temperature management can help achieve melt-index fluctuation of less than 0.4 g/10 min in appropriate applications and can improve the qualified yield rate by approximately 25 percent. These results depend on the incoming material, moisture level, contamination, processing history, test method, and downstream quality criteria. They should therefore be verified through application trials before commercial production.
Particle Size Control and Screening
Powder fineness is a major factor in the value of recycled PA and PP. Powder that is too coarse may disperse poorly in masterbatch production, coating applications, or subsequent compounding. Powder that is too fine may require more energy, produce excess dust, or create handling problems. The 500 mm system is designed to provide adjustable particle size according to the selected gap, screen, feed rate, material condition, and operating speed.
The product description states a general fineness range of approximately 20–100 mesh, with 30–80 mesh identified as a common operating range. The technical table specifies 10–30 mesh for the standard configuration, and the application information indicates that laboratory-oriented processing may be adjusted to approximately 20–120 mesh. These figures reflect different operating configurations and application targets rather than a single guaranteed output for every material.
Before purchasing, customers should define the desired particle size in terms of a recognized test method and distribution requirement. Mesh size is a useful general reference, but it does not fully describe the distribution of particles. A customer requiring a narrow particle-size distribution should evaluate D10, D50, and D90 values, oversize percentage, fines percentage, and flow properties through a material test.
The integrated vibrating screen helps separate particles after grinding. The vibrating motion promotes continuous classification and helps prevent oversized particles from entering the finished product stream. It also supports a more uniform powder output than a system that relies only on the grinding chamber without secondary screening.
Uniform particles, high sphericity, and good flowability are valuable in many downstream operations. They can improve feeding consistency, dispersion, mixing, coating coverage, and the repeatability of injection molding or extrusion compounds. For powder coating applications, consistent fineness helps support more uniform electrostatic charging and film formation.
Advantages of Integrated Screening
An integrated screen provides several practical advantages over separate manual screening:
1. It reduces the need to transfer material between independent machines.
2. It reduces powder loss during handling.
3. It provides a continuous classification step.
4. It helps remove oversize particles before packaging or downstream processing.
5. It reduces operator labor and manual inspection requirements.
6. It supports a more compact plant layout.
7. It simplifies the connection between grinding, classification, dust collection, and bagging.
The standard vibrating screen has a diameter of approximately 1,000 mm and uses a 1.1 kW motor. The appropriate screen specification should be selected according to the target particle size and material behavior. PA and PP may respond differently to vibration, static electricity, moisture, and fines generation, so application testing remains important.
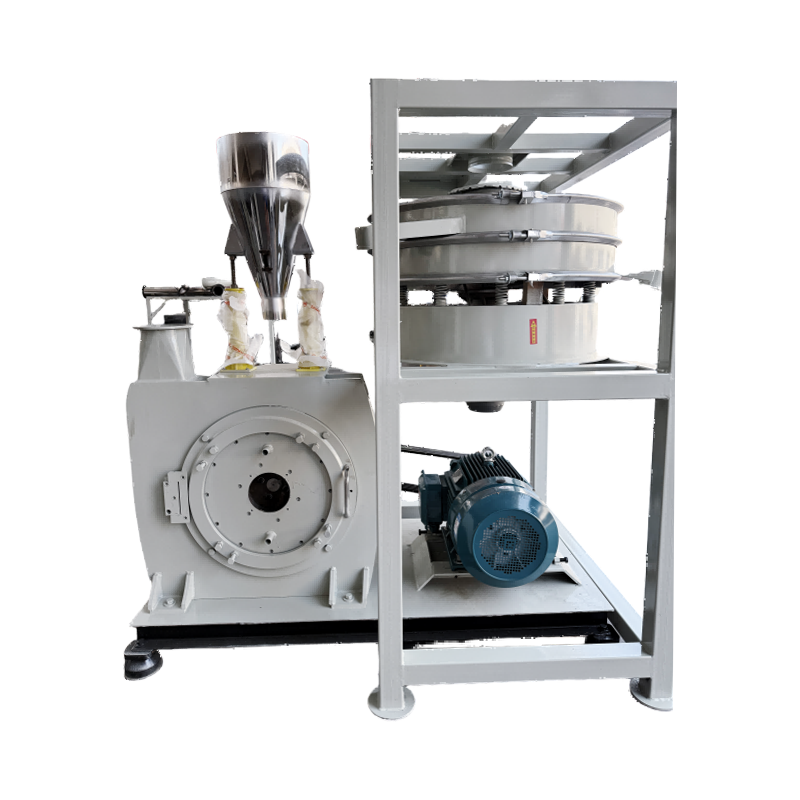
500PA/PP Ambient Temperature Grinder Requires No Liquid Nitrogen
Technical Specifications
The following table summarizes the principal configuration information supplied for the 500 mm PA/PP pulverizer. Capacity and fineness are application-dependent. Actual results may vary according to material type, moisture, feed size, contamination, screen selection, and operating settings.
| Item | Specification | Application Notes |
|---|---|---|
| Machine type | 500 | 500 mm class disc pulverizer |
| Grinding disc diameter | 500 mm | Designed for small and medium production applications |
| Standard capacity | Approximately 50–160 kg/h | Depends on material, fineness, and feed condition |
| Extended application range | Approximately 200–400 kg/h in selected conditions | Requires application-specific evaluation and configuration |
| Typical fineness | 10–30 mesh standard table range | Other screen and gap configurations are available |
| Broader stated fineness range | Approximately 20–100 mesh | Common operating range may be approximately 30–80 mesh |
| Drive motor | 37/45 kW | Selection depends on material and production target |
| Speed control | Star-delta, soft start, or inverter | Inverter control provides additional operating flexibility |
| Grinding disc material | D2 or hardened alloy configuration | High wear resistance for demanding plastic applications |
| Blower motor | 5.5/7.5 kW | Supports pneumatic conveying and discharge |
| Pipe material | Stainless steel | Improves cleanliness and corrosion resistance |
| Pipe diameter | Approximately 159 mm | Suitable for the specified conveying arrangement |
| Vibrating screen diameter | Approximately 1,000 mm | Integrated classification after grinding |
| Vibrating screen motor | 1.1 kW | Provides continuous material separation |
| Feeding method | Vacuum feeding | Supports enclosed and efficient material transfer |
| Dust collector bag diameter | Approximately 300 mm | Supports dust management and cleaner operation |
| Cooling method | Water cooling | Water enters through one connection and exits through another |
| Total installed power | Approximately 50–60 kW in typical configurations | Varies with motor and auxiliary selections |
| Noise level | Below approximately 85 dB | Actual workplace level depends on layout and enclosure |
Processing PA Engineering Plastics
Polyamide recycling often involves materials with high technical value but challenging processing characteristics. PA6 and PA66 waste may come from automotive components, electrical connectors, cable sheathing, textile tow, injection-molded parts, and production scrap. These materials can contain glass fiber, mineral filler, colorants, or other additives that increase wear and influence grinding behavior.
The 500 mm grinder is suited to small and medium batches of PA waste that have already been sorted, cleaned, and reduced to an appropriate feed size. Pulverized PA powder can be used in regeneration granulation, compounding, injection molding, additive or filament development, and selected research applications.
When processing PA, feed preparation is essential. Oversized parts should be reduced before entering the pulverizer. Metal contamination must be removed through magnets, metal detectors, or manual inspection. Moisture should be controlled because PA is hygroscopic and can absorb water from the environment. Excess moisture may affect flow, heat generation, powder behavior, and downstream quality.
Glass-fiber-reinforced PA requires special attention to disc wear and powder classification. The hardened disc configuration helps resist abrasive action, while adjustable speed and gap settings allow the operator to balance throughput against fineness. If the target powder is intended for high-performance compounding, the customer should also test fiber length distribution, ash content, moisture, and thermal properties.
For PA powder used in 3D printing filament development, powder consistency and cleanliness are especially important. The pulverizer can support the preparation of trial material, but the complete filament process also requires drying, compounding, filtration, extrusion, diameter control, and mechanical testing. The grinder is therefore one part of a broader recycling and material-development system.
Processing PP Films and Injection Scrap
Polypropylene waste is widely available from packaging film, injection-molded components, automotive bumpers, containers, caps, and industrial production scrap. PP is relatively lightweight and valuable when recovered in a clean, sorted form. However, frictional heat can soften PP during grinding, causing adhesion and unstable output if the process is not properly controlled.
The ambient-temperature system addresses this issue through water cooling, controlled chamber temperature, adjustable grinding conditions, and vibrating classification. The objective is to produce free-flowing PP powder with uniform fineness and minimal agglomeration.
PP powder may be used as a carrier or component in color masterbatch, filled masterbatch, modified masterbatch, blow molding compounds, injection materials, extrusion formulations, and selected powder coating products. Fine and uniform particles can improve mixing and dispersion, especially when the powder must carry pigments, fillers, stabilizers, or other additives.
For film waste, sorting and cleaning are important because paper, adhesive, metal, and multilayer contamination can reduce product quality. Film should be dry and cut or densified as necessary to ensure stable feeding. For injection scrap and automotive components, the customer should separate incompatible polymers and remove metal inserts before pulverizing.
Operators can adjust the gap and screen according to whether the process prioritizes high throughput or finer particle size. A wider setting may be more suitable for a coarse powder used in a subsequent melt-compounding stage, while a narrower setting may be selected for masterbatch or coating applications requiring better dispersion.
Applications in Recycling, Masterbatch, and Powder Coating
Plastic Recycling
The machine can be integrated into a recycling line after sorting, washing, drying, and preliminary size reduction. In some operations, it may process clean production scrap directly after cutting or granulation. In others, it serves as a secondary size-reduction or powder-preparation stage.
Producing powder rather than only flakes can create additional options for material utilization. Powder may be blended more easily with virgin resin, additives, pigments, and fillers. It may also be suitable for specialized molding, coating, or compounding processes that cannot efficiently use large flakes.
Masterbatch Production
Uniform PA or PP powder can act as a carrier or processing component for color, filler, and functional masterbatch. Consistent particle size supports more uniform additive distribution and can reduce fluctuations during feeding. The powder’s flowability is also important because poor flow may cause bridging, inconsistent dosing, or equipment blockage.
Masterbatch producers often handle many colors and formulations. The compact design, vacuum feeding, integrated screening, and accessible cleaning arrangement can make the 500 mm model useful for short production runs and frequent material switching. A documented cleaning procedure remains necessary when producing light colors or high-purity formulations after dark or highly filled materials.
Powder Coating
The system can support entry-level PP-based powder coating development and small-scale production. Uniform powder helps improve application consistency in electrostatic spraying and fluidized-bed dipping. For trial production, research, and multi-variety operation, a medium-capacity pulverizer can be more appropriate than a large industrial line.
Powder coating performance depends on more than particle size. Melt behavior, resin formulation, additives, charging properties, curing conditions, and substrate preparation all influence final coating quality. The pulverizer should therefore be selected as part of a complete coating development process.
Research and Development
Universities, research centers, and new-material companies often need equipment that can process relatively small quantities while providing repeatable conditions. The 500 mm machine can support trial pulverizing of PA and PP samples, formulation studies, recycled material evaluation, and process validation.
Its adjustable fineness and speed-control options allow researchers to compare different grinding conditions. Sample preparation can be performed without committing to a large production line, making the machine suitable for early-stage development and small-batch customization.
Advantages Compared with Conventional Competitors
Competitor comparisons should always be based on verified application data, but the 500 mm ambient-temperature design offers several structural advantages over basic disc pulverizers and cryogenic systems.
Compared with Basic Non-Cooled Pulverizers
A basic non-cooled pulverizer may have a lower initial purchase price, but it can experience temperature rise during continuous PA or PP processing. This may lead to melt adhesion, unstable powder size, reduced throughput, and frequent cleaning. The water-cooled chamber and intelligent temperature control of this machine are designed to provide more stable operation during demanding production.
The hardened disc configuration is another advantage over ordinary wear parts. A conventional disc may be adequate for clean, unfilled plastics but may wear quickly when processing glass-fiber-reinforced PA or mineral-filled compounds. Longer disc life can reduce maintenance frequency and help preserve product consistency.
Compared with Cryogenic Pulverizers
Cryogenic pulverizers may achieve very low material temperatures, but they require liquid nitrogen or another cryogenic medium. This increases the complexity of storage, supply, safety management, and operating cost. The ambient-temperature grinder avoids routine liquid nitrogen use for the intended PA and PP applications.
For customers with moderate production volumes, the elimination of cryogenic infrastructure can simplify factory planning. It may also make the machine more practical in regions where liquid nitrogen is expensive, difficult to deliver, or subject to supply interruptions.
The ambient-temperature design also supports faster startup and shutdown procedures. Operators do not need to wait for cryogenic equipment to reach a low-temperature operating condition. This can be valuable in research, small-batch, and multi-material production environments.
Compared with Large High-Capacity Lines
Large pulverizing lines can provide greater throughput, but they may require more floor space, higher capital investment, larger labor requirements, and longer cleaning procedures. A 500 mm machine is more suitable when production volumes are moderate, product varieties are numerous, or the customer needs flexible scheduling.
The compact footprint and total power requirement of approximately 50–60 kW in typical configurations can help reduce infrastructure demands. It can also serve as a dedicated line for a specific material or as a flexible secondary machine alongside larger equipment.
Integrated Process Management
The combination of vacuum feeding, pneumatic conveying, water cooling, vibrating screening, stainless-steel piping, dust collection, and adjustable grinding conditions creates a more complete process than a standalone grinding chamber. Fewer disconnected steps can reduce manual handling and material loss.
This integrated approach also improves workflow visibility. Operators can monitor feed, grinding, screening, dust collection, and packaging as connected parts of one process. The result is a cleaner and more organized production area when the system is correctly installed and maintained.
Manufacturing Strengths and Quality Control
The equipment is manufactured by Changzhou Mao Yue Intelligent Equipment Co., Ltd., a Chinese source manufacturer specializing in plastic crushing and pulverizing equipment. The company has accumulated approximately three decades of experience in plastic size reduction and has developed products for rotational molding, masterbatch, polymers, PVC, PE, recycling, and powder coating applications.
The manufacturer operates six processing workshops, each averaging approximately 1,400 square meters. This workshop structure provides space for machining, welding, assembly, testing, storage, and process coordination. A factory with dedicated manufacturing areas can better control production flow than a business that depends entirely on outsourced assembly.
The company uses high-precision grinding machines imported from Taiwan and built according to German standards. Precision grinding is important for pulverizer components because disc flatness, surface finish, concentricity, and dimensional accuracy affect gap adjustment and grinding stability.
German dynamic balancing equipment is used for rotating components. Dynamic balancing helps reduce vibration caused by uneven mass distribution. Lower vibration can improve bearing life, reduce noise, protect the machine frame, and support more stable operation at high spindle speeds.
Japanese welding systems are also identified among the factory’s manufacturing resources. Consistent welding quality is important for the machine frame, pipelines, chambers, hoppers, and other structural components. Proper welding design and inspection help reduce deformation, leakage, and fatigue-related problems.
European-Oriented Component Standards
The company states that its components are manufactured according to European quality standards. The specified European-standard belt pulley arrangement, stainless-steel pipework, and high-precision processing equipment reflect an emphasis on component reliability and serviceability.
European-oriented design does not automatically guarantee performance in every application, but it provides a useful framework for dimensional control, safety, material selection, and component consistency. Customers should still confirm the exact electrical standard, voltage, frequency, guarding, emergency-stop arrangement, and documentation required in their destination country.
Certification and Management Systems
The manufacturer has obtained CE mechanical certification and ISO 9001 quality management system certification. CE certification indicates conformity with relevant European requirements for the applicable machine configuration, while ISO 9001 reflects a formal quality management framework.
Customers should request the relevant certificates, manuals, risk assessment documents, electrical drawings, spare-parts lists, and inspection records for the specific machine supplied. Proper documentation supports installation, operator training, preventive maintenance, and regulatory compliance.
Application-Oriented Engineering
A pulverizer cannot be selected successfully by motor power alone. The manufacturer’s experience across plastics, recycling, masterbatch, and powder coating applications supports a more application-oriented selection process. Material type, feed form, moisture, filler content, desired fineness, output target, and downstream use should all be considered before final configuration.
For a customer processing glass-fiber-reinforced PA, the recommended disc, screen, motor, and wear-part arrangement may differ from the configuration selected for clean PP film. This application-based approach can improve performance and reduce the risk of purchasing an unsuitable standard machine.
Energy, Noise, and Factory Integration
The typical total power requirement is approximately 50–60 kW, depending on the drive motor, blower, screen, feeding arrangement, and other auxiliary components. This places the machine in a practical range for small and medium-sized factories with suitable electrical infrastructure.
Energy consumption should be evaluated per kilogram of finished powder rather than only by installed motor power. Actual energy efficiency depends on the target fineness, feed size, throughput, material hardness, screen resistance, and operating schedule. A higher throughput at a slightly coarser fineness may produce a lower energy cost per kilogram than a low-throughput ultra-fine setting.
The stated noise level is below approximately 85 dB. Actual workplace noise depends on room acoustics, installation foundation, pipe layout, material feed, blower operation, and whether acoustic enclosures are used. Customers should conduct a site-specific noise assessment and provide hearing protection where required by local regulations.
The stainless-steel pipe system helps support cleaner material transfer and may be useful when producing powder for applications with strict contamination control. Vacuum feeding reduces open handling and can help improve the tidiness of the production area. Dust collection is important because fine plastic powder can become airborne during transfer, screening, or bagging.
Recommended factory integration normally includes a stable foundation, adequate ventilation, electrical protection, cooling-water supply, dust-control arrangements, safe access for maintenance, and a suitable finished-product packaging station. The layout should provide sufficient clearance around the disc chamber, motor, screen, blower, dust collector, and control cabinet.
Maintenance and Operating Practices
Regular maintenance is necessary to obtain the expected service life and product consistency. Operators should inspect grinding disc wear, belt tension, bearings, seals, screen condition, blower performance, pipe cleanliness, dust collector bags, and electrical connections according to a documented schedule.
The grinding gap should be checked periodically because vibration, wear, thermal expansion, or incorrect adjustment can affect product fineness. Operators should not attempt to achieve finer powder simply by closing the gap beyond the recommended range. Excessive contact may increase heat, energy consumption, wear, and the risk of equipment damage.
Cooling-water quality and flow should also be monitored. Blocked lines, insufficient flow, leaks, or poor water quality can reduce heat-transfer performance. If the factory uses recirculated water, filtration and routine inspection may be required to prevent scale or contamination from affecting the cooling system.
The screen should be cleaned when powder buildup reduces classification efficiency. Different materials may require different cleaning procedures, especially when changing from dark to light colors or from filled compounds to unfilled resin. A carefully controlled changeover procedure can minimize cross-contamination.
Feedstock preparation is one of the most effective ways to protect the machine. Operators should remove metal, stones, excessive moisture, and incompatible materials before feeding. Large pieces should be reduced to a size compatible with the feed opening. Stable feed preparation improves capacity, reduces overload risk, and supports a more consistent powder.
Suggested Preventive Maintenance Schedule
Before each shift, operators should inspect the machine for unusual noise, vibration, leaks, loose fasteners, abnormal temperature, and visible dust leakage. The cooling-water circuit and dust collection system should be checked before production begins.
During operation, operators should monitor motor current, product appearance, powder temperature, feed consistency, and screen output. A sudden change in motor load or powder flow may indicate blockage, disc wear, excessive moisture, or a change in feed composition.
At regular weekly or monthly intervals, the maintenance team should inspect belts, bearings, screen fasteners, pipe connections, electrical terminals, and safety devices. The exact interval depends on working hours and material abrasiveness.
When replacing a disc or opening the grinding chamber, the machine must be isolated from all energy sources. Lockout and tagout procedures should be applied, and only trained personnel should perform internal maintenance.
How to Select the Correct Configuration
Customers should begin by defining the material. PA6, PA66, PP film, injection scrap, glass-fiber-reinforced PA, mineral-filled PP, and powder coating formulations can have significantly different grinding characteristics.
The next step is to define the feed form. Clean pre-cut parts, compacted film, flakes, runners, molded components, and laboratory samples may require different feeding and pre-processing arrangements.
The target powder size should then be specified. A customer seeking 10–30 mesh powder may select a different screen and operating condition from a customer seeking 60–100 mesh powder. If a narrow distribution is required, laboratory testing should confirm the appropriate screen, gap, spindle speed, and feed rate.
Expected production should be expressed as finished powder per hour, not simply incoming feed rate. Losses from screening, dust collection, oversize recycling, and cleaning should be considered when calculating the required capacity.
Finally, the customer should evaluate downstream use. Powder for masterbatch, injection compounding, powder coating, research, or filament development may have different requirements for moisture, contamination, particle shape, flowability, and thermal history.
Installation and Commissioning
Installation should be carried out on a level and sufficiently strong foundation. The machine should be aligned according to the manufacturer’s instructions, and rotating components should be checked before startup. The electrical supply must match the selected motor and control configuration.
The cooling-water system should be tested for flow, pressure, leaks, and temperature-control response before material is introduced. The dust collection system should be connected and operating before pulverizing begins. Pipe joints should be sealed properly to prevent powder leakage and air loss.
Commissioning should begin with a clean and known feedstock. Operators can then gradually adjust feed rate, disc gap, speed, cooling conditions, and screen configuration while recording motor current and powder quality. The first production trials should be used to establish a process recipe for each material.
Training should cover safe startup and shutdown, emergency stopping, screen replacement, disc inspection, cleaning, cooling-water management, dust control, and lockout procedures. Well-trained operators are more likely to identify abnormal conditions before they develop into serious failures.
Quality Evaluation of Finished Powder
Finished powder should be evaluated according to its intended use. Basic checks may include visual appearance, color, odor, moisture, particle size, flowability, bulk density, and contamination. More advanced evaluations may include melt flow rate, ash content, thermal analysis, tensile properties after reprocessing, and microscopic particle examination.
For recycled PA, moisture content and thermal history are especially important. For glass-filled material, filler distribution and ash content should be checked. For PP masterbatch applications, color dispersion, flow behavior, and compatibility with the selected carrier system should be evaluated.
Powder samples should be collected from different points in a production run rather than from only one initial sample. This helps identify variations caused by temperature buildup, disc wear, feed changes, or screen loading.
Q&A
What materials can the 500 mm grinder process?
The primary applications are PA6, PA66, PP film, PP injection scrap, automotive plastic parts, containers, cable sheathing, textile waste, masterbatch materials, and selected powder coating materials. The exact suitability depends on feed preparation, moisture, fillers, contamination, and target fineness.
Does the machine require liquid nitrogen?
No. The machine is designed for ambient-temperature pulverizing with water cooling and intelligent temperature management. It is intended to process suitable PA and PP materials without routine liquid nitrogen use.
What is the actual production capacity?
The standard technical table lists approximately 50–160 kg/h. The broader product information refers to approximately 200–400 kg/h under selected conditions. Capacity varies with material, moisture, feed size, target mesh, screen configuration, motor selection, and operating settings. A material test is recommended for a reliable production estimate.
What particle size can be produced?
The standard table lists approximately 10–30 mesh, while the product description identifies a broader range of approximately 20–100 mesh and a common range of 30–80 mesh. Alternative configurations may support finer or different particle sizes. Final results must be confirmed through testing because mesh output depends strongly on the material and screen.
Can it process glass-fiber-reinforced PA?
Yes, the machine is designed to support glass-fiber-reinforced PA applications, and its wear-resistant disc configuration is intended to reduce accelerated wear. Customers should provide information about fiber content, filler type, contamination, and target powder size so that the appropriate disc and operating parameters can be selected.
How is the machine cooled?
The grinding system uses water cooling. One connection serves as the water inlet and another as the outlet. The intelligent temperature control system regulates operating conditions to help prevent excessive heat, melt adhesion, and thermal degradation.
Is the screen included?
The described configuration includes an integrated vibrating screen with an approximate diameter of 1,000 mm and a 1.1 kW motor. Screen selection and final configuration should be confirmed according to the required product fineness.
What type of feeding system is used?
The specified feeding method is vacuum feeding. This supports enclosed material transfer and can help reduce manual handling, dust escape, and feeding interruptions.
How often must the grinding disc be replaced?
Disc life depends on material abrasiveness, filler content, contamination, operating gap, speed, feed rate, and maintenance. The product information indicates approximately 600–800 hours of continuous operation under suitable conditions and states that the hardened disc can provide approximately twice the service life of standard discs. Actual replacement timing should be based on wear inspection and product-quality results.
Is the machine suitable for a laboratory?
It can be suitable for universities, research institutions, material companies, and small-batch development, particularly where a flexible system is preferred. However, the 500 mm size is an industrial machine rather than a benchtop unit. The customer should confirm whether the capacity, floor space, power supply, and cleaning requirements match the research program.
Can the machine be used for powder coating?
It can support entry-level PP-based powder coating development and small-scale production. Powder coating performance depends on the complete formulation and application process, including resin selection, additives, particle size, charging, curing, and substrate preparation.
What information should be provided for a quotation?
Customers should provide the material type, feed form, filler content, moisture condition, expected hourly output, target particle size, electrical standard, working hours, downstream use, and any special cleanliness or automation requirements. Supplying representative samples for testing can improve configuration accuracy.
Conclusion
The 500 mm ambient-temperature grinder provides a practical solution for PA and PP pulverizing where stable powder quality, moderate capacity, flexible production, and controlled investment are important. Its water-cooled grinding chamber reduces reliance on liquid nitrogen, while temperature control helps prevent overheating, PP adhesion, and PA thermal degradation.
The combination of a wear-resistant grinding disc, adjustable gap, variable speed options, vacuum feeding, stainless-steel conveying pipes, vibrating screening, and dust collection creates a complete and adaptable processing system. It is appropriate for recycling, masterbatch, powder coating, research, and small-batch material development.
Compared with basic non-cooled machines, it offers stronger control over heat and wear. Compared with cryogenic equipment, it provides a simpler operating model without routine liquid nitrogen consumption. Compared with oversized production lines, it offers a more compact and accessible solution for small and medium-sized factories.
Its performance is supported by the manufacturer’s experience in plastic pulverization, multi-workshop production structure, precision machining equipment, dynamic balancing capability, welding resources, quality management certification, and application-oriented engineering. When correctly configured and maintained, the machine can help processors convert PA and PP waste into uniform, useful powder for higher-value downstream applications.
References
1. Product technical specification sheet for the 500 mm PA/PP ambient-temperature pulverizer.
2. Manufacturer-provided application information for PA6, PA66, PP film, injection scrap, masterbatch, recycling, and powder coating.
3. Manufacturer-provided information regarding grinding disc materials, wear resistance, temperature control, and operating life.
4. ISO 9001 quality management system principles for manufacturing and process control.
5. General industrial guidance on plastic recycling, particle-size classification, dust control, and preventive maintenance.
6. General engineering principles for disc pulverizer design, rotating equipment balancing, water cooling, and pneumatic conveying.
7. General safety practices for industrial machinery, electrical isolation, rotating equipment, dust management, and lockout procedures.