

 English
 русский
 Español
 عربى
 中文简体
 中文简体
Content
- 1 1. Why Integrated Plastic Size Reduction Matters
- 2 2. Main Process Flow
- 3 3. Product Advantages Over Conventional Crushing and Pulverizing Systems
- 4 4. Technical Configuration and Operating Specifications
- 5 5. Manufacturing Quality and Engineering Strength
- 6 6. Intelligent Control and Automation
- 7 7. Material Applications
- 8 8. Powder Quality and Downstream Value
- 9 9. Installation, Operation, and Maintenance Considerations
- 10 10. Economic and Environmental Benefits
- 11 11. Why Manufacturer Experience Matters
- 12 12. Recommended Selection Procedure
- 13 13. Frequently Asked Questions
- 13.1 13.1 What types of plastic can the line process?
- 13.2 13.2 Can it process large pipes and profiles?
- 13.3 13.3 What final powder size can be achieved?
- 13.4 13.4 Is the line suitable for rotational-molding powder?
- 13.5 13.5 How does the system control grinding temperature?
- 13.6 13.6 How does the line reduce dust emissions?
- 13.7 13.7 What prevents the crusher from jamming?
- 13.8 13.8 Can the line be customized?
- 13.9 13.9 What maintenance is required?
- 13.10 13.10 What certifications does the manufacturer have?
- 13.11 13.11 How should the capacity be evaluated?
- 13.12 13.12 Is the line suitable for a centralized recycling plant?
- 14 14. Conclusion
- 15 References
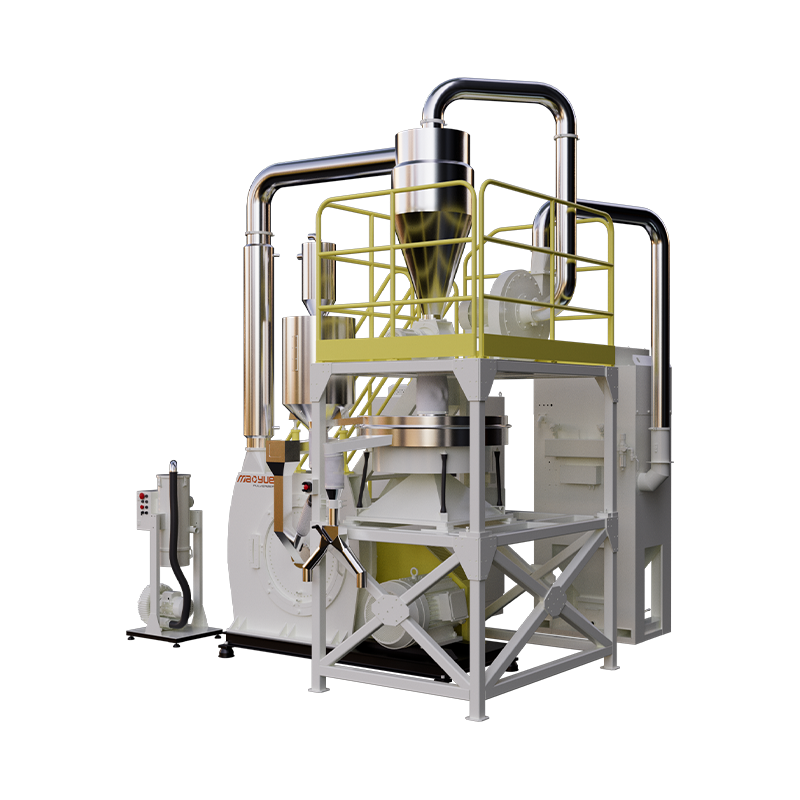
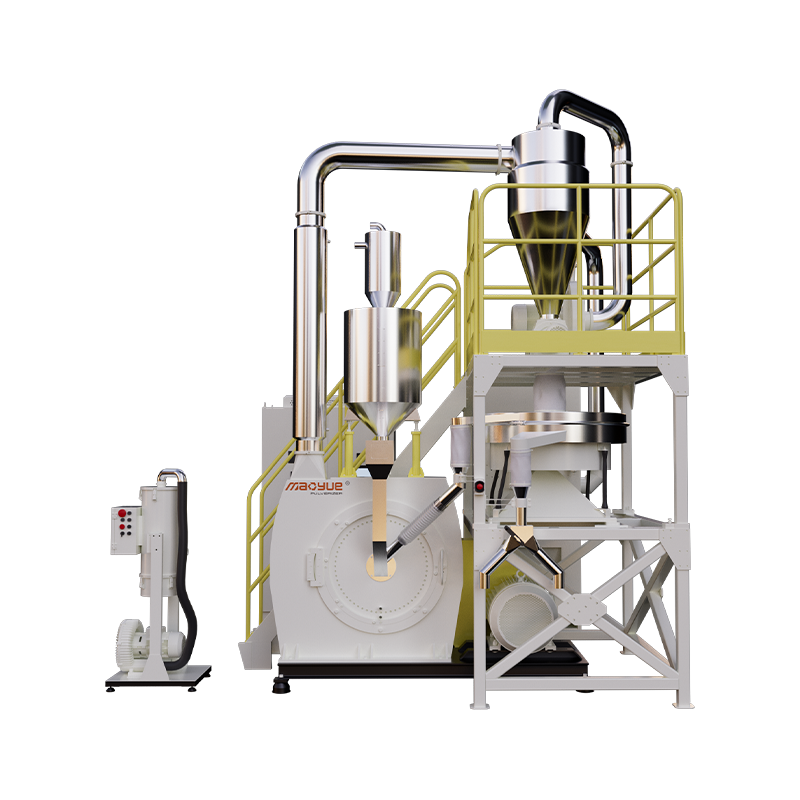
- 16 Product: Hammer-impact swing-knife crushing and pulverizing production line
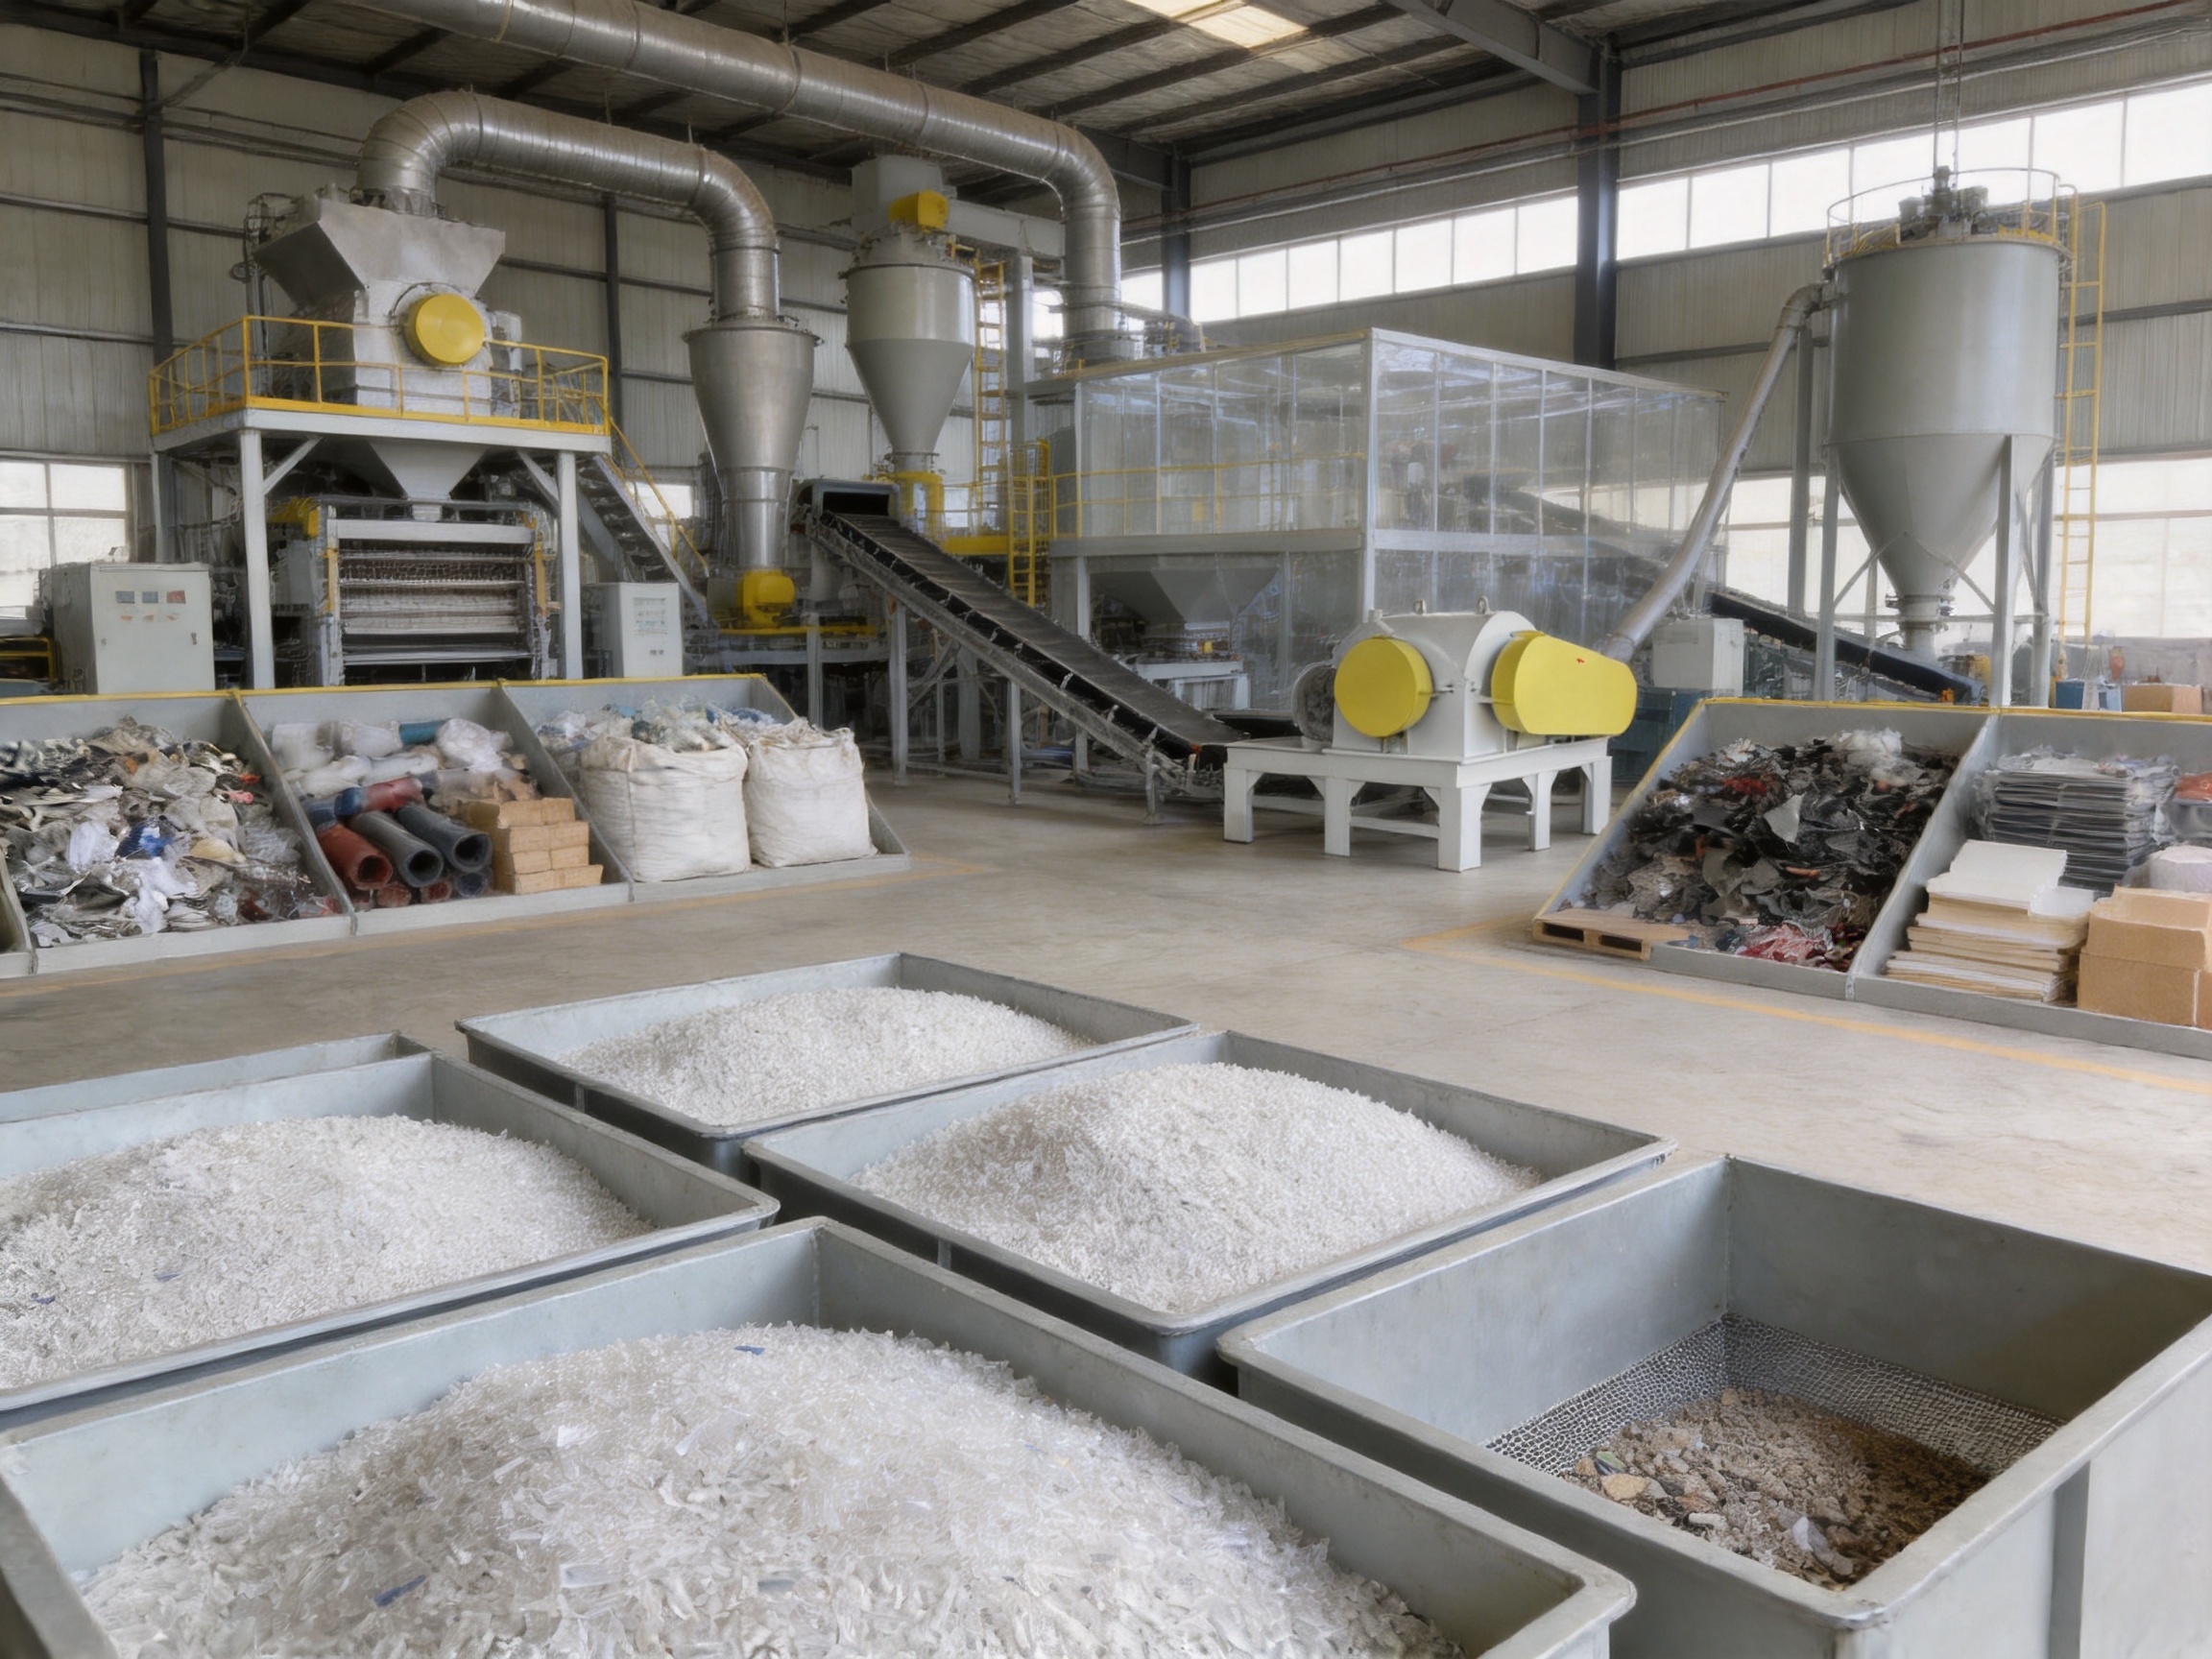
Plastic recycling increasingly depends on equipment that can process difficult, irregular, and contaminated feedstock while producing a consistent material for reuse. Large pipes, profiles, sheets, foam boards, woven bags, pallets, barrels, flooring scraps, appliance housings, and other plastic waste cannot always be handled efficiently by a single conventional crusher or pulverizer. They often require a coordinated sequence of coarse size reduction, fine grinding, conveying, separation, screening, cooling, and dust control.
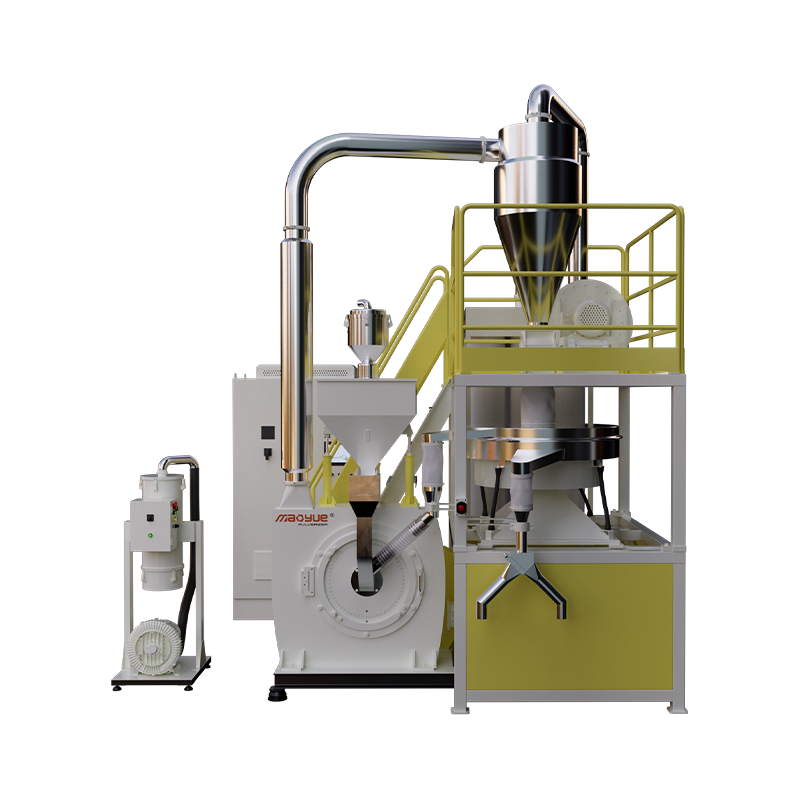
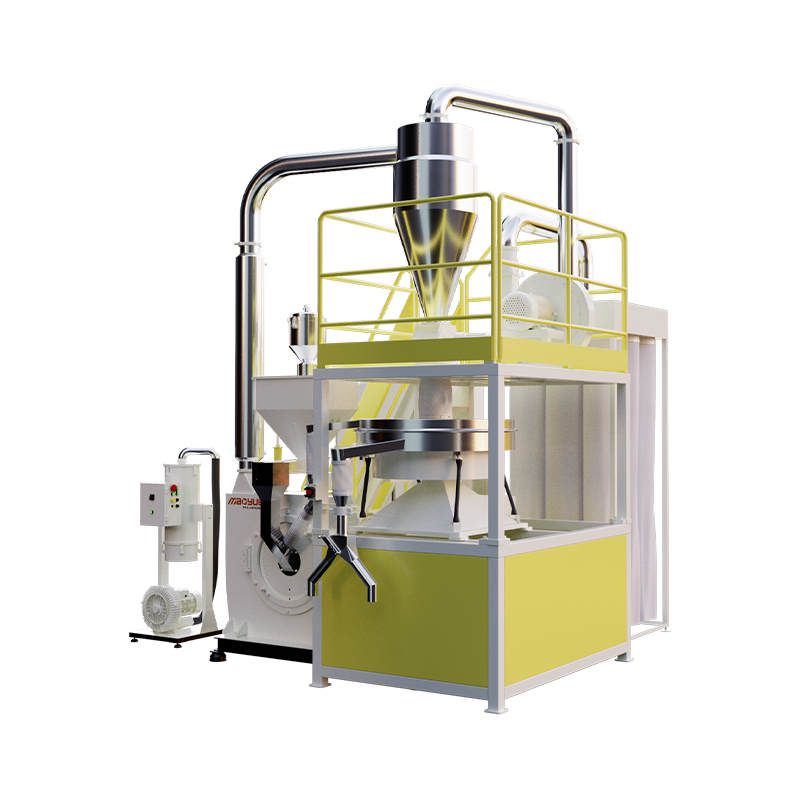
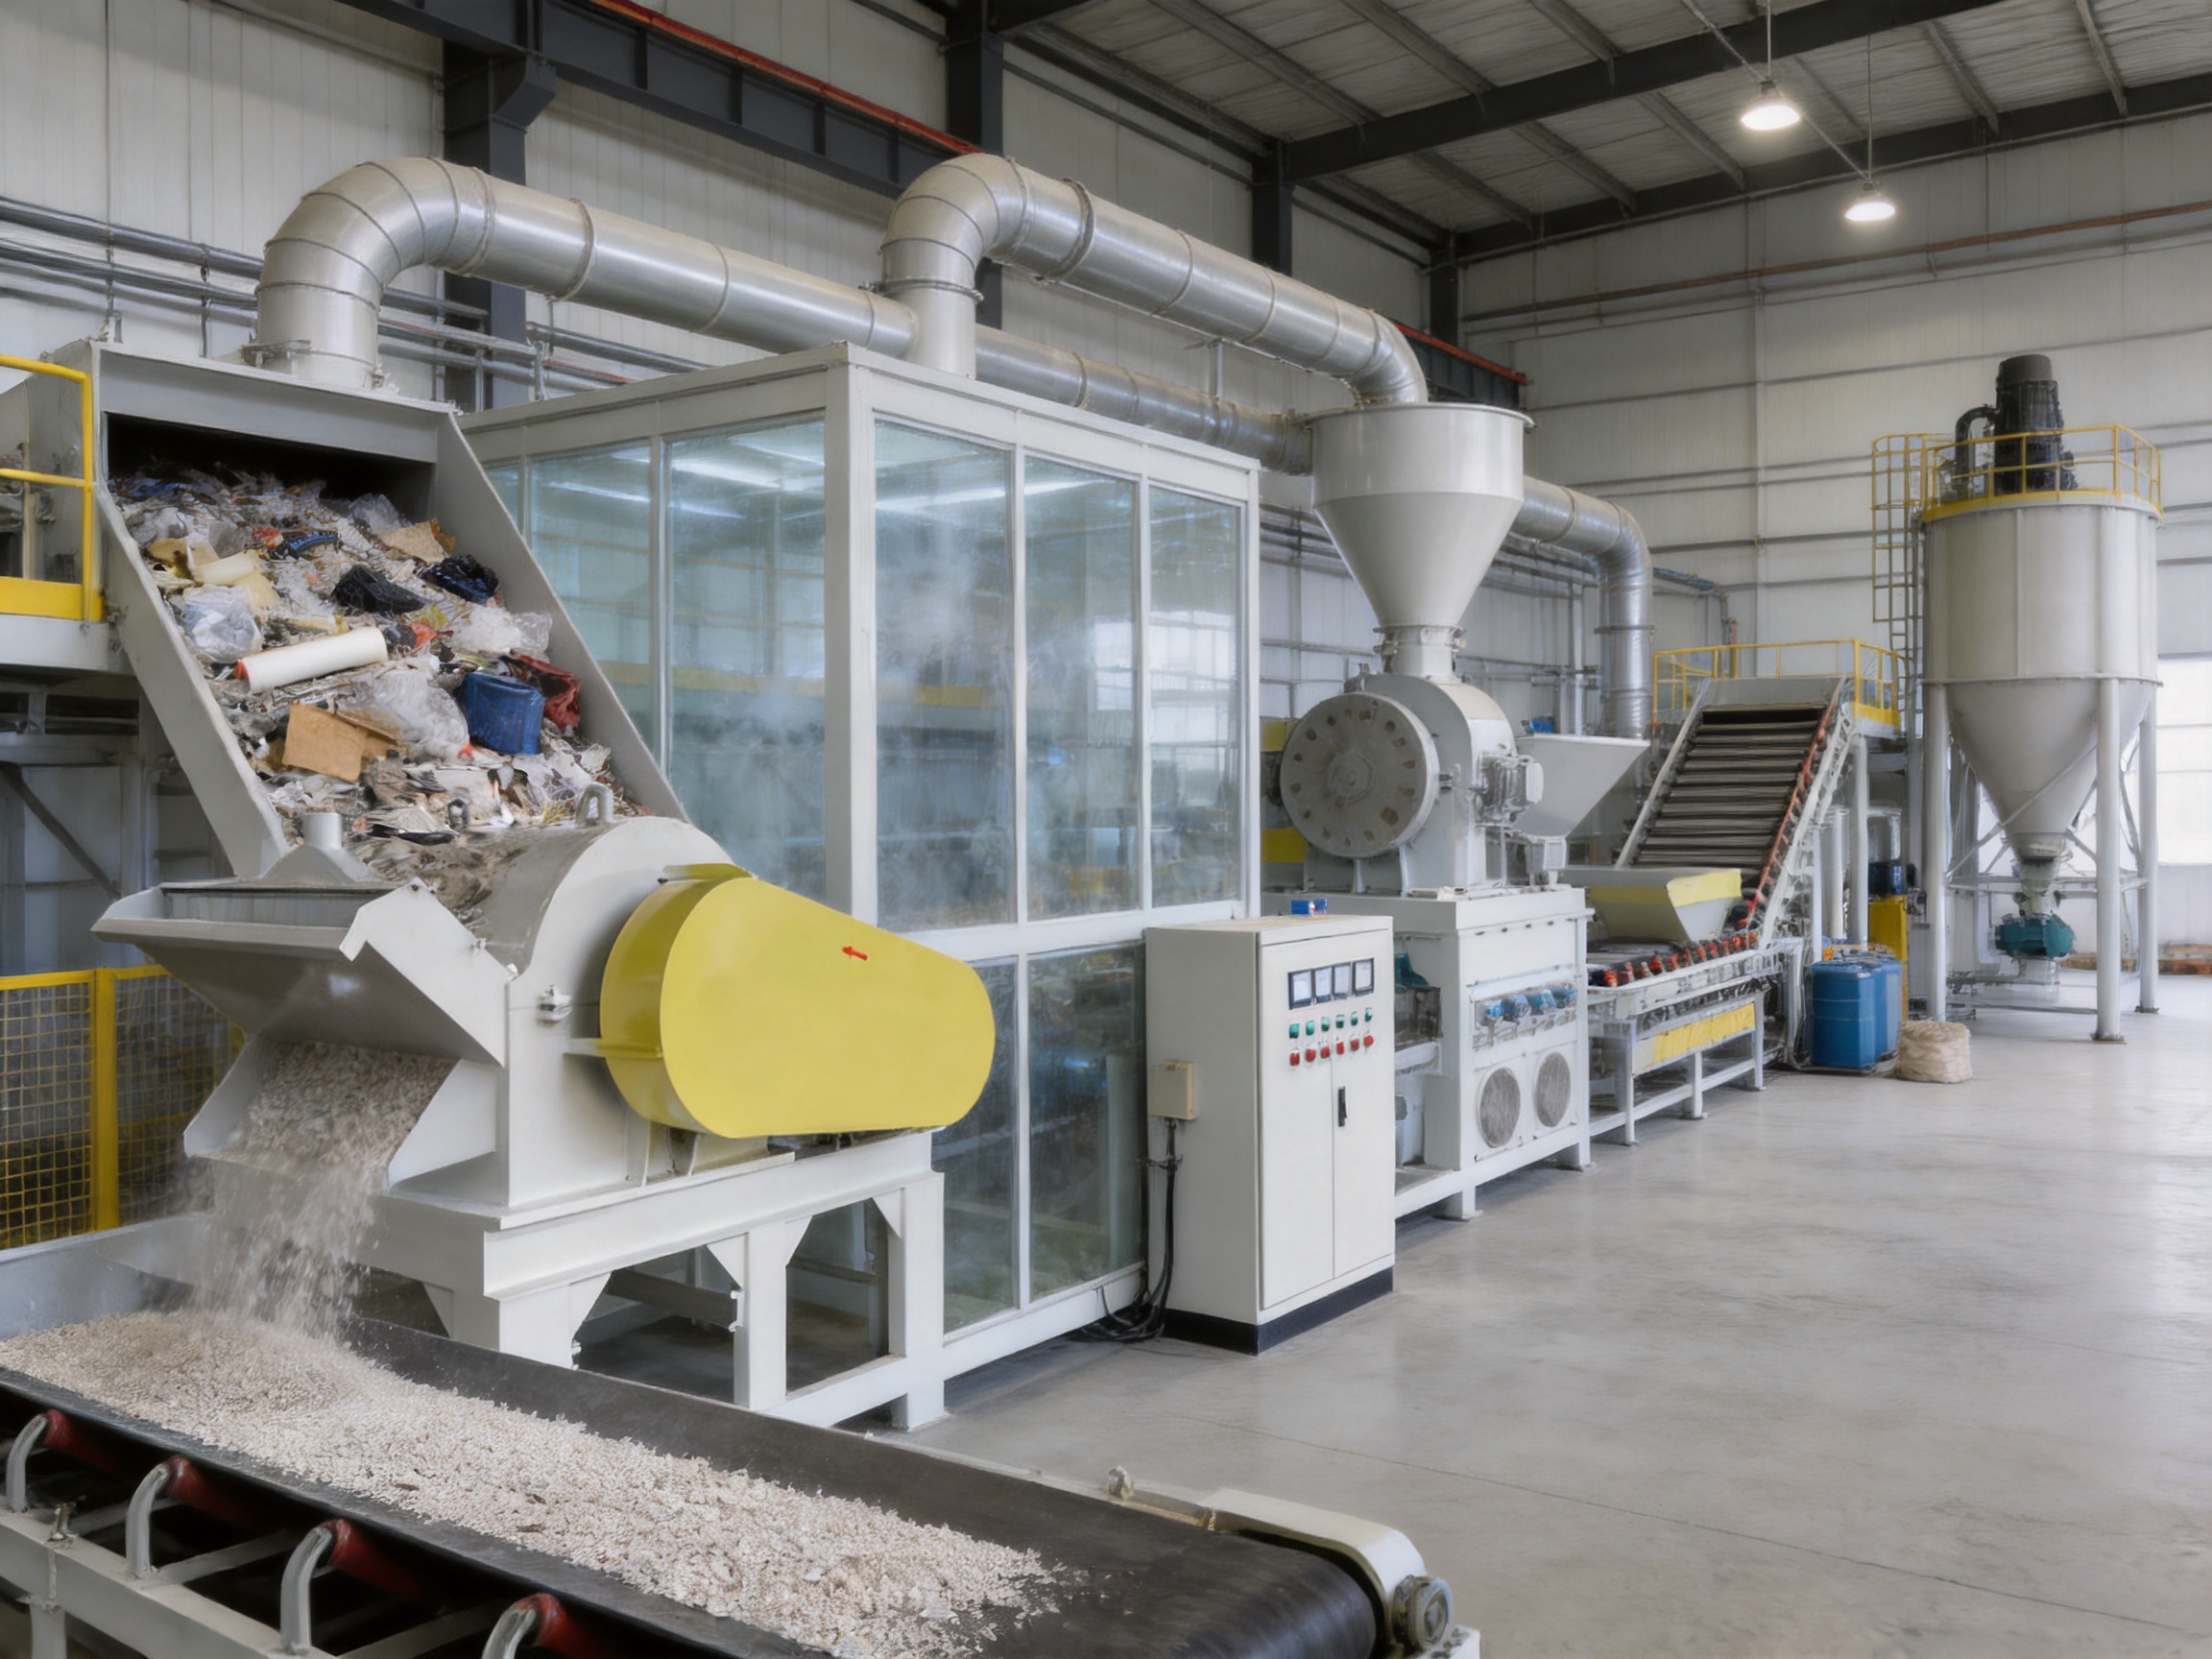
The hammer-impact swing-knife crushing and pulverizing production line is designed as an integrated answer to this challenge. It combines a heavy-duty hammer-blade coarse crusher with a precision disc mill, negative-pressure conveying, cyclone separation, vibrating screening, temperature-control equipment, and pulse dust collection. Instead of treating crushing and pulverizing as isolated operations, the line connects them into a continuous process capable of converting large plastic waste into uniform fine powder.
Depending on the material, operating conditions, and final application, the system can produce powder in the approximate range of 20 to 80 mesh or finer. The line is suitable for PVC, PE, PP, PET, ABS, EVA, and other medium-hardness or high-impact plastics. It is particularly valuable in rotational molding, SPC flooring, pipe and profile production, sheet manufacturing, plastic compounding, engineering-plastic recycling, and centralized waste treatment.
1. Why Integrated Plastic Size Reduction Matters
Plastic waste is rarely uniform. A recycling plant may receive thin films, thick pipe sections, rigid profiles, sheet offcuts, foam boards, injection-molded parts, woven sacks, and bulky molded products on the same day. These materials vary in thickness, toughness, elasticity, moisture content, and heat sensitivity. A machine optimized for one type of waste may perform poorly when the feedstock changes.
Traditional recycling arrangements often use separate machines for coarse crushing and fine pulverizing. Although this configuration can work, it frequently creates transfer points between machines. Operators may need to manually move intermediate material, inspect particle size, clear blockages, and adjust each machine independently. The additional labor increases operating costs and can reduce production stability.
An integrated crushing and pulverizing line reduces these difficulties by coordinating the entire material flow. Large pieces enter the front-end hammer-impact crusher, where they are reduced to a controlled intermediate size. The crushed material then moves through enclosed conveying equipment to the disc pulverizer. After fine grinding, the powder is separated, screened, and collected. Oversize material can be returned or adjusted through the screening system according to the production requirement.
This arrangement offers several practical benefits:
First, it reduces manual handling. Operators can manage feeding, grinding, screening, and dust collection through a centralized control system rather than supervising every transfer step individually.
Second, it improves process continuity. The crusher and pulverizer are selected to work as parts of one line, reducing the mismatch that can occur when unrelated machines are connected together.
Third, it improves cleanliness and material recovery. Enclosed negative-pressure conveying helps prevent fine powder from escaping into the workshop, while pulse dust collection captures airborne particles and returns the working environment to a safer condition.
Fourth, it supports a wider range of applications. The line can be configured for rigid PVC waste, PE and PP rotational-molding scrap, engineering plastics, foam materials, and other recyclable plastics requiring different degrees of size reduction.
2. Main Process Flow
The production line is built around a logical sequence that takes material from large waste pieces to controlled fine powder. Although the exact equipment arrangement can be customized, the standard process includes feeding, hammer-impact crushing, pneumatic conveying, disc pulverizing, cyclone separation, vibrating screening, and dust collection.
2.1 Feeding and Preliminary Material Preparation
Plastic waste is supplied to the front-end crusher through a suitable feeding system. The feeding opening can be customized according to the dimensions and form of the raw material. Large pipe sections, profiles, sheets, foam boards, woven bags, pallets, and molded products can be introduced without the extensive manual size reduction required by many small conventional grinders.
Before feeding, the material should be checked for metal, stones, excessive moisture, and other foreign objects. Removing hard contaminants helps protect the blades, grinding discs, bearings, and conveying equipment. Material preparation also improves overall throughput and reduces the likelihood of unplanned stoppages.
2.2 Hammer-Impact Coarse Crushing
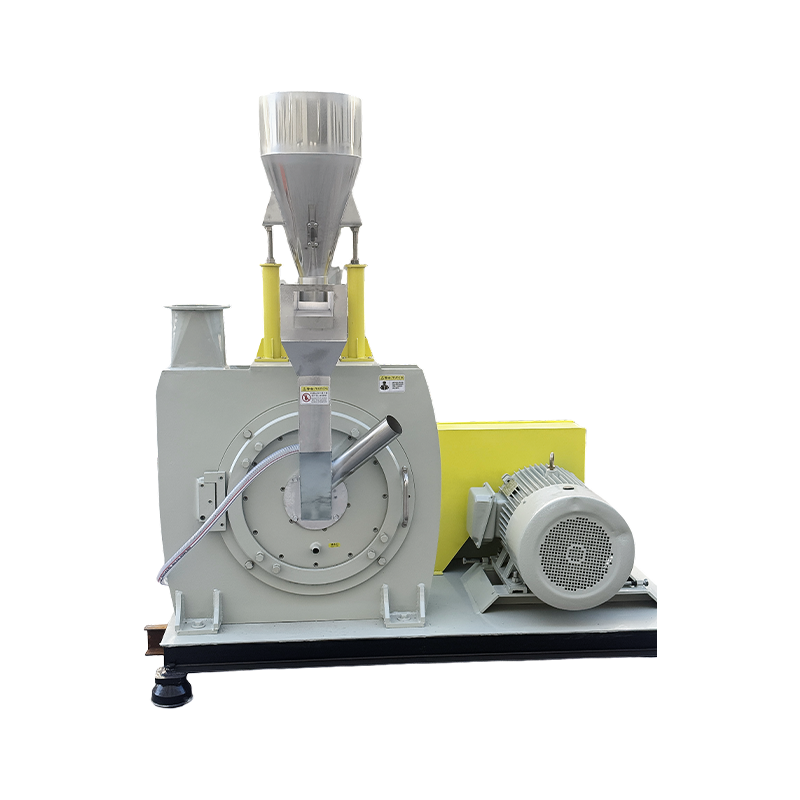
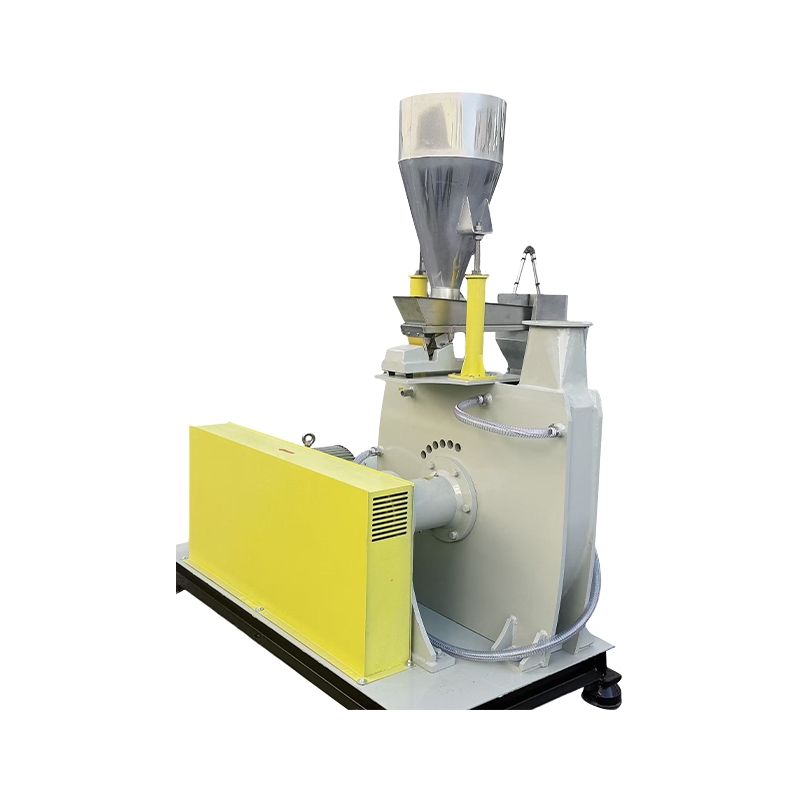
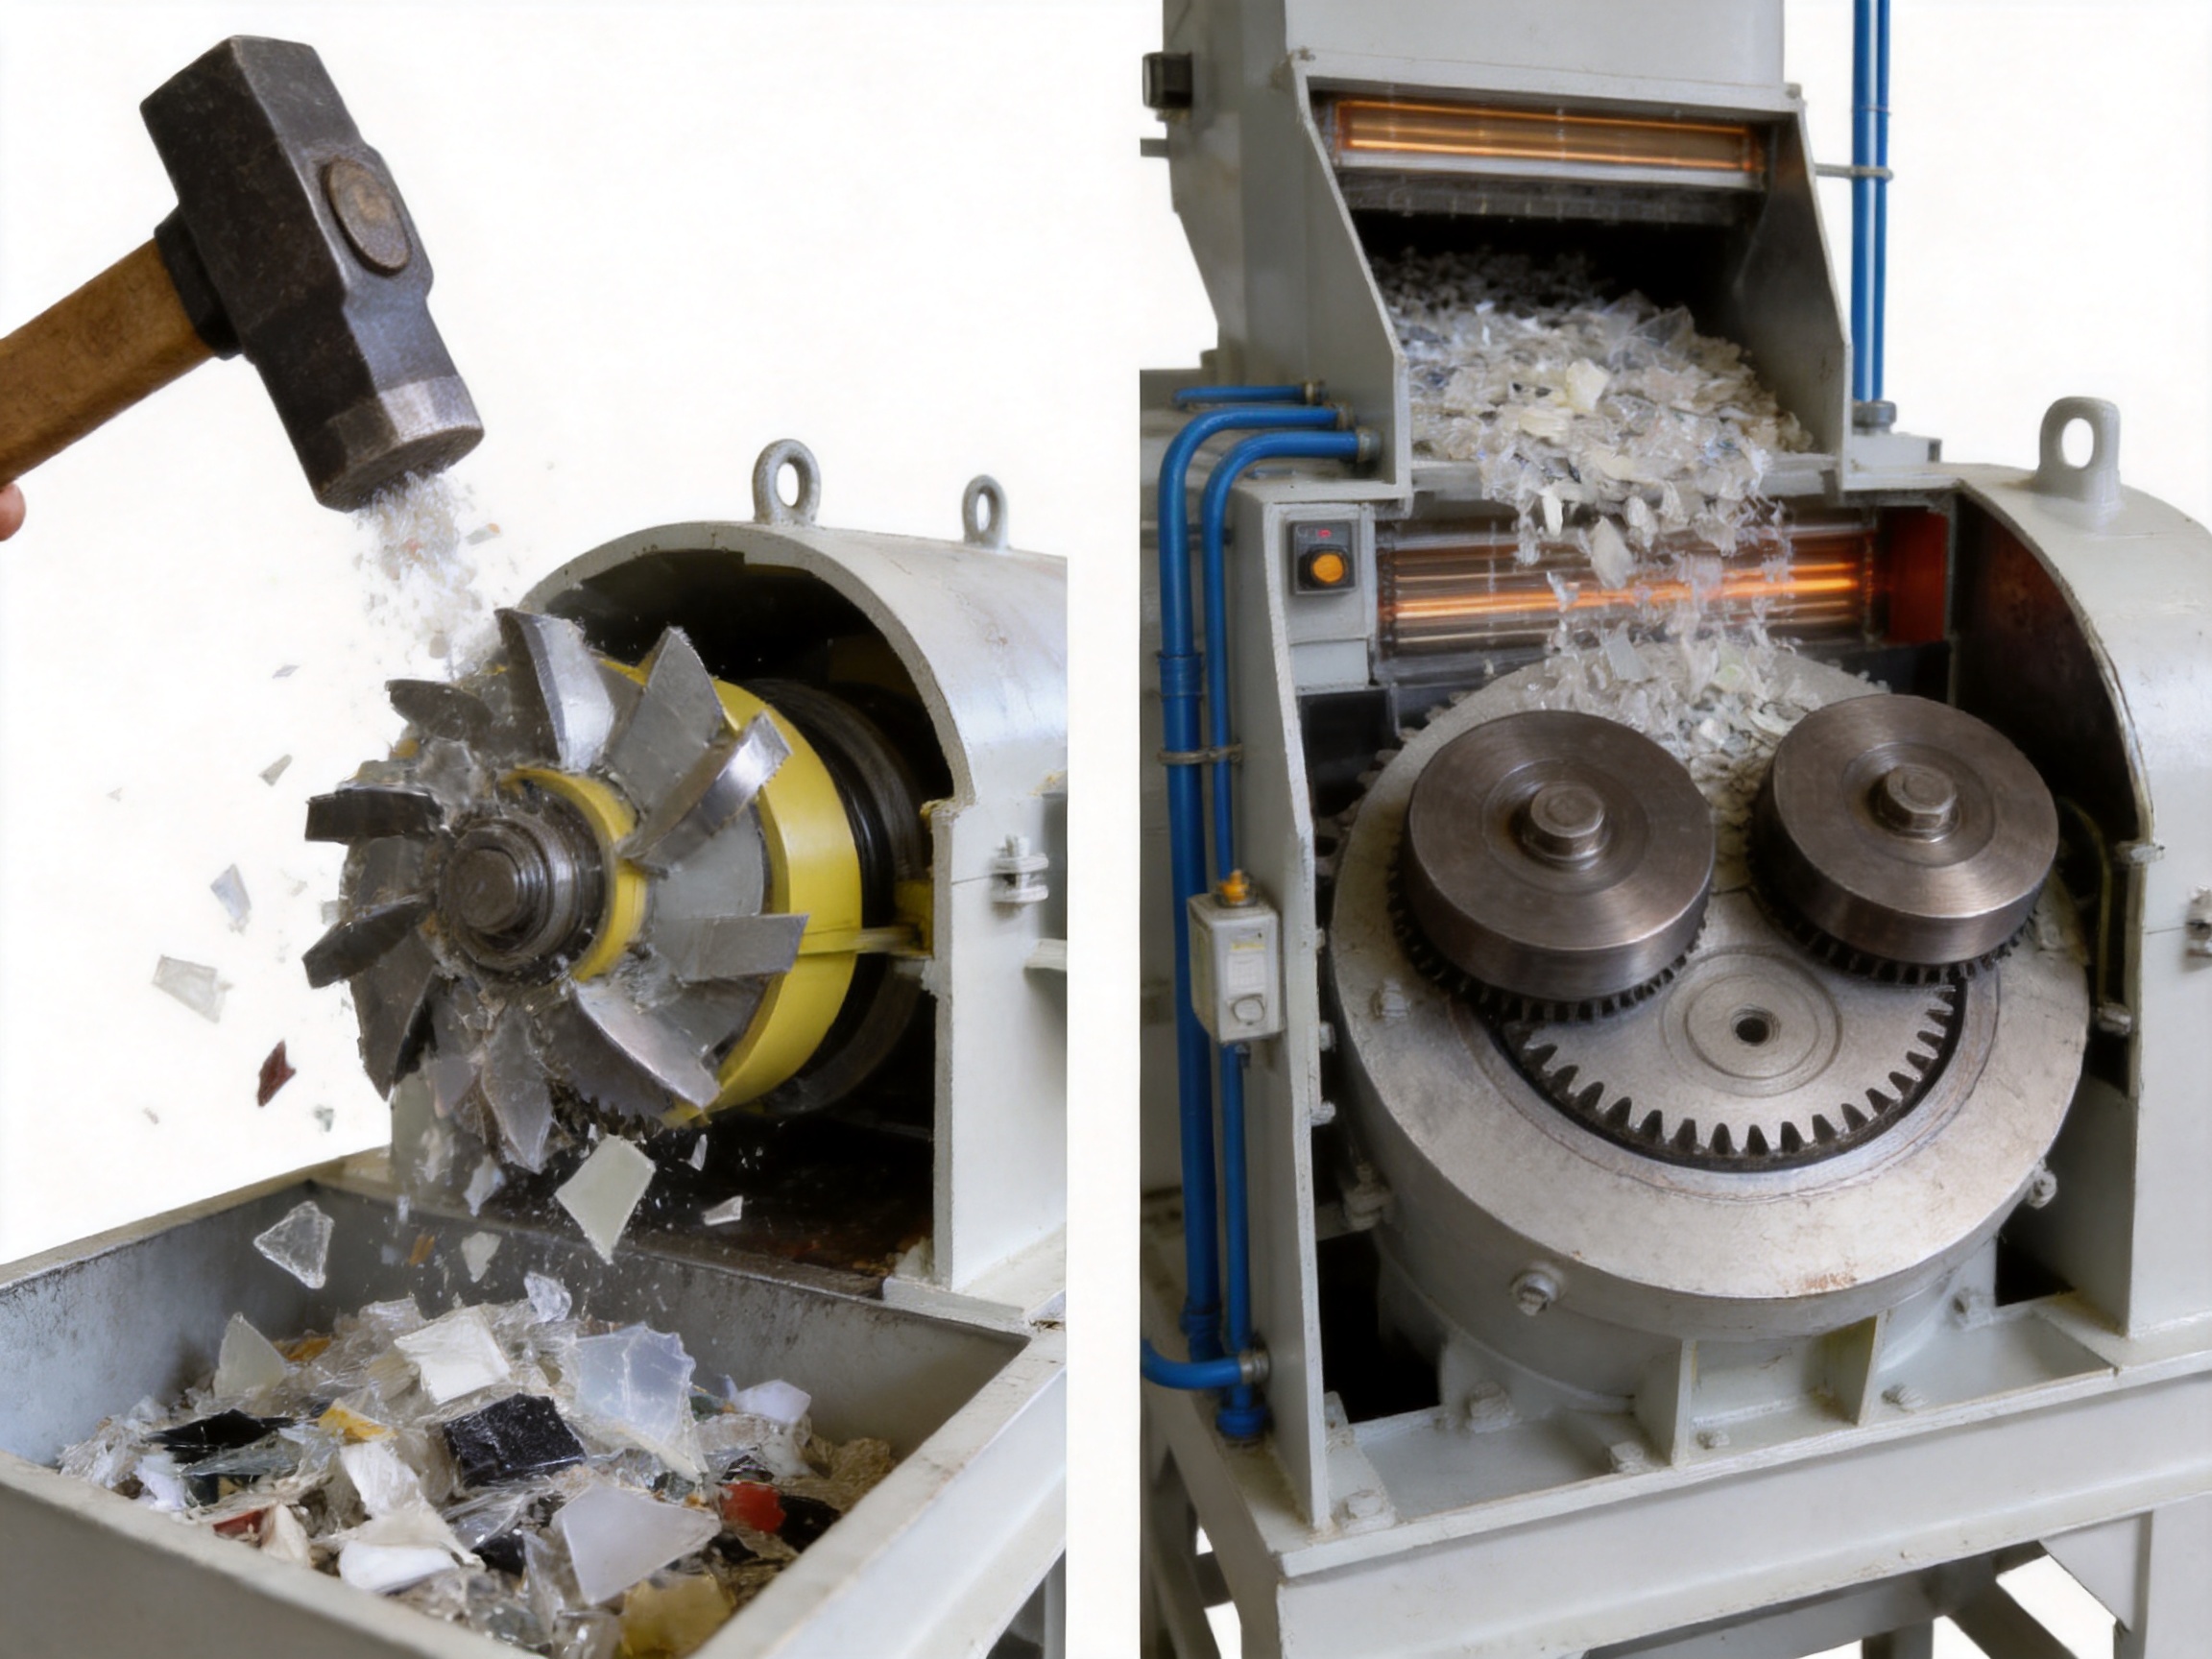
The first major stage uses a heavy-duty hammer-impact swing-knife structure. High-speed rotating knives generate combined impact, shearing, and tearing forces. This combination allows the machine to break large and irregular plastic waste into controlled pieces more effectively than a simple cutting action alone.
The coarse crusher is designed to handle materials that may be difficult for a conventional knife crusher. Flexible plastics can wrap around ordinary blades, while long pipes and profiles can bridge across a feed opening. The hammer-impact action helps break the material before it has time to form long entangled strands. The design therefore reduces the risk of jamming and improves feeding stability.
The coarse crushing particle size can be adjusted within a practical range according to the feedstock and downstream grinding requirements. The supplied specification identifies a nominal 16 millimeter mesh or sizing configuration for the listed type, while the broader product description indicates an adjustable intermediate particle range of approximately 5 to 20 millimeters. Actual results depend on material properties, knife condition, feed rate, and screen configuration.
By preparing a more uniform intermediate material, the coarse crusher protects the disc pulverizer from sudden overloads. It also helps the fine-grinding section maintain a stable feed rate, which is essential for consistent powder quality.
2.3 Negative-Pressure Conveying
After coarse crushing, the material is transported through an enclosed negative-pressure conveying system. Unlike open mechanical transfer, pneumatic conveying limits contact between the intermediate material and the surrounding workshop. This is especially important when the material is small, lightweight, or likely to generate dust.
Negative-pressure operation helps control the direction of airflow. Air and material move toward the collection and separation equipment rather than escaping outward through gaps. This arrangement supports cleaner production, reduces material loss, and helps protect workers from exposure to airborne plastic particles.
The conveying system also creates a more flexible equipment layout. Individual machines do not necessarily need to be positioned in a straight line, allowing the production line to fit different factory spaces. Modular equipment placement can simplify future expansion or relocation.
2.4 Precision Disc Pulverizing
The fine-grinding stage uses a disc pulverizer available in different model classes, including 500, 600, and 800 configurations. The grinding discs are made from DC53 high-grade mold steel, selected for hardness, wear resistance, and suitability for demanding size-reduction work.
The grinding disc geometry is produced using high-precision tooth-by-tooth machining. Accurate tooth profiles help create a more consistent grinding gap and a more controlled reduction process. The discs are also dynamically balanced to reduce vibration during high-speed operation. Proper balance improves mechanical stability, protects bearings, and supports a longer service life for the machine structure.
The disc mill is responsible for transforming the pre-crushed particles into fine powder. The final size depends on the material, disc gap, rotor speed, feed rate, cooling performance, and screening arrangement. Applications may require powder in the approximate range of 20 to 80 mesh or finer. Rotational-molding powder and SPC core-layer powder generally require good uniformity, dispersion, and flowability, so the grinding section must be adjusted carefully rather than operated only at maximum speed.
2.5 Cyclone Separation and Screening
Following pulverizing, the ground material is carried into the separation section. Cyclone separation uses airflow and centrifugal movement to separate powder from the conveying stream. This helps stabilize the transfer of fine material and reduces the amount of powder remaining in the air path.
Vibrating screening provides an additional method of controlling the final product. It separates material according to the required particle size and can help remove oversize particles from the finished powder. A well-adjusted screening system improves batch consistency, which is important when the powder is reused in extrusion, rotational molding, flooring production, or compounding.
Screening can also support closed-loop operation. Material that does not meet the target size may be returned for additional grinding or directed to a separate outlet. This reduces the risk that coarse particles will contaminate the final product.
2.6 Pulse Dust Collection
The line uses high-efficiency pulse bag dust collection to control fine particles generated during crushing, conveying, grinding, separation, and screening. The stated dust-capture efficiency is greater than 99.9 percent under suitable operating conditions. Actual environmental performance depends on correct installation, sealing, airflow adjustment, filter maintenance, and compliance with local regulations.
Pulse cleaning uses compressed air to remove accumulated dust from the filter bags. The cleaning cycle helps maintain airflow and prevents excessive filter resistance. By collecting fine powder rather than allowing it to escape, the system improves raw material utilization and supports a cleaner workshop.
Dust control is not only an environmental requirement. It is also a production and maintenance issue. Uncontrolled powder can settle on motors, electrical cabinets, bearings, platforms, and ventilation surfaces. Effective collection helps reduce cleaning requirements and supports safer access for operators.
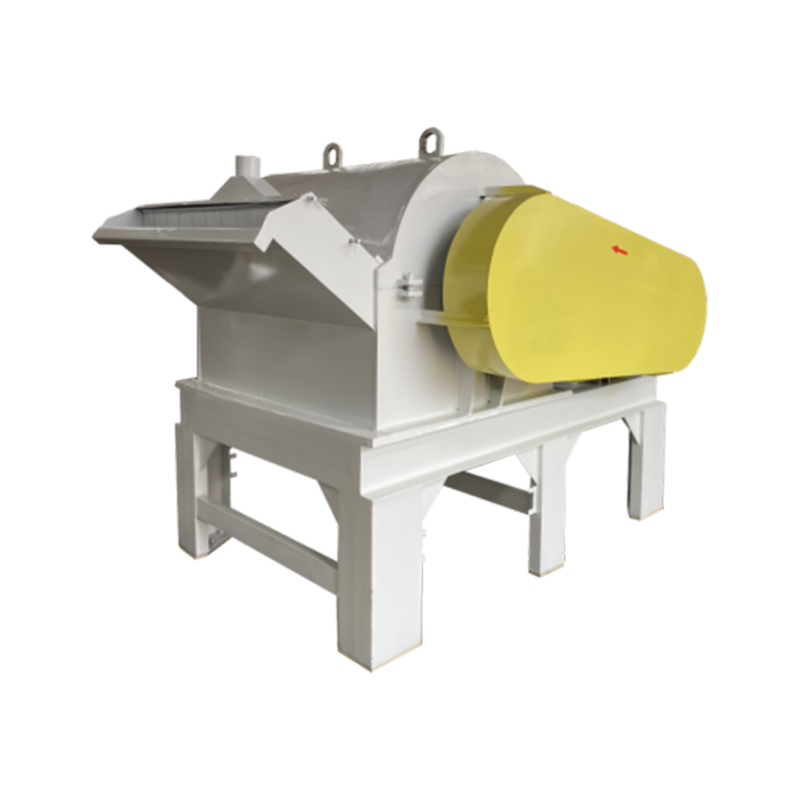
Hammer-impact swing-knife crushing and pulverizing production line
3. Product Advantages Over Conventional Crushing and Pulverizing Systems
The principal advantage of this production line is the integration of multiple processing stages into one coordinated system. However, its value is not limited to the number of machines included. The design addresses several recurring problems associated with conventional crushing and grinding arrangements.
3.1 Better Handling of Large and Irregular Waste
Many ordinary knife crushers are optimized for relatively manageable pieces. Long pipes, bulky profiles, thick sheets, and flexible sacks can create feeding difficulties. They may rotate without being cut, bridge at the inlet, or wrap around the rotor. The hammer-impact swing-knife configuration uses impact and shear together, allowing it to break difficult materials more readily.
The wider customizable feed inlet also reduces the amount of preliminary manual cutting. This can be especially important for recycling plants receiving post-industrial scrap in irregular shapes. Less manual preparation means lower labor requirements and more consistent feeding.
3.2 Reduced Entanglement and Jamming
Flexible PE, PP, EVA, woven bags, and similar materials can be challenging because they deform instead of breaking cleanly. A purely cutting-based rotor may encourage long strips to wrap around the shaft. The impact action of the hammer-blade rotor helps disrupt the material structure and reduce entanglement.
No crusher is completely immune to foreign objects, overfeeding, or unsuitable material. Nevertheless, the combined force pattern offers an advantage over simple knife-type structures when processing high-impact or flexible plastics. Stable feeding is one of the most important factors in achieving the advertised capacity range.
3.3 More Uniform Fine Powder
Fine powder quality depends on more than grinding speed. Disc accuracy, dynamic balance, gap adjustment, material flow, cooling, and screening all influence the result. The use of precision-machined grinding discs and dynamic balancing provides a stronger foundation for producing uniform powder than an inaccurately assembled or poorly balanced grinding chamber.
Uniform particle size improves dispersion in downstream production. In rotational molding, consistent powder can support more predictable melting and surface formation. In SPC flooring, uniform recycled powder can contribute to more stable mixing and core-layer processing. In extrusion and compounding, controlled powder size can improve feeding and blending behavior.
3.4 Improved Heat Management
Plastic grinding generates heat through friction and impact. PVC, PE, and other heat-sensitive materials may soften, adhere to the grinding disc, discolor, or degrade if the grinding chamber becomes too hot. Excessive heat can also reduce powder flowability and increase cleaning requirements.
The grinding section uses a reinforced dual cooling system, multi-point temperature sensors, and PLC-based control. The operating temperature is described as being controlled approximately between 50 and 80 degrees Celsius, depending on the material and process conditions. This temperature range is a control target rather than a universal result for every application.
Cooling allows the operator to balance production capacity against powder quality. If the feed rate is too high or the material is too warm, the control system can support adjustments to feeding, airflow, or cooling. By continuously monitoring temperature at multiple points, the system provides more information than a single manual temperature check.
3.5 Cleaner and Safer Production
Open transfer points and poorly sealed grinding systems can release plastic dust throughout a workshop. The integrated negative-pressure conveying and pulse dust collection arrangement is designed to reduce this problem. Enclosed material movement also minimizes direct operator contact with the processed powder.
Cleaner production benefits both regulatory compliance and daily operations. A workshop with less airborne dust is easier to maintain, easier to inspect, and more comfortable for employees. Proper dust collection also reduces the accumulation of combustible or irritating particles on nearby equipment.
3.6 Lower Labor and Space Requirements
Separate crushing and pulverizing systems often require additional conveyors, intermediate storage, manual transfer, and independent operators. An integrated line reduces these requirements through continuous conveying and centralized control.
The modular layout also allows the equipment to be arranged according to the customer’s factory dimensions. A compact design can reduce the amount of floor space required for intermediate material storage. The exact footprint depends on the selected crusher, pulverizer, dust collector, screening equipment, and conveying route.
3.7 Flexible Application Range
The same basic production concept can serve several material streams. Rigid PVC pipe scrap may require a different feeding rate and cooling setting from PE rotational-molding waste. PET, ABS, and EVA may require different grinding gaps or throughput adjustments. The variable-frequency feeding system and PLC control make it easier to adapt operating conditions.
This flexibility gives recycling companies more opportunities to process multiple products using one line. It can also support future changes in the waste stream without requiring a completely new machine arrangement.
4. Technical Configuration and Operating Specifications
The following table summarizes the listed specifications for the hammer-impact coarse-crushing section. These figures should be used as a reference for the specified equipment configuration. Final performance should be confirmed through material testing and a technical proposal based on the customer’s feedstock.
| Item | Specification | Remarks |
|---|---|---|
| Machine type | 1000 | Listed model type |
| Knife quantity | 36 rotary knives | Hammer-impact swing-knife rotor |
| Capacity | 1–2.5 tons per hour | Depends on material and operating conditions |
| Nominal mesh or sizing specification | 16 millimeters | Intermediate crushing reference |
| Drive motor options | 55, 75, 90, or 110 kilowatts | Selected according to application |
| Speed control | Inverter | Supports adjustable operating speed |
| Bearing specification | Imported NSK bearings | Applied to the listed belt-pulley standard |
| Knife material | SKD-11 | Wear-resistant tool steel |
| Host speed | 860 revolutions per minute | Listed reference speed |
| Feeding size | 1,350 millimeters | Listed feeding dimension |
| Electrical cabinet starting method | Star-delta or soft start | Selected according to the electrical configuration |
| Fine pulverizer models | 500, 600, and 800 | Disc mill model options |
| Typical final powder range | Approximately 20–80 mesh or finer | Depends on material and adjustment |
| Grinding disc material | DC53 high-grade mold steel | Designed for wear resistance and precision |
| Temperature-control range | Approximately 50–80 degrees Celsius | Process target subject to material conditions |
Capacity should not be interpreted as a guaranteed output for every plastic. Thin film, rigid PVC, wet feedstock, contaminated waste, highly elastic materials, and heat-sensitive polymers can behave differently. A proper technical evaluation considers bulk density, particle shape, moisture, impurity level, desired final mesh, and operating temperature.
5. Manufacturing Quality and Engineering Strength
The performance of a recycling line depends heavily on manufacturing accuracy. A crusher may have an appropriate motor rating, but poor rotor alignment, inaccurate knife installation, weak welding, or insufficient balancing can cause vibration, rapid wear, and inconsistent output. For this reason, the manufacturing process behind the equipment is as important as the equipment concept itself.
5.1 Long-Term Specialization
Changzhou Mao Yue Intelligent Equipment Co., Ltd. has approximately 30 years of experience in plastic crushing and pulverizing equipment. Its specialization in plastic size reduction allows the company to focus on the practical problems encountered in rotational molding, PVC processing, recycling, masterbatch production, polymer handling, and powder coating.
Long-term specialization provides an important advantage over manufacturers that treat pulverizers as a general-purpose product. Plastic materials differ significantly in thermal behavior, toughness, elasticity, and grinding response. Experience across multiple applications helps the engineering team select suitable rotor structures, grinding discs, cooling systems, screens, conveying arrangements, and electrical controls.
5.2 Large-Scale Workshop Organization
The company operates six processing workshops, each averaging approximately 1,400 square meters. This manufacturing capacity supports the production of large equipment assemblies and helps separate different stages of fabrication, machining, welding, assembly, and testing.
A structured workshop arrangement can improve production flow and reduce the risk of work being performed in unsuitable areas. Large components can be handled more safely, while assembly teams have adequate room for alignment, inspection, and trial operation.
5.3 High-Precision Machining
The production facility uses Taiwan-imported high-precision grinding machines built to German standards. Precision machining is especially important for pulverizer discs, knife seats, shafts, and other rotating or wear-sensitive components.
Grinding disc tooth profiles must be accurately formed so that the working clearance remains stable. Even small dimensional differences can affect powder uniformity, energy consumption, vibration, and local heat generation. High-precision machining helps the manufacturer produce replaceable components with consistent dimensions.
5.4 Dynamic Balancing
High-speed rotating parts must be balanced carefully. The company uses German dynamic balancing equipment to calibrate rotating components. Proper balancing reduces vibration transmitted to the bearings, housing, foundation, and electrical components.
Lower vibration supports a more comfortable working environment and can reduce fatigue in mechanical parts. It also helps maintain a stable grinding gap, which contributes to uniform powder production. Dynamic balancing is therefore a performance requirement rather than merely a finishing step.
5.5 Welding and Structural Fabrication
Reliable welding affects the strength, sealing performance, and long-term stability of the production line. The company uses Japanese welding systems in its manufacturing process. Accurate welding helps produce robust frames, housings, hoppers, platforms, ducts, and dust-collection structures.
Strong and properly sealed housings are particularly important in a negative-pressure system. Gaps or deformation can reduce airflow efficiency and allow dust to escape. Consistent fabrication helps maintain the integrity of the complete line.
5.6 European-Quality Manufacturing Approach
The company states that it manufactures components according to European quality standards and has obtained CE mechanical certification and ISO 9001 quality management system certification. These certifications support a structured approach to design, production, documentation, and quality control.
Certification does not eliminate the need for correct installation and safe operation. However, it provides customers with evidence that the equipment is produced within a documented quality-management framework. It also supports international procurement and helps customers organize their own equipment compliance processes.
6. Intelligent Control and Automation
The line uses PLC centralized control to coordinate the major process units. A centralized control architecture can manage feeding, crusher operation, pulverizer operation, temperature monitoring, conveying, screening, and dust collection in a logical sequence.
6.1 Variable-Frequency Feeding
Variable-frequency feeding allows the material flow to be adjusted according to the load on the crusher and pulverizer. When the grinding chamber approaches a high load or temperature condition, the feed rate can be reduced. When operating conditions are stable, the feed rate can be increased within the limits of the selected equipment.
Controlled feeding is more effective than relying on an operator to add material at an irregular rate. It helps prevent sudden overloads, reduces surging, and supports more consistent powder quality.
6.2 Temperature Monitoring
Multi-point temperature sensors provide information from different parts of the grinding process. Plastic does not always heat evenly. A single sensor may fail to identify a local hot spot near the disc, outlet, or material accumulation zone. Multi-point monitoring gives the control system a more complete view of thermal conditions.
When combined with cooling equipment and PLC control, temperature monitoring helps protect heat-sensitive materials. It can reduce the risk of PVC yellowing, adhesion, thermal degradation, and loss of flowability.
6.3 One-Button Start and Stop
One-button start and stop functions simplify operation by following a programmed sequence. Downstream equipment may need to start before upstream feeding begins, while shutdown may require the line to clear material before the main machines stop. Automated sequencing helps prevent material accumulation and reduces operator error.
Emergency-stop circuits, protective interlocks, overload protection, and appropriate guarding remain essential. Automatic control should support, not replace, safe working procedures and regular inspection.
7. Material Applications
7.1 PVC Pipes, Profiles, Sheets, and Foam Boards
PVC waste is often generated in the manufacture and installation of pipes, window and door profiles, flooring sheets, and foam boards. These materials can be bulky and may contain long sections or large offcuts. The front-end hammer-impact crusher reduces their dimensions, while the disc pulverizer produces powder that can be reused in PVC processing or SPC flooring core layers.
Because PVC is sensitive to excessive heat, temperature control is especially important. The reinforced cooling system and sensor-based control help reduce the risk of overheating, sticking, yellowing, and degradation. Operators should still separate incompatible materials and avoid feeding contaminated waste that could damage the machine or compromise powder quality.
7.2 PE and PP Rotational-Molding Waste
Rotational molding produces products such as tanks, bins, toys, playground components, pallets, and other hollow or molded structures. Production rejects and end-of-life products can be bulky, tough, and difficult to feed into a small crusher.
The integrated line can process PE and PP waste into approximately 30 to 80 mesh powder when correctly configured. Uniform powder with good flowability is suitable for new rotational-molding products, modified materials, and other plastic manufacturing applications. The ability to return processed powder to a similar product stream supports a practical closed-loop recycling model.
7.3 Woven Bags, Flexible Materials, and Packaging Waste
Woven bags and other flexible plastics can create entanglement problems in standard knife crushers. The impact and shear action of the hammer-blade rotor helps break these materials into manageable pieces before fine grinding.
Flexible materials may require careful feeding and airflow adjustment. If the material is too light, excessive conveying air can affect separation efficiency. If it is contaminated with moisture or dirt, additional preparation may be necessary. A material trial is recommended before selecting final operating parameters.
7.4 PET, ABS, and EVA
The line is also suitable for selected engineering and specialty plastics, including PET, ABS, and EVA. Potential feedstocks include bottle flakes, appliance housings, automotive or electrical components, films, foamed materials, and production scrap.
These materials may have different hardness and thermal characteristics. PET can be relatively tough, ABS may contain reinforcing or blended components, and EVA may be softer and more elastic. The crusher and pulverizer settings should therefore be selected according to the exact grade and application.
Processed powder can be directed toward extrusion, injection molding, compounding, modification, or other value-added uses. Sorting and contamination control are essential if the powder is intended for a high-quality recycled product.
7.5 Centralized Industrial Waste Treatment
Recycling stations, environmental service companies, and industrial plastic processors can use the line as a centralized treatment system. Such facilities often receive multiple forms of plastic waste and need equipment that can operate continuously at a commercial capacity.
The line’s modular arrangement allows the customer to select suitable front-end feeding, crushing, grinding, screening, conveying, and dust-control components. This makes it possible to build a solution around actual waste volumes rather than purchasing a generic machine with unsuitable capacity.
8. Powder Quality and Downstream Value
The commercial value of recycled powder depends on more than the amount of waste processed. Particle size distribution, cleanliness, color, thermal history, bulk density, flowability, and polymer consistency all influence the final application.
A well-controlled pulverizing process can improve the uniformity of the powder and make it easier to blend with virgin resin, additives, fillers, or other recycled material. Uniform powder can also improve dosing accuracy in downstream equipment.
For rotational molding, powder flowability and particle distribution affect feeding, melting, coating of the mold surface, and final product appearance. For SPC flooring, consistent powder can support stable formulation and production of the core layer. For extrusion and compounding, controlled size can assist blending and reduce feeding variation.
Recycling companies should define the required final specification before commissioning the line. Important questions include the target mesh range, acceptable oversize percentage, allowable contamination, color requirements, moisture limits, and whether the powder will be used in a closed-loop application.
9. Installation, Operation, and Maintenance Considerations
Correct installation is necessary to achieve the expected performance. The foundation should support the equipment weight and dynamic loads. Conveying ducts should be routed with suitable bends and access points. Electrical power must match the motor configuration, and the dust collector should be connected according to the required airflow and filtration arrangement.
Operators should inspect knives, grinding discs, screens, bearings, belts, seals, and dust-collection bags at scheduled intervals. Wear parts should be replaced or adjusted before they cause secondary damage. Dull knives can increase energy consumption and heat generation, while worn grinding discs can reduce powder uniformity.
Material should be fed consistently rather than dumped in large surges. Foreign metal should be removed before it enters the crusher. Moisture should be controlled because wet material can reduce conveying efficiency, affect screening, and cause powder to adhere to internal surfaces.
The dust collector requires regular inspection of filter bags, pulse valves, compressed-air quality, pressure difference, and discharge arrangements. A dust collector that is not maintained can lose airflow and reduce the effectiveness of the entire line.
Temperature alarms should not be ignored. If the grinding chamber becomes too hot, the operator should check feed rate, material composition, cooling water or air supply, disc clearance, and ventilation. Continuing to operate under abnormal thermal conditions can reduce product quality and shorten component life.
10. Economic and Environmental Benefits
The line can reduce labor costs by automating material transfer and coordinating multiple process stages. It can also reduce floor-space requirements by eliminating some intermediate storage and manual handling points. Energy consumption should be evaluated across the complete system rather than by looking only at the motor rating of one machine.
Efficient processing improves raw material utilization because fine powder is collected instead of being lost as airborne dust. The ability to reuse production scrap can reduce purchases of virgin resin and lower disposal expenses. For manufacturers generating large volumes of waste, converting scrap into usable powder can create a direct internal material stream.
Environmental performance comes from several design elements working together. Enclosed conveying limits emissions at transfer points. Negative pressure helps direct dust toward the collection system. Pulse filtration captures fine particles. Controlled operation reduces material loss and supports compliance with applicable environmental requirements.
Payback depends on many factors, including waste volume, product value, labor costs, electricity rates, final powder price, maintenance requirements, and the percentage of material successfully recovered. A technical and economic assessment should be completed before investment.
11. Why Manufacturer Experience Matters
Purchasing a plastic pulverizing line is not simply a matter of selecting a motor size. The equipment must be matched to the customer’s materials, output requirements, factory conditions, environmental obligations, and maintenance capabilities. A manufacturer with long-term experience can contribute to this process through material testing, process design, component selection, and after-sales support.
The company’s product range is centered on disc pulverizers and plastic size-reduction equipment. Its machines are used in rotational molding, masterbatch, polymers, PVC, PE, recycling, and powder coating. This application background enables the manufacturer to understand both the mechanical and production requirements of fine plastic powder.
The company has established long-term partnerships with more than 5,000 enterprises in domestic and international markets. Such a customer base indicates broad exposure to different production conditions, although each new project still requires individual assessment.
Customization is another important strength. The feed inlet, motor power, cooling method, conveying arrangement, screening equipment, and dust-collection capacity can be selected according to the customer’s material and desired output. The coarse-crushing section can use air cooling or water-mist assistance when additional thermal control is needed.
12. Recommended Selection Procedure
A successful project should begin with a detailed description of the raw material. The customer should provide information about polymer type, size, thickness, bulk density, moisture, contamination, and whether different materials are mixed.
The second step is to define the final product. The required mesh range, powder flowability, acceptable temperature, color, contamination level, and downstream processing method all affect the equipment configuration.
The third step is capacity planning. The stated coarse-crushing configuration has a reference capacity of 1 to 2.5 tons per hour, but actual fine-powder output can differ. The complete line should be balanced so that the crusher, pulverizer, conveyor, screen, and dust collector can operate together without creating a bottleneck.
The fourth step is process testing. A representative sample should be processed to verify throughput, temperature behavior, particle-size distribution, power consumption, and powder quality. Testing is particularly important when the material is a mixed stream or a heat-sensitive polymer.
The final step is installation and operator training. Staff should understand startup and shutdown procedures, alarm handling, cleaning, wear-part replacement, dust-collector maintenance, and safe access to the equipment.
13. Frequently Asked Questions
13.1 What types of plastic can the line process?
The line is designed for PVC, PE, PP, PET, ABS, EVA, and other medium-hardness or high-impact plastics. The exact configuration should be confirmed according to the material grade, size, moisture, contamination, and required final powder.
13.2 Can it process large pipes and profiles?
Yes. The hammer-impact swing-knife crusher is designed to handle large pipes, profiles, sheets, foam boards, pallets, woven bags, and other bulky waste. The feed inlet can be customized, and the material may require preparation if it exceeds the selected feeding dimensions.
13.3 What final powder size can be achieved?
The product description indicates an approximate final range of 20 to 80 mesh or finer. The actual result depends on the plastic type, grinding-disc configuration, feed rate, temperature, screen, and operating adjustment.
13.4 Is the line suitable for rotational-molding powder?
Yes. PE and PP rotational-molding waste can be processed into fine, uniform powder suitable for reuse in rotational molding or modified-material production. A material test should verify the required particle distribution and flowability.
13.5 How does the system control grinding temperature?
The grinding section uses a reinforced dual cooling system, multi-point temperature sensors, and PLC intelligent control. The stated operating target is approximately 50 to 80 degrees Celsius, but the correct temperature depends on the material and production conditions.
13.6 How does the line reduce dust emissions?
Material is moved through enclosed negative-pressure conveying, and the line includes cyclone separation and pulse bag dust collection. The stated dust-capture efficiency is greater than 99.9 percent under suitable operating and maintenance conditions.
13.7 What prevents the crusher from jamming?
The hammer-impact swing-knife structure combines impact and shearing forces, helping break flexible and irregular materials before they can wrap around the rotor. Correct feeding, foreign-object removal, and proper maintenance remain necessary for reliable operation.
13.8 Can the line be customized?
Yes. Customization may include the feed inlet, motor power, pulverizer model, cooling method, conveying route, screening system, dust collector, electrical controls, and layout. The final design should be based on material testing and the required output.
13.9 What maintenance is required?
Routine maintenance includes inspection of knives, grinding discs, bearings, belts, screens, seals, filter bags, pulse valves, and electrical components. Operators should also monitor vibration, temperature, airflow, and powder quality.
13.10 What certifications does the manufacturer have?
The manufacturer states that it has CE mechanical certification and ISO 9001 quality management system certification. Customers should review the documentation applicable to their specific machine configuration and local installation requirements.
13.11 How should the capacity be evaluated?
Capacity should be evaluated using the actual feedstock rather than a general material label. Thickness, bulk density, moisture, contamination, final mesh, and temperature limits can significantly affect production. A representative sample test is recommended.
13.12 Is the line suitable for a centralized recycling plant?
Yes. Its modular structure, automated control, dust collection, and ability to process several plastic categories make it suitable for recycling stations, environmental companies, plastic manufacturers, and centralized industrial waste treatment centers.
14. Conclusion
The hammer-impact swing-knife crushing and pulverizing production line provides a complete approach to plastic waste size reduction. Its front-end crusher is designed for large, irregular, flexible, and high-impact plastic waste, while the precision disc pulverizer produces controlled fine powder for demanding downstream applications.
The integration of impact crushing, fine grinding, negative-pressure conveying, cyclone separation, vibrating screening, temperature control, and pulse dust collection gives the line advantages over disconnected conventional systems. It reduces manual handling, improves process continuity, supports more uniform powder, limits dust leakage, and adapts to multiple plastic recycling applications.
Its value is strengthened by the manufacturer’s long-term specialization, six workshop production structure, high-precision machining equipment, dynamic balancing capability, advanced welding systems, and documented quality certifications. These manufacturing strengths help create equipment that is not only powerful, but also stable, maintainable, and suitable for continuous industrial use.
For companies processing PVC pipes, profiles, SPC flooring scrap, PE and PP rotational-molding waste, woven bags, engineering plastics, foam materials, or mixed industrial plastic waste, the line offers a practical route from bulky discarded material to reusable fine powder. The best results come from matching the machine configuration to the actual material, conducting representative testing, controlling temperature and dust, and maintaining the equipment according to a structured service plan.
References
1. Manufacturer-provided product specifications for the hammer-impact swing-knife crushing and pulverizing production line.
2. Manufacturer-provided technical information for plastic disc pulverizers, grinding discs, cooling systems, screening systems, and dust-collection equipment.
3. Manufacturer-provided company information concerning production workshops, machining equipment, dynamic balancing, welding systems, certifications, and application experience.
4. General principles of plastic recycling, mechanical size reduction, particle-size control, pneumatic conveying, and industrial dust collection.
5. General engineering practices for plastic-processing equipment selection, temperature management, preventive maintenance, and workplace dust control.