

 English
 русский
 Español
 عربى
 中文简体
 中文简体
Content
- 1 Introduction
- 2 1. The Role of Blades in a PE Pulverizing System
- 3 2. Alloy Steel Construction and Material Advantages
- 4 3. Hardness, Toughness, and Wear Resistance
- 5 4. Precision Heat Treatment
- 6 5. Manufacturing Process and Quality Control
- 7 6. Performance Advantages Compared with Ordinary Cutting Discs
- 8 7. Service Life and Maintenance Economics
- 9 8. Precision Clearance and Powder Quality
- 10 9. Thermal Management During Grinding
- 11 10. Applications in Plastic Recycling
- 12 11. Applications in Powder Coatings
- 13 12. Modified Plastics and Masterbatch Production
- 14 13. Rotational Molding and Chemical Processing
- 15 14. Research, Development, and Small-Batch Processing
- 16 15. Compatibility and Customization
- 17 16. Installation and Commissioning Recommendations
- 18 17. Maintenance and Inspection
- 19 18. Company Manufacturing Strengths
- 20 19. Sustainability and Total Operating Value
- 21 20. How to Select the Correct Blade
- 22 21. Frequently Asked Questions
- 22.1 Q1: What makes alloy steel blades different from ordinary pulverizer blades?
- 22.2 Q2: What hardness can these PE pulverizer blades achieve?
- 22.3 Q3: Can the blades process glass-fiber-reinforced plastic?
- 22.4 Q4: How long can one blade set operate?
- 22.5 Q5: What powder fineness can be achieved?
- 22.6 Q6: Are the blades compatible with other brands of pulverizers?
- 22.7 Q7: Can the blade dimensions and tooth profile be customized?
- 22.8 Q8: Why is thermal control important when grinding PE?
- 22.9 Q9: What should be checked before installing replacement blades?
- 22.10 Q10: What certifications does the manufacturer hold?
- 22.11 Q11: Can these blades be used in recycling and powder-coating lines?
- 22.12 Q12: How can blade life be maximized?
- 23 Conclusion
- 24 References
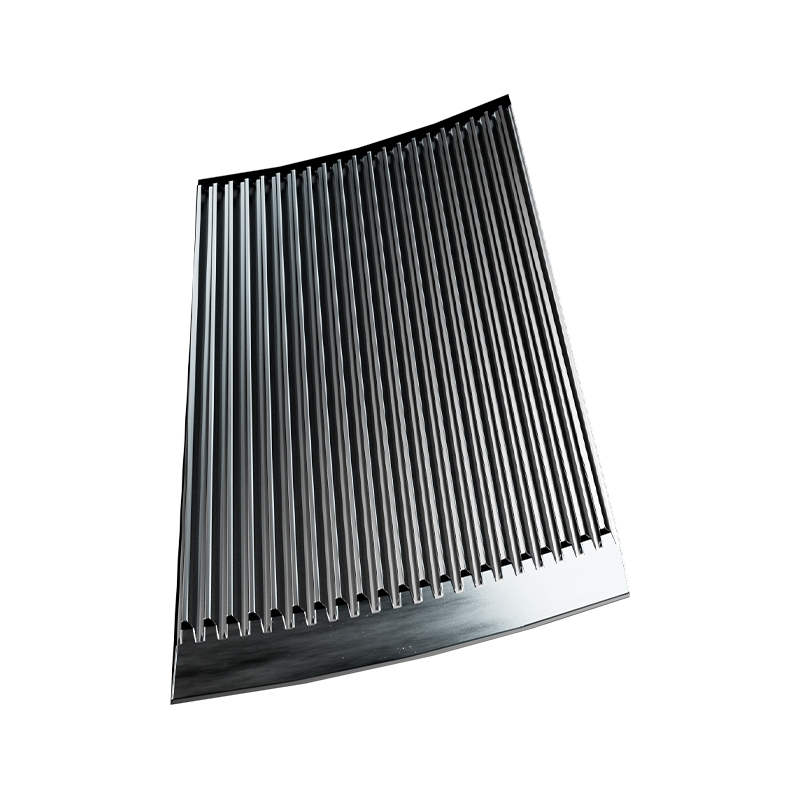
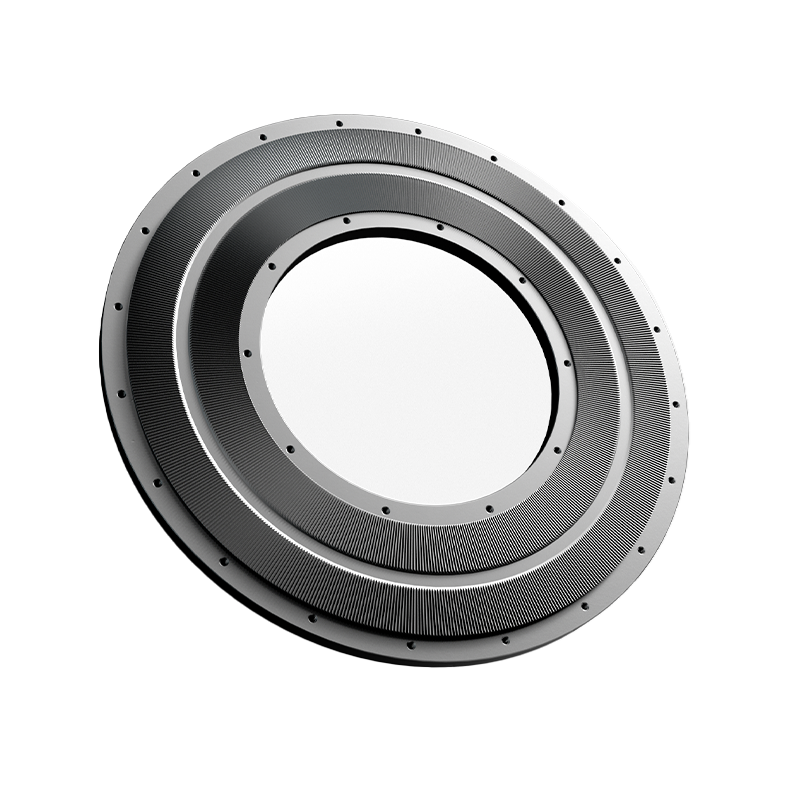
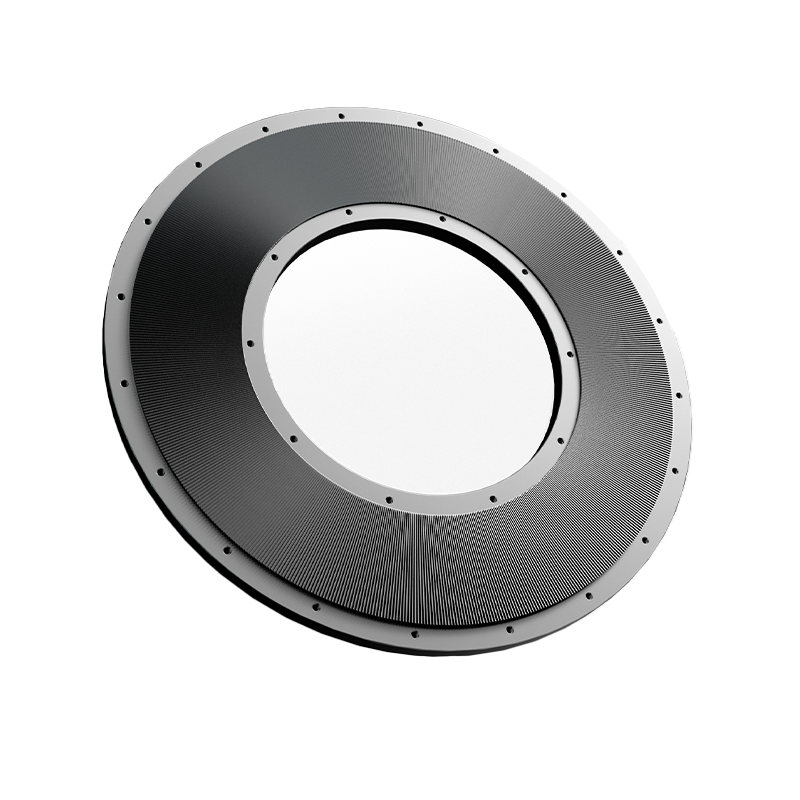
- 25 Product: PE Pulverizer alloy steel blades
Introduction
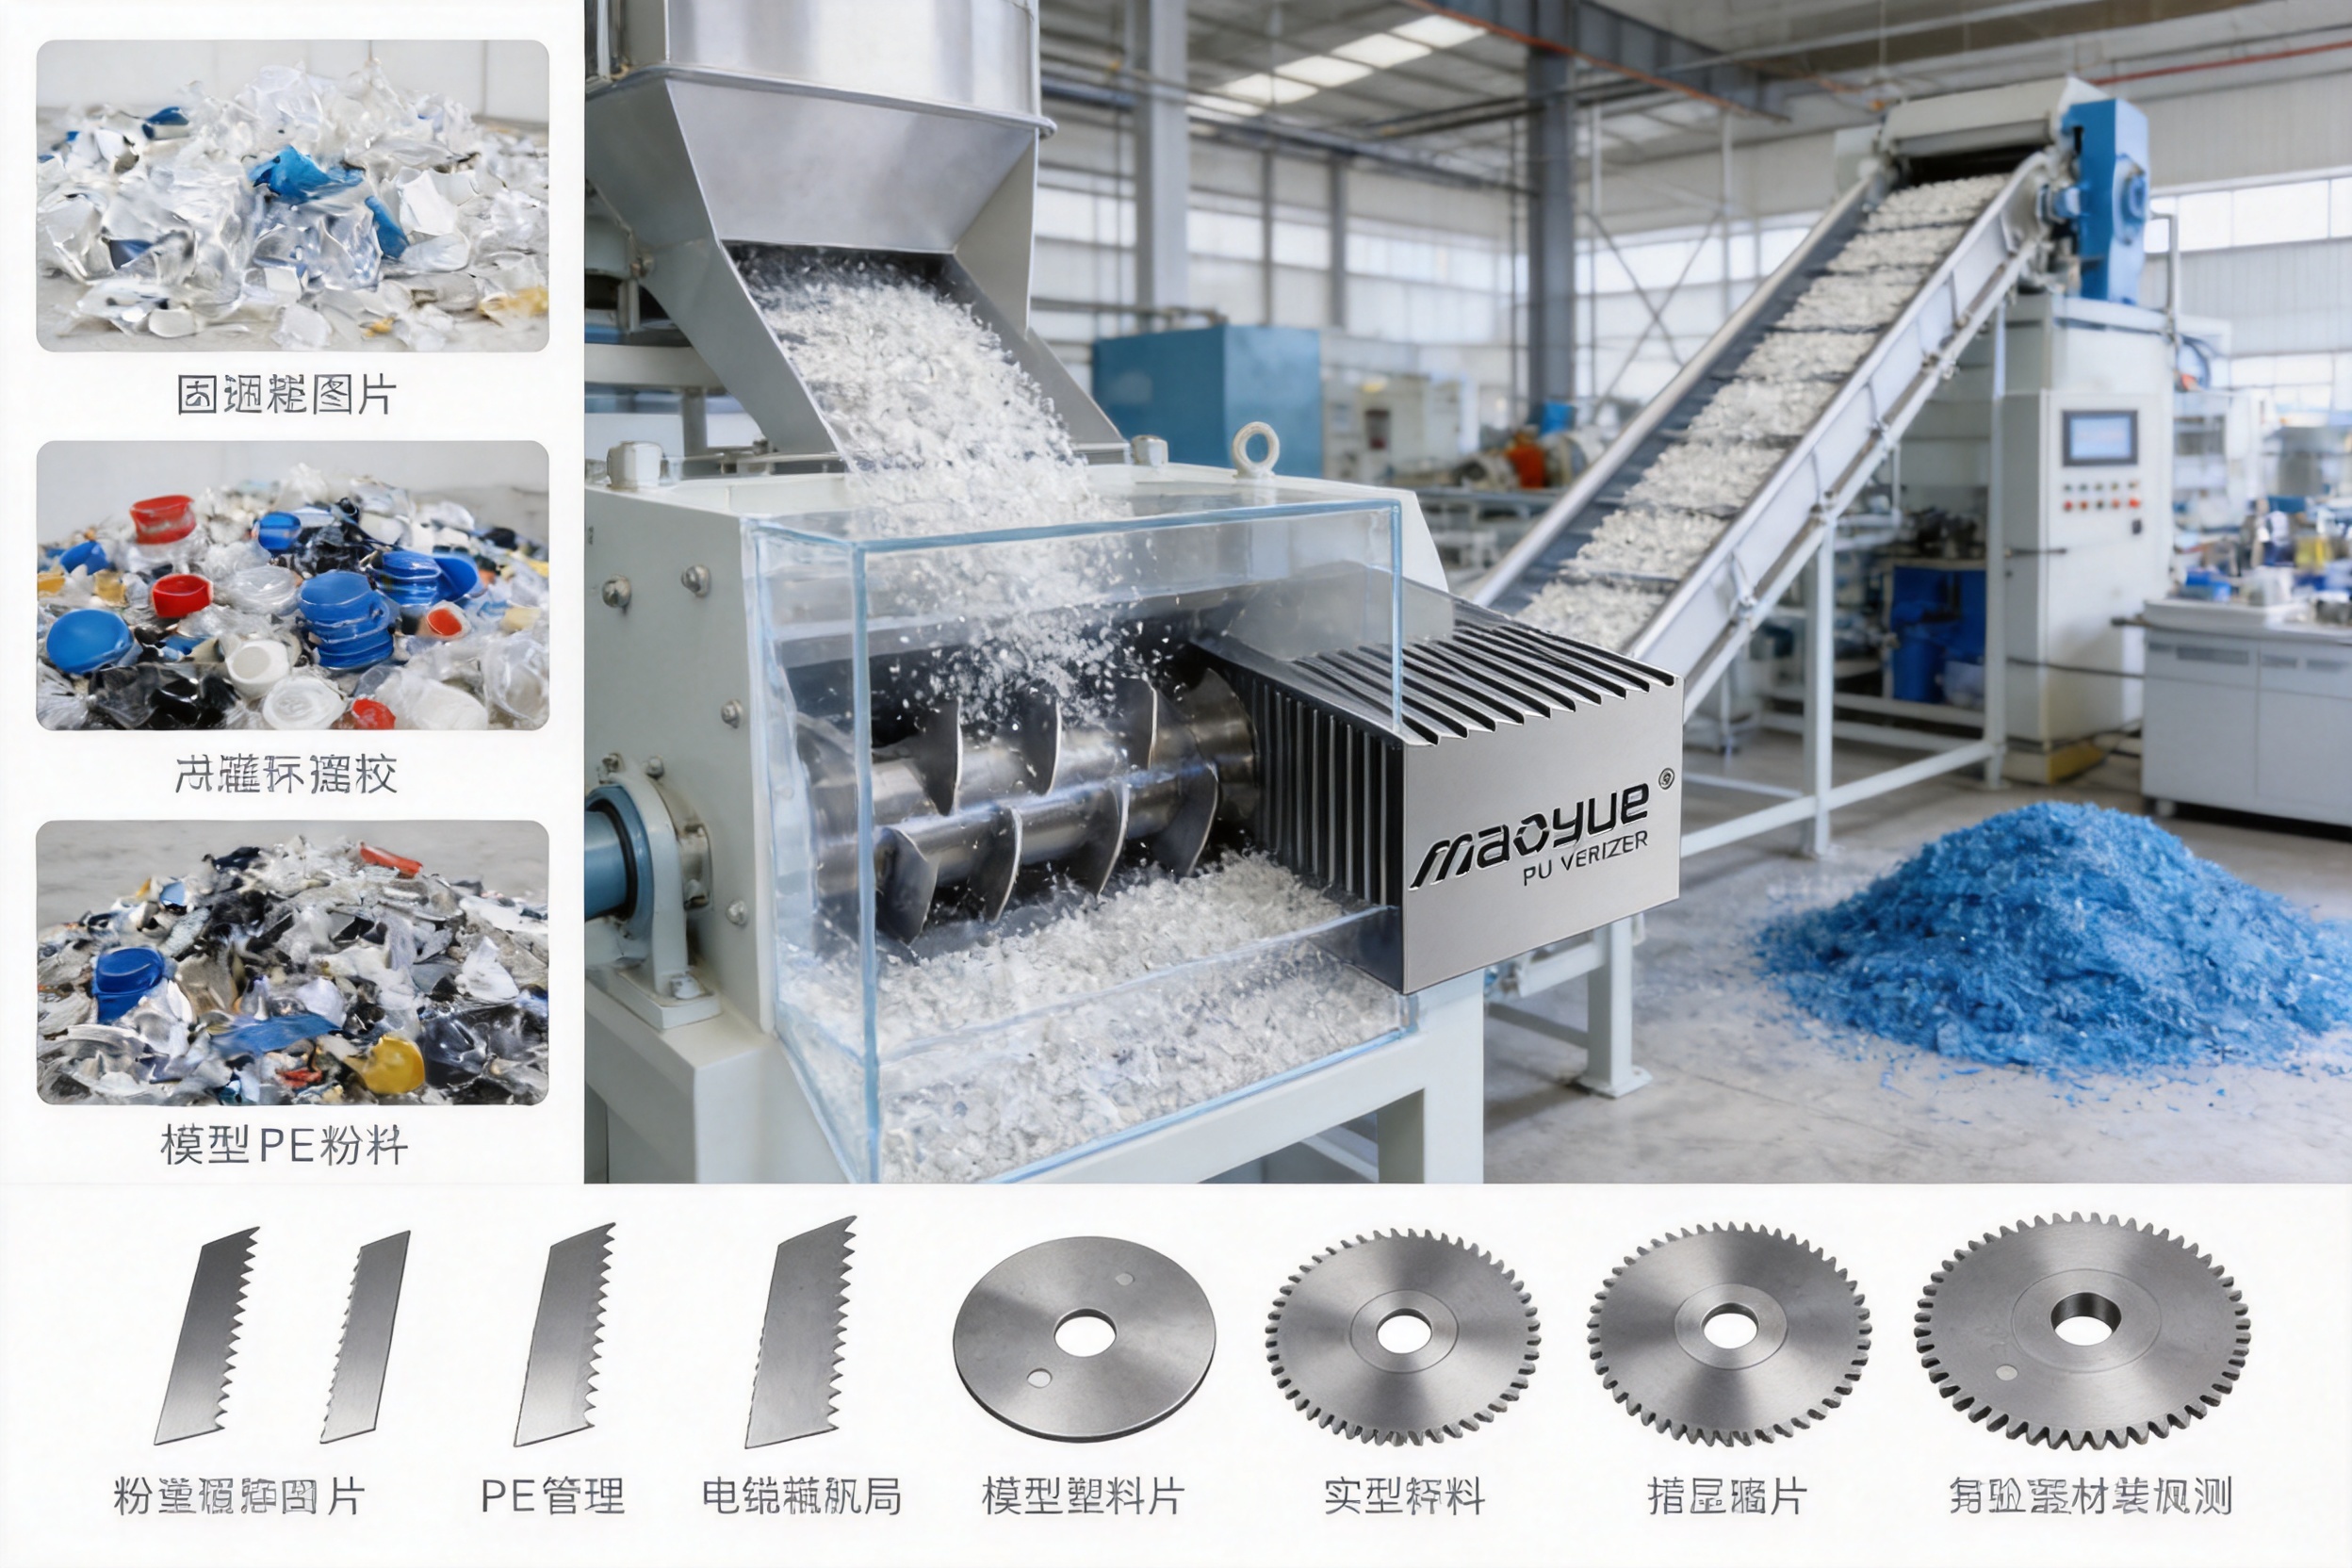
PE pulverizer alloy steel blades are essential wear components in plastic grinding systems designed to convert polyethylene waste, production scrap, and semi-finished materials into controlled powder. Although a pulverizer may contain a motor, grinding disc, classifier, cooling system, and feeding mechanism, the blades remain one of the most important components affecting grinding efficiency, powder quality, energy consumption, and maintenance frequency.
For processors working with polyethylene film, pipes, bottle caps, cable sheathing, packaging bands, rotational molding materials, or recycled production waste, ordinary cutting discs may not provide adequate service life. Polyethylene can be tough, elastic, and sensitive to heat. When reinforced plastics or other high-toughness materials are introduced into the grinding chamber, the blade edge may wear quickly, become dull, or generate excessive frictional heat. These problems can lead to unstable particle size, increased downtime, higher replacement costs, and inconsistent downstream processing.
High-performance PE pulverizer alloy steel blades are developed to address these operating challenges. Manufactured from high-density wear-resistant alloy steel and processed through controlled heat treatment, these blades are designed to combine high hardness with impact resistance. A typical hardness level of HRC 60–65 or higher provides substantially greater wear resistance than ordinary cutting discs manufactured around HRC 45. Depending on the operating conditions, material characteristics, machine settings, and maintenance practices, the service life can be extended by two to three times or more compared with conventional blades.
This article examines the material structure, manufacturing process, performance advantages, installation considerations, applications, and maintenance requirements of PE pulverizer alloy steel blades. It also explains how a specialized manufacturer such as Changzhou Mao Yue Intelligent Equipment Co., Ltd. supports product consistency through precision machining, dynamic balancing, advanced welding, quality management, and customized engineering.
1. The Role of Blades in a PE Pulverizing System
A plastic pulverizer reduces material through a combination of high-speed rotation, cutting, shearing, impact, and friction. The rotating disc and fixed disc work together to create a controlled grinding gap. Material enters the grinding chamber, is accelerated by centrifugal force, and passes through the active cutting and grinding zone repeatedly until it reaches the required particle size.
In this process, the blade edge is exposed to continuous mechanical stress. Every blade must withstand repeated contact with plastic particles, intermittent impact from irregular feedstock, friction generated by high-speed movement, and thermal loads caused by the conversion of mechanical energy into heat. If the cutting edge wears unevenly, the grinding gap changes. If the blade becomes too hot, polyethylene may soften, smear, or adhere to the grinding disc. If the blade is too brittle, impact can cause chipping or premature failure.
Therefore, the ideal blade is not simply the hardest possible component. It must achieve a carefully balanced combination of hardness, toughness, dimensional accuracy, wear resistance, thermal stability, and compatibility with the pulverizer disc. The alloy steel formulation and heat-treatment process are particularly important because they determine the blade’s ability to retain a sharp edge while resisting cracking and deformation.
Blade geometry is also significant. The tooth profile, cutting angle, number of teeth, surface finish, and clearance between rotating and stationary components all influence the grinding result. A suitable blade design helps the machine generate efficient shearing and frictional grinding instead of relying excessively on impact. This reduces unnecessary energy loss and supports more uniform powder production.
2. Alloy Steel Construction and Material Advantages
PE pulverizer alloy steel blades are produced from high-density wear-resistant steel, such as chromium-molybdenum-vanadium alloy or a comparable high-hardness material. Each alloying element contributes to the performance of the blade in a different way.
2.1 Chromium
Chromium improves hardenability and contributes to wear resistance. It helps the steel respond consistently during heat treatment and supports the formation of a strong hardened structure. Chromium-containing steel is often selected for tools that must maintain dimensional stability during repeated mechanical loading.
2.2 Molybdenum
Molybdenum enhances toughness, hardenability, and resistance to softening at elevated temperatures. This is particularly valuable in plastic pulverizing applications because the grinding zone can heat up during continuous operation. A molybdenum-containing alloy is better able to retain its mechanical properties when exposed to frictional heat.
2.3 Vanadium
Vanadium can form fine, hard carbide particles within the steel matrix. These carbides help resist abrasive wear and support edge retention. When properly controlled during melting, forging, and heat treatment, vanadium contributes to a fine-grained structure and improved service reliability.
The final performance does not depend on the alloy formula alone. Steel cleanliness, forging quality, grain structure, heat-treatment accuracy, machining precision, and final inspection all influence the finished blade. A high-quality material that is improperly heat-treated may still develop distortion, uneven hardness, or brittle edges. For this reason, the manufacturing process must be treated as an integrated system rather than a single material-selection decision.
3. Hardness, Toughness, and Wear Resistance
The specified hardness of PE pulverizer alloy steel blades is commonly HRC 60–65 or higher. This is considerably higher than the approximate HRC 45 hardness associated with ordinary cutting discs. Higher hardness generally improves resistance to abrasive wear and allows the edge to remain sharp for a longer period.
However, hardness must be balanced with toughness. A blade that is excessively hard but insufficiently tough may chip when it encounters a hard contaminant, a thick lump, or an uneven feed condition. The objective of multiple precision heat treatments is to create a blade structure that combines a hard working surface with sufficient internal toughness.
In practical operation, this balance can produce several advantages:
1. Longer edge retention during continuous grinding.
2. Reduced wear when processing tough or reinforced polyethylene materials.
3. Lower risk of rapid edge rounding.
4. More stable particle-size distribution over longer operating periods.
5. Reduced frequency of blade replacement.
6. Lower labor requirements for disassembly, inspection, and installation.
7. Less production loss caused by unexpected shutdowns.
Under suitable operating conditions, the wear rate may be reduced by more than 70 percent compared with ordinary cutting discs. Actual results depend on the material being processed, contamination levels, feed rate, rotor speed, grinding clearance, cooling performance, and operator practices. Nevertheless, the combination of high hardness and controlled toughness provides a strong foundation for long-term use.
4. Precision Heat Treatment
Heat treatment is one of the most important stages in blade manufacturing. It transforms the steel’s internal structure and establishes the final relationship between hardness, toughness, dimensional stability, and wear resistance.
A typical precision heat-treatment sequence may include preheating, austenitizing, controlled quenching, tempering, and, where required, multiple tempering cycles. Cryogenic treatment or stress-relief procedures may also be applied according to the steel grade and product design. The exact parameters are determined by the alloy composition, section thickness, blade geometry, and required mechanical properties.
Multiple tempering cycles can help stabilize the structure and reduce internal stresses created during quenching. Stress relief is particularly important for pulverizer blades because even minor distortion can affect the grinding clearance. A blade that appears visually acceptable may still create uneven performance if its flatness or concentricity is not properly controlled.
After heat treatment, hardness should be checked at appropriate locations. The manufacturer may also inspect flatness, dimensional tolerances, edge condition, and surface quality. When necessary, metallographic analysis can be used to verify that the hardened structure is uniform and free from unacceptable defects.
Precision heat treatment delivers value in several ways. It improves wear resistance, helps maintain cutting performance under elevated temperatures, reduces the risk of deformation, and increases consistency between production batches. These benefits are particularly important for industrial users who operate pulverizers continuously or on multiple shifts.
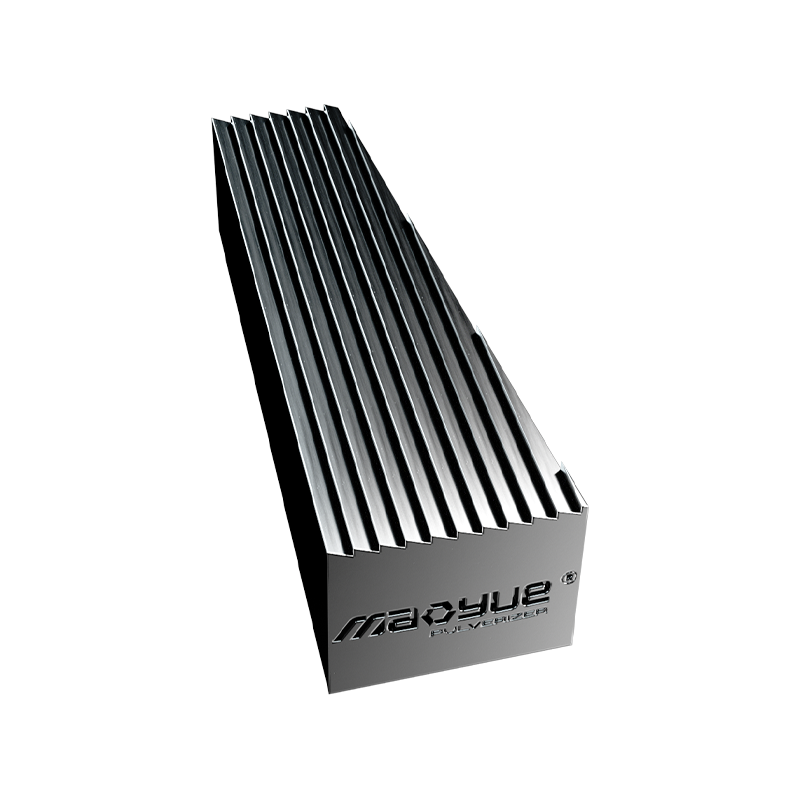
PE Pulverizer alloy steel blades
5. Manufacturing Process and Quality Control
The performance of a PE pulverizer blade is determined by every stage of production. Changzhou Mao Yue Intelligent Equipment Co., Ltd. manufactures plastic pulverizing components with an emphasis on precision processing and European-style quality requirements. Its production capability includes multiple processing workshops, specialized technical personnel, high-precision grinding equipment, dynamic balancing systems, and advanced welding facilities.
5.1 Material Preparation
The process begins with the selection and verification of alloy steel. Chemical composition must correspond to the required grade, and incoming material should be inspected for surface defects, dimensional consistency, and traceability. Proper material identification helps ensure that the heat-treatment recipe and machining allowance are suitable for the steel being used.
5.2 Forging and Forming
Forging can improve the density and directional structure of the steel. A properly forged blank has fewer internal discontinuities and a more favorable grain flow than a poorly prepared material. The forging process must be controlled to avoid overheating, underfilling, excessive oxidation, or residual stress.
After forging, the blank is prepared for machining. Excess material is removed while sufficient allowance is retained for heat-treatment distortion and final grinding. This stage requires careful planning because the final blade must meet both mechanical and geometric requirements.
5.3 Rough Machining
Rough machining establishes the basic dimensions of the blade, including its outer profile, mounting holes, tooth arrangement, and reference surfaces. The use of accurate fixtures helps maintain repeatability among blades in the same set.
Mounting accuracy is essential. If the holes or reference surfaces are misaligned, the blade may not sit correctly on the disc. This can cause vibration, uneven wear, excessive noise, and inconsistent grinding performance. For this reason, blade geometry must be considered together with the pulverizer disc and rotor assembly.
5.4 Heat Treatment and Stress Relief
After rough machining, the blade is subjected to the specified heat-treatment cycle. The process is monitored to achieve the target hardness while minimizing distortion. Stress relief and tempering help improve dimensional stability before final machining.
5.5 Precision Grinding
Precision grinding is used to achieve final thickness, flatness, tooth geometry, edge condition, and surface finish. High-precision grinding machines support tighter tolerances than basic machining methods. Changzhou Mao Yue Intelligent Equipment Co., Ltd. uses Taiwan-imported high-precision grinding equipment built to German standards for this type of processing.
Precision grinding is especially important for pulverizer blades because the working clearance may be adjusted to a very fine level. A small difference in blade thickness or flatness can influence the grinding gap and create uneven material flow. Accurate finishing improves the consistency of the blade set and helps the pulverizer maintain stable output.
5.6 Dynamic Balancing
High-speed rotating components must be balanced carefully. Uneven mass distribution can create vibration, increase bearing loads, accelerate wear, and reduce operating comfort. Dynamic balancing equipment is used to identify and correct imbalance in the rotating disc or related assembly.
German dynamic balancing equipment is used within the company’s manufacturing system to support stable component performance. Proper balancing is not only a machine safety issue; it also contributes to better powder quality because reduced vibration helps maintain a more consistent grinding gap.
5.7 Welding and Structural Fabrication
Where the pulverizer system includes welded structures, housings, supports, or cooling assemblies, welding quality also affects blade performance indirectly. A rigid and accurately fabricated machine frame helps maintain alignment between the rotating and stationary discs. Japanese welding systems are used in the company’s production capabilities to support reliable structural fabrication.
5.8 Final Inspection
Final inspection may include dimensional measurement, hardness testing, visual inspection, flatness verification, hole-position checking, surface-quality review, and balance-related checks. Product documentation can also include material information, inspection results, and identification details for future replacement orders.
This integrated manufacturing approach distinguishes a specialized pulverizer component supplier from a general cutting-tool producer. The blade is not treated as an isolated item. It is designed, machined, balanced, and tested as part of a complete pulverizing system.
6. Performance Advantages Compared with Ordinary Cutting Discs
Standard cutting discs may provide acceptable results for light-duty applications, but they can become inefficient when used in demanding PE pulverizing operations. The main difference is usually found in the material specification, heat treatment, precision, and suitability for continuous industrial use.
| Performance Factor | Ordinary Cutting Disc | PE Pulverizer Alloy Steel Blade | Operational Benefit |
|---|---|---|---|
| Typical hardness | Approximately HRC 45 | Approximately HRC 60–65 or higher | Improved wear resistance and edge retention |
| Material structure | General-purpose tool or cutting steel | High-density wear-resistant alloy steel | Better resistance to abrasive and impact loads |
| Heat treatment | Basic or less specialized treatment | Multiple precision heat treatments | Improved hardness, toughness, and stability |
| Service life | More frequent replacement | Up to approximately 800 hours under suitable conditions | Lower downtime and maintenance costs |
| Clearance control | Limited adjustment precision | Precision-adjustable clearance with fine tuning | More consistent powder fineness |
| Continuous operation | Greater risk of rapid dulling | Designed for long-duration industrial use | More stable production output |
| Customization | Often limited | Disc diameter, tooth profile, and material options can be customized | Better compatibility with different machines and materials |
The comparison should not be interpreted as a guarantee of identical results in every factory. Blade life depends on the entire application. A contaminated waste stream containing metal, stones, or other hard particles can reduce service life substantially. Incorrect clearance, inadequate cooling, excessive feed rate, or improper installation can also reduce performance. Even so, the alloy steel blade provides a significantly stronger technical foundation than a general-purpose disc.
7. Service Life and Maintenance Economics
A single-blade set can achieve approximately 800 hours of continuous service life under appropriate operating conditions. This figure represents a major advantage for production lines that operate continuously or process large volumes of material. Longer service life has value beyond the cost of the blade itself.
When blade replacement is required frequently, the user must account for machine shutdown, cooling time, disassembly, cleaning, inspection, installation, alignment, testing, and restart. Labor is consumed during every maintenance cycle, while production capacity is unavailable. If the machine is part of a larger recycling or compounding line, a pulverizer stoppage may also interrupt feeding, conveying, storage, extrusion, or packaging operations.
Longer-lasting blades can reduce:
1. Direct blade purchasing costs.
2. Labor costs associated with replacement.
3. Unplanned downtime.
4. Losses caused by unstable powder quality.
5. Emergency spare-parts requirements.
6. Production waste during machine restart and adjustment.
7. Maintenance-related safety exposure.
In addition, stable blade geometry helps the machine operate closer to its intended design point. A dull or uneven blade may require higher motor load to achieve the same output. It may also generate more heat and produce a broader particle-size distribution. By retaining its edge, the alloy steel blade supports more predictable energy use and output quality.
8. Precision Clearance and Powder Quality
The clearance between the rotating and stationary grinding components is a critical operating parameter. A larger clearance may reduce the risk of contact but can produce coarser material. A smaller clearance can improve fineness but may increase friction, heat generation, and the possibility of interference if the components are not accurately aligned.
PE pulverizer alloy steel blades support precision-adjustable clearance and micron-level fine tuning when used with a properly designed machine. Fine adjustment allows operators to match the grinding gap to the material type, feed rate, target fineness, and machine speed.
With suitable settings, PE powder can be controlled within approximately 20–80 mesh or finer. The precise result depends on the pulverizer model, screen or classification arrangement, feedstock properties, temperature control, and operating parameters. The objective is not simply to produce the smallest possible particle. The objective is to produce a stable and uniform particle distribution that meets downstream requirements.
Uniform powder offers several benefits. It can improve feeding stability, reduce agglomeration, support more consistent melting, and improve dispersion in compounding applications. In rotational molding, consistent particle size may help the material distribute more evenly across the mold surface. In powder coating, uniformity supports predictable fluidization and coating behavior. In extrusion and injection molding, consistent feed characteristics can improve process control.
9. Thermal Management During Grinding
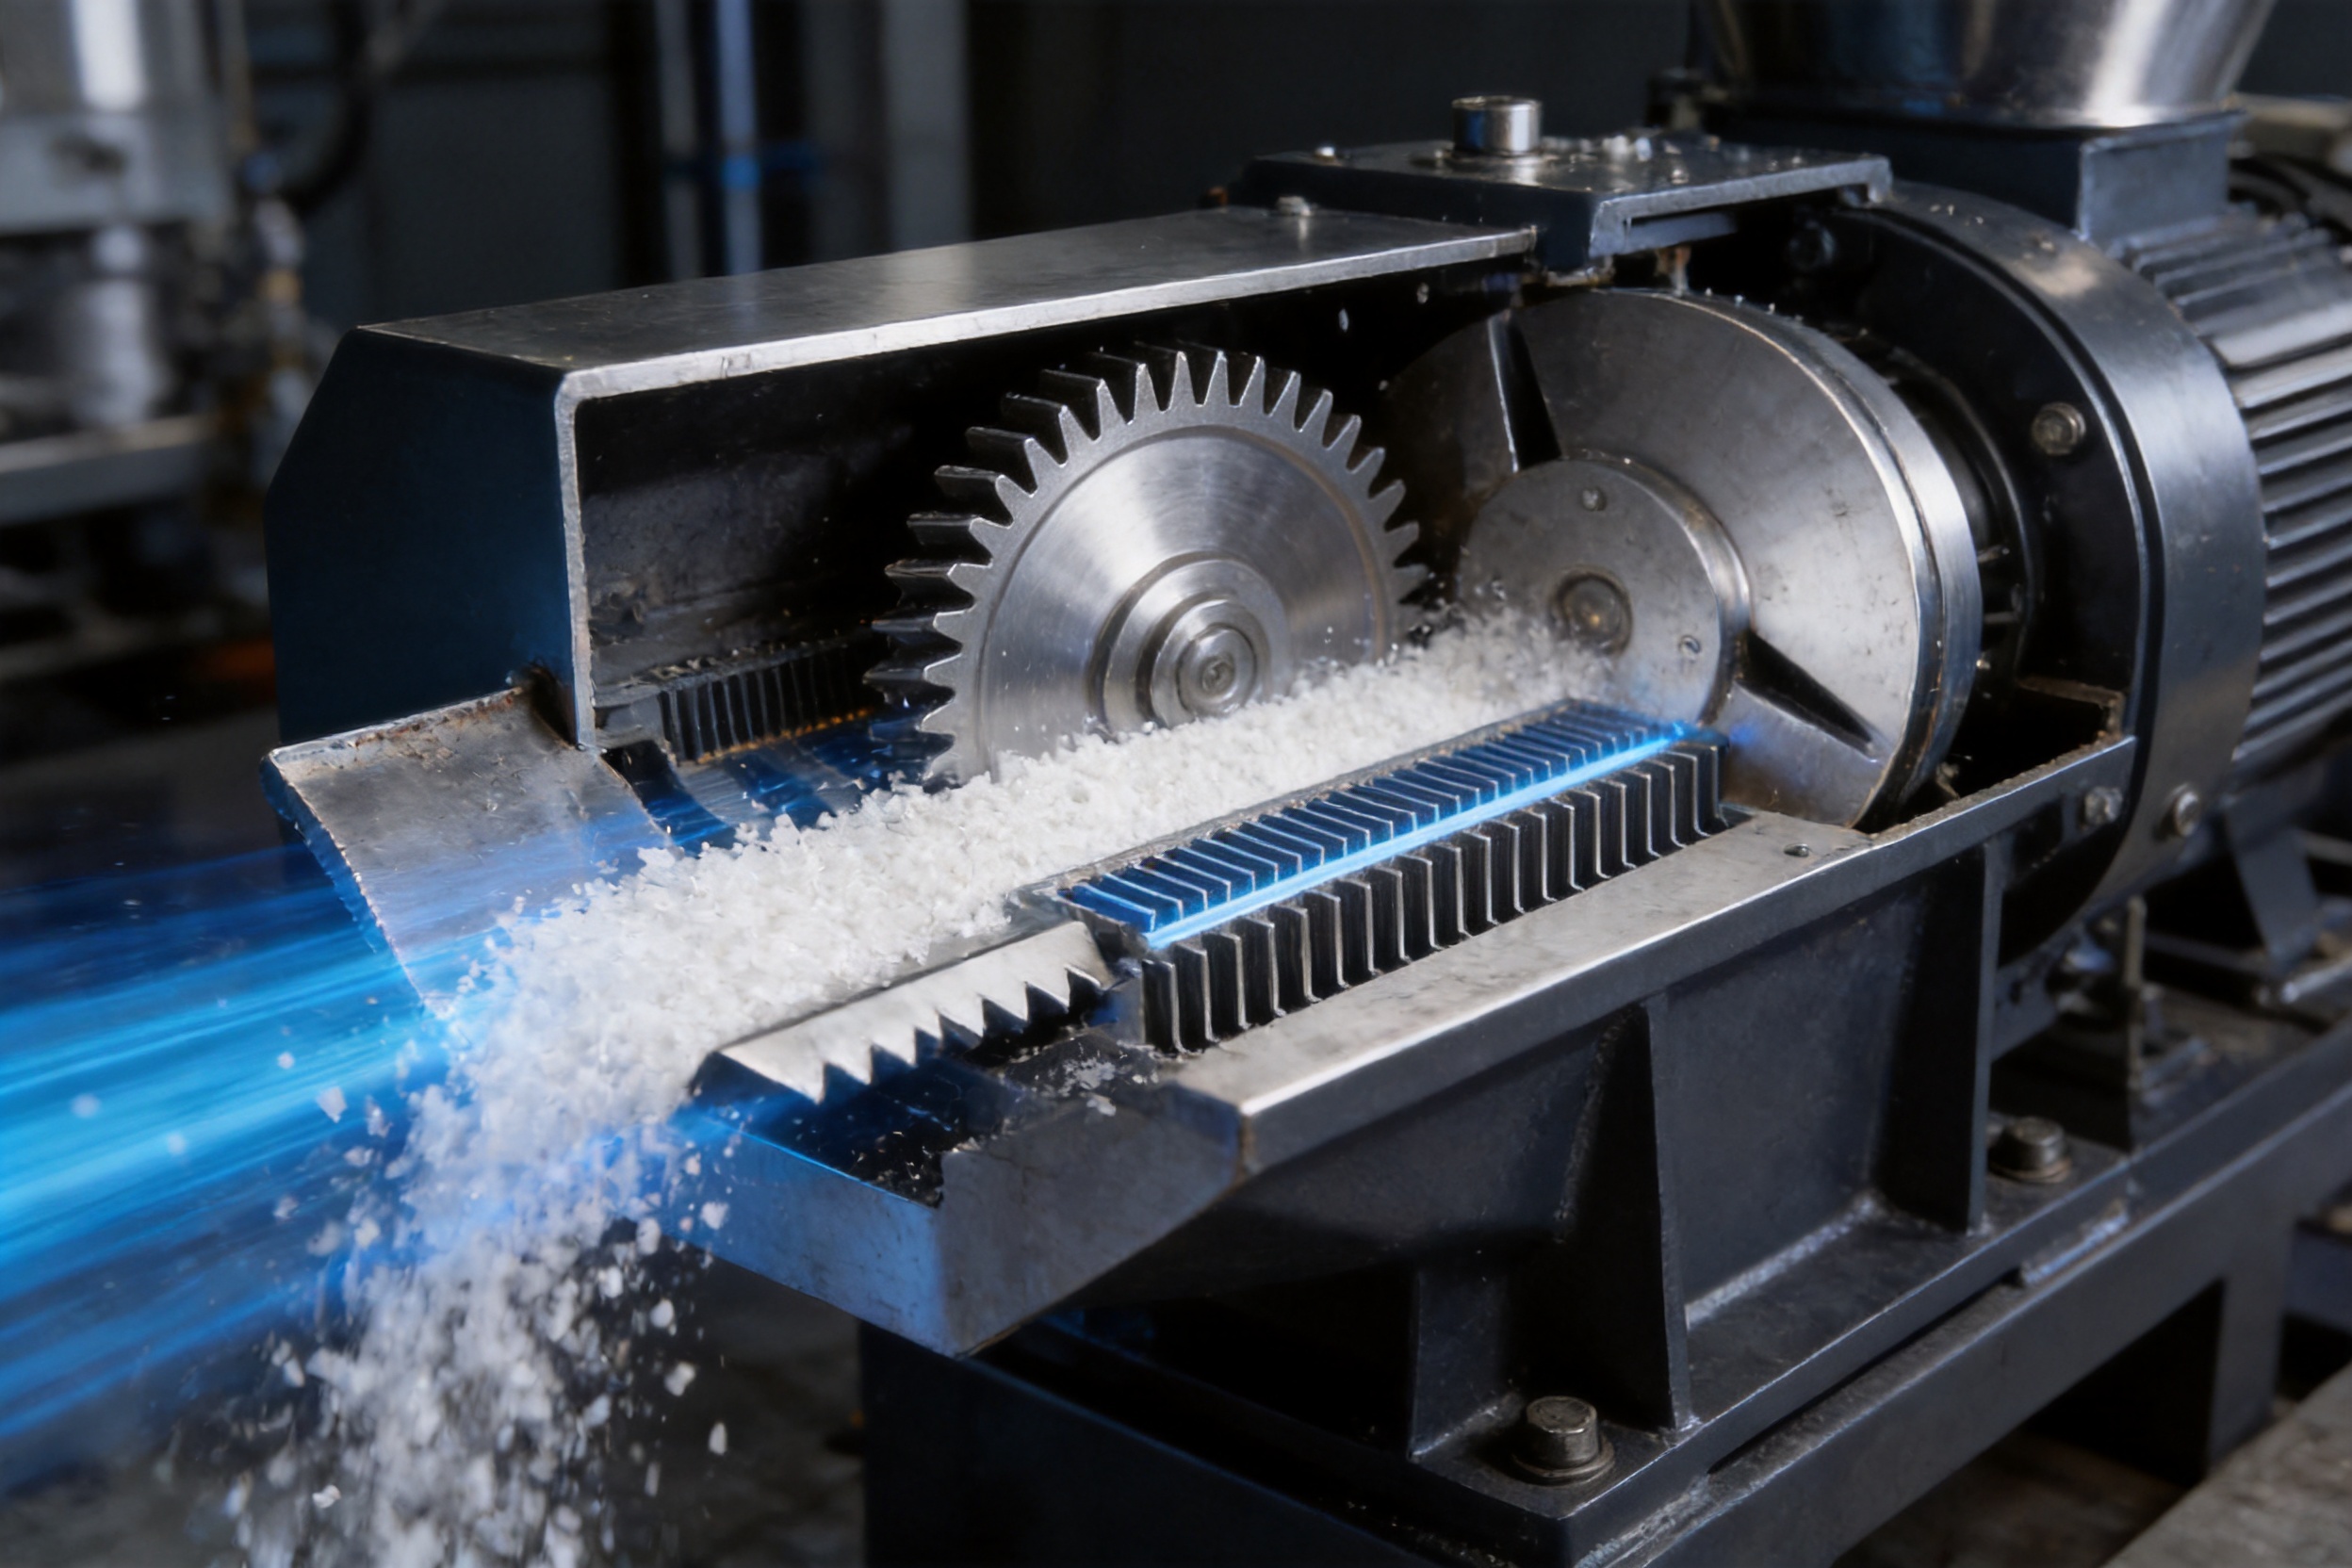
Polyethylene is sensitive to excessive frictional heat. As temperature increases, the material may soften, stick to the grinding surfaces, form agglomerates, or partially melt. These conditions can reduce throughput and interfere with the production of free-flowing powder. Heat can also affect the blade itself by accelerating softening, reducing edge stability, or causing dimensional changes.
The grinding disc and blade assembly can be designed with multi-tiered finned heat-dissipation structures and high-thermal-conductivity materials. These features increase the effective surface area available for heat transfer and help control disc temperature during operation.
Thermal control normally depends on several factors working together:
1. Blade geometry and cutting efficiency.
2. Disc design and heat-dissipation area.
3. Cooling-air or water-cooling arrangements, where applicable.
4. Feed rate and material temperature.
5. Rotor speed.
6. Grinding clearance.
7. Cleaning and airflow maintenance.
8. Correct selection of the blade and disc for the material.
A sharp, wear-resistant edge reduces the tendency of the machine to rub rather than cut. Efficient shearing can lower unnecessary friction and help the machine maintain a more manageable operating temperature. This is especially important during 24-hour industrial production, when even a small thermal imbalance can become a serious process problem over time.
Operators should still monitor temperature, motor current, vibration, powder appearance, and material flow. Blade design cannot compensate for blocked cooling passages, excessive feed rate, incorrect clearance, or contaminated feedstock.
10. Applications in Plastic Recycling
PE pulverizer alloy steel blades are suitable for a wide range of recycling and plastic processing applications. The most common feedstocks include polyethylene film, pipes, bottle caps, cable sheathing, strapping bands, molded components, and production scrap.
10.1 PE Film
Waste film can be difficult to process because it is flexible and may wrap around moving components. A properly configured pulverizer with sharp, wear-resistant blades can convert film into a more manageable powder or fine granulated material. Stable grinding helps prepare the material for regranulation, extrusion, or other recycling processes.
10.2 PE Pipes
Pipe scrap is generally thicker and more rigid than film. The blade system must tolerate greater impact when larger pieces enter the grinding chamber. High toughness, correct tooth geometry, and appropriate feed preparation are important for reliable processing.
10.3 Bottle Caps and Molded Parts
PE bottle caps and molded components may be relatively dense and can contain additives or colorants. Consistent grinding helps produce material suitable for reuse in compounding, pelletizing, injection molding, or other conversion processes.
10.4 Cable Sheathing and Strapping Bands
Cable sheathing and strapping bands often have high toughness and may resist ordinary cutting action. Alloy steel blades with strong edge retention can reduce the frequency of replacement during these demanding operations.
10.5 Recycling Line Integration
The pulverizer can be integrated with feeding, metal separation, conveying, storage, extrusion, and pelletizing equipment. Consistent powder quality supports more stable downstream processing and can help reduce the need for repeated screening or reprocessing.
11. Applications in Powder Coatings
PE powder is used in various coating applications where particle size, flowability, purity, and thermal behavior are important. Pulverizer blades must generate a fine and uniform powder while avoiding excessive heat that could cause scorching, sticking, or agglomeration.
For electrostatic spraying and fluidized-bed impregnation, powder consistency influences transport, fluidization, deposition, and coating thickness. Oversized particles may settle unevenly or fail to fluidize properly. Agglomerated particles can lead to inconsistent feeding and surface defects.
Alloy steel blades contribute to powder-coating production by maintaining a sharp edge and stable grinding performance over longer operating periods. When combined with accurate clearance adjustment and effective temperature control, the pulverizer can produce PE powder within the desired size range while reducing the risk of thermal damage.
12. Modified Plastics and Masterbatch Production
In modified plastics and filler masterbatch production, PE-based powder may be used as a carrier or as part of a compound formulation. Uniform particle size helps improve the distribution of additives, pigments, fillers, and functional materials during mixing and extrusion.
Uneven powder can produce inconsistent feed rates and poor dispersion. Fine particles may also behave differently from coarse particles during conveying and dosing. A stable powder structure allows compounders to establish more predictable process conditions and can contribute to better product consistency.
For color masterbatch production, uniformity is particularly important because uneven carrier particles may affect pigment distribution. For filler masterbatch, consistent particle size can support more controlled mixing and reduce variation between production batches. For functional masterbatch, the powder characteristics may influence the distribution of additives designed to improve electrical, optical, mechanical, or barrier properties.
13. Rotational Molding and Chemical Processing
Rotational molding requires powder that can flow and distribute across the internal surface of a heated mold. During heating and rotation, the powder gradually melts and forms a continuous wall. Powder with excessive agglomeration or inconsistent particle size may contribute to uneven wall thickness, surface defects, incomplete fusion, or trapped air.
Uniformly ground PE powder is suitable for the production of large hollow containers, storage tanks, industrial vessels, amusement equipment, and related products. The improved powder distribution can support smoother surfaces and more consistent wall formation.
In chemical processing, powder size and purity may affect reaction behavior, blending, feeding, or material handling. A pulverizer equipped with wear-resistant alloy steel blades can provide a reliable method for preparing PE-based materials where stable particle distribution is required.
14. Research, Development, and Small-Batch Processing
Laboratories and research departments often process small quantities of material, but their requirements for purity and repeatability can be more demanding than those of large production lines. A small variation in particle size may influence test results, formulation development, or process evaluation.
PE pulverizer alloy steel blades can be used in development work involving recycled materials, modified formulations, powder coatings, rotational molding compounds, and new additives. The ability to fine-tune clearance and maintain a clean, stable grinding environment helps researchers produce more representative samples.
When laboratory or pilot-scale equipment is used, operators should clean the grinding chamber carefully between materials. Cross-contamination can affect test results, especially when different colors, additives, or recycled feedstocks are evaluated.
15. Compatibility and Customization
As an original accessory for Mao Yue pulverizing equipment, these blades are designed to fit common disc diameters used in PE and PP pulverizers, including approximately 500 mm, 600 mm, and 800 mm configurations. They may also be adaptable to selected equipment from other manufacturers, subject to dimensional verification and engineering review.
Compatibility should never be determined by disc diameter alone. Before ordering replacement blades, users should confirm:
1. Outer diameter and inner diameter.
2. Mounting-hole quantity and position.
3. Blade thickness.
4. Tooth count and tooth profile.
5. Rotation direction.
6. Fixed-disc and rotating-disc arrangement.
7. Required grinding clearance.
8. Material type and expected contamination level.
9. Machine speed and motor power.
10. Cooling configuration.
Customized options may include disc diameter, tooth geometry, steel grade, hardness range, mounting pattern, and special processing requirements. Customization is useful when a customer processes an unusual PE formulation, requires a particular powder fineness, operates a modified machine, or needs a replacement part for an older pulverizer.
A qualified supplier should review drawings, photographs, sample components, or machine specifications before confirming compatibility. Correct fit is essential for safety, performance, and service life.
16. Installation and Commissioning Recommendations
Even a high-quality blade can perform poorly if installed incorrectly. Before installation, the machine should be isolated from all power sources and allowed to cool. The grinding chamber must be cleaned so that old plastic, dust, and foreign particles do not affect seating or clearance.
Mounting surfaces should be inspected for burrs, deformation, corrosion, or embedded material. Fasteners should be checked for correct grade and condition. Bolts must be tightened according to the equipment manufacturer’s recommended sequence and torque. Uneven tightening can distort the disc or create local stress in the blade.
After installation, the rotating assembly should be checked manually for free movement and possible interference. Where applicable, runout and balance should be verified. The machine should first be operated at no load or under a controlled low-load condition to confirm that there is no abnormal noise, vibration, or contact.
During initial production, operators should monitor motor current, vibration, temperature, powder fineness, and feed stability. If the material begins to soften or agglomerate, the operator should review the feed rate, cooling, clearance, and rotor speed. Continuing operation under abnormal conditions may damage both the blades and the pulverizer disc.
17. Maintenance and Inspection
Regular maintenance extends blade life and protects the complete pulverizer. Inspection intervals should be based on operating hours, material abrasiveness, production volume, and the level of contamination in the feedstock.
17.1 Routine Checks
Routine checks should include blade sharpness, visible chipping, edge rounding, surface cracks, mounting security, grinding clearance, vibration, temperature, and powder quality. Operators should record unusual changes rather than relying only on visual judgment.
17.2 Cleaning
Plastic residue should be removed from the grinding chamber and cooling passages. Accumulated material can interfere with airflow, increase friction, and create thermal problems. Cleaning also helps prevent cross-contamination when different materials are processed.
17.3 Clearance Adjustment
The grinding gap should be adjusted according to the material and required powder fineness. Excessively small clearance can increase heat and risk contact, while excessive clearance may reduce fineness and output quality. Adjustments should be made symmetrically and verified after the machine reaches its normal operating condition where applicable.
17.4 Blade Replacement
Blades should be replaced when wear reaches the manufacturer’s recommended limit, when the tooth profile is significantly altered, or when cracks and chips are detected. Mixing heavily worn blades with new blades may create uneven loading and inconsistent grinding. Whenever a blade set is replaced, the operator should inspect the disc, fasteners, bearings, seals, and balance condition.
18. Company Manufacturing Strengths
Changzhou Mao Yue Intelligent Equipment Co., Ltd. is a source manufacturer with approximately 30 years of experience in plastic crushing and pulverizing equipment. Its specialization covers disc pulverizers and related components for rotational molding, masterbatch, polymers, PVC, PE, recycling, and powder coating.
The company operates six processing workshops, with each workshop averaging approximately 1,400 square meters. This production structure supports the separation of different manufacturing activities and provides capacity for machining, fabrication, assembly, inspection, and customized orders.
A professional technical team regularly studies advanced equipment technologies from countries such as Germany. This technical focus is reflected in the company’s use of high-precision grinding equipment, dynamic balancing systems, and advanced welding technology. Such equipment is important because pulverizer performance depends on the relationship between blade geometry, disc balance, structural rigidity, and final assembly accuracy.
The company has developed long-term partnerships with more than 5,000 enterprises in domestic and international markets. This customer experience provides practical knowledge of different feedstocks, production environments, machine configurations, and replacement requirements.
Changzhou Mao Yue Intelligent Equipment Co., Ltd. has obtained CE mechanical certification and ISO 9001 quality management system certification. These certifications support its focus on product safety, manufacturing control, documentation, and continuous quality improvement.
Its manufacturing philosophy emphasizes quality, service, innovation, and customized solutions. For customers purchasing PE pulverizer alloy steel blades, this means technical support can extend beyond the individual replacement component. The supplier can evaluate machine compatibility, grinding requirements, disc configuration, material characteristics, and desired powder quality as part of a broader solution.
19. Sustainability and Total Operating Value
Longer blade life contributes to more sustainable plastic processing. When blades are replaced less frequently, fewer worn components need to be discarded and fewer resources are consumed in manufacturing replacement parts. Reduced downtime also helps improve the productivity of existing equipment, limiting the need for unnecessary machine expansion.
Uniform powder can improve material utilization in downstream operations. Better particle distribution may reduce rejects, reprocessing, and off-specification output. In recycling applications, this supports the conversion of waste PE into useful raw material for new products.
Energy performance also matters. A sharp blade can reduce the mechanical effort required to achieve a given powder size. Stable clearance and efficient heat management can help the motor and cooling system operate more effectively. The actual energy savings depend on the entire machine design and operating conditions, but blade performance is an important part of the overall equation.
These benefits align with the principles of resource efficiency, waste reduction, circular manufacturing, and responsible use of industrial equipment. For plastic processors, sustainability is not separate from cost control. Longer service life, fewer stoppages, and improved powder quality can support both environmental and commercial objectives.
20. How to Select the Correct Blade
Before purchasing PE pulverizer alloy steel blades, users should collect detailed information about the machine and application. The following questions help ensure a correct selection:
1. What is the pulverizer model and disc diameter?
2. Is the blade installed on the rotating disc, fixed disc, or both?
3. What are the outer diameter, inner diameter, thickness, hole pattern, and tooth count?
4. What type of polyethylene is being processed?
5. Does the material contain glass fiber, mineral filler, pigments, metal, sand, or other contaminants?
6. What powder fineness and particle-size distribution are required?
7. What are the normal rotor speed, feed rate, and production hours?
8. Is the machine air-cooled, water-cooled, or equipped with another thermal-management system?
9. What problems occurred with the previous blades?
10. Is a customized tooth profile or steel specification required?
Providing drawings, photographs, sample blades, and operating data allows the manufacturer to make a more accurate recommendation. This reduces the risk of ordering a dimensionally compatible part that is not suitable for the actual material or production conditions.
21. Frequently Asked Questions
Q1: What makes alloy steel blades different from ordinary pulverizer blades?
Alloy steel blades are produced from higher-performance wear-resistant materials and receive specialized heat treatment. They typically achieve higher hardness, stronger edge retention, improved impact resistance, and longer service life than ordinary cutting discs. Their geometry and precision finishing are also optimized for pulverizer operation.
Q2: What hardness can these PE pulverizer blades achieve?
The typical hardness is HRC 60–65 or higher, depending on the selected steel grade and heat-treatment specification. The final hardness should be balanced with toughness and dimensional stability for the intended application.
Q3: Can the blades process glass-fiber-reinforced plastic?
They can be used for demanding materials, including certain reinforced or high-toughness plastics. However, glass fiber and mineral fillers are abrasive, so service life depends on concentration, feedstock cleanliness, feed rate, and machine settings. Application evaluation is recommended before selecting the final specification.
Q4: How long can one blade set operate?
Under suitable operating conditions, a single-blade set can achieve approximately 800 hours of continuous service life. Actual service life varies according to material, contamination, speed, cooling, clearance, and maintenance.
Q5: What powder fineness can be achieved?
The pulverizer can produce PE powder in the approximate range of 20–80 mesh or finer when the machine, blade profile, clearance, cooling, and operating conditions are correctly matched. The final result should be confirmed through testing because different PE grades behave differently during grinding.
Q6: Are the blades compatible with other brands of pulverizers?
Some blades may be adaptable to other brands, but compatibility must be confirmed by comparing disc diameter, thickness, hole pattern, tooth profile, rotation direction, and clearance requirements. The manufacturer should review technical data before an order is finalized.
Q7: Can the blade dimensions and tooth profile be customized?
Yes. Customization may include disc diameter, mounting arrangement, tooth profile, steel grade, hardness, and other dimensional specifications. Drawings or sample components are normally required for accurate engineering.
Q8: Why is thermal control important when grinding PE?
Excessive heat can soften polyethylene, cause sticking and agglomeration, reduce powder quality, and accelerate blade wear. Efficient blade geometry, proper clearance, cooling structures, and controlled operating conditions help maintain stable temperatures.
Q9: What should be checked before installing replacement blades?
The operator should inspect the disc, mounting surfaces, fasteners, bearings, seals, balance condition, and cooling passages. The new blades should be installed with correct alignment and tightening procedures, followed by a controlled no-load or low-load test.
Q10: What certifications does the manufacturer hold?
Changzhou Mao Yue Intelligent Equipment Co., Ltd. has obtained CE mechanical certification and ISO 9001 quality management system certification. These certifications support its manufacturing quality, product safety, and process-control practices.
Q11: Can these blades be used in recycling and powder-coating lines?
Yes. They are designed for PE and related plastic pulverizing applications, including recycling, regranulation preparation, powder coatings, masterbatch, rotational molding, chemical processing, and research or pilot-scale work.
Q12: How can blade life be maximized?
Blade life can be improved by removing metal and mineral contaminants, maintaining correct clearance, avoiding excessive feed rates, monitoring temperature and vibration, cleaning cooling passages, balancing the rotating assembly, and replacing blades before severe damage occurs.
Conclusion
PE pulverizer alloy steel blades are high-value components for plastic processors that require long service life, stable powder quality, and reliable continuous operation. Their main advantages come from the combination of wear-resistant alloy steel, high hardness, controlled toughness, multiple precision heat treatments, accurate machining, precision-adjustable clearance, and effective thermal management.
Compared with ordinary cutting discs, these blades can provide stronger resistance to abrasion and impact, lower wear rates, more consistent powder output, and significantly reduced replacement frequency. Under appropriate conditions, a service life of approximately 800 continuous operating hours can help reduce downtime, maintenance labor, and total operating costs.
The value of the blade is further increased when it is manufactured as part of a complete pulverizer engineering system. Changzhou Mao Yue Intelligent Equipment Co., Ltd. combines decades of industry experience with multiple processing workshops, high-precision grinding equipment, dynamic balancing technology, advanced welding systems, technical expertise, CE certification, and ISO 9001 quality management. These strengths support reliable production of standard and customized pulverizer components.
For recycling, powder coating, masterbatch, rotational molding, chemical processing, and research applications, correct blade selection is essential. Users should evaluate machine dimensions, material characteristics, contamination, required fineness, cooling conditions, and operating hours before purchasing. When the blade specification is properly matched with the pulverizer and maintained correctly, it can improve grinding efficiency, product consistency, equipment reliability, and the sustainability of PE processing operations.
References
1. General principles of alloy steel selection for wear-resistant industrial cutting components.
2. Industrial guidance on heat treatment, tempering, hardness control, and dimensional stability of tool steels.
3. Technical literature on plastic pulverizing, particle-size reduction, and high-speed disc grinding.
4. Processing references for polyethylene recycling, regranulation, powder coating, and rotational molding.
5. Industrial practices for dynamic balancing of high-speed rotating equipment.
6. Quality management principles associated with ISO 9001 manufacturing systems.
7. Machinery safety and conformity principles associated with CE mechanical certification.
8. Manufacturer-provided technical information for PE pulverizer alloy steel blades and plastic pulverizing equipment.